Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
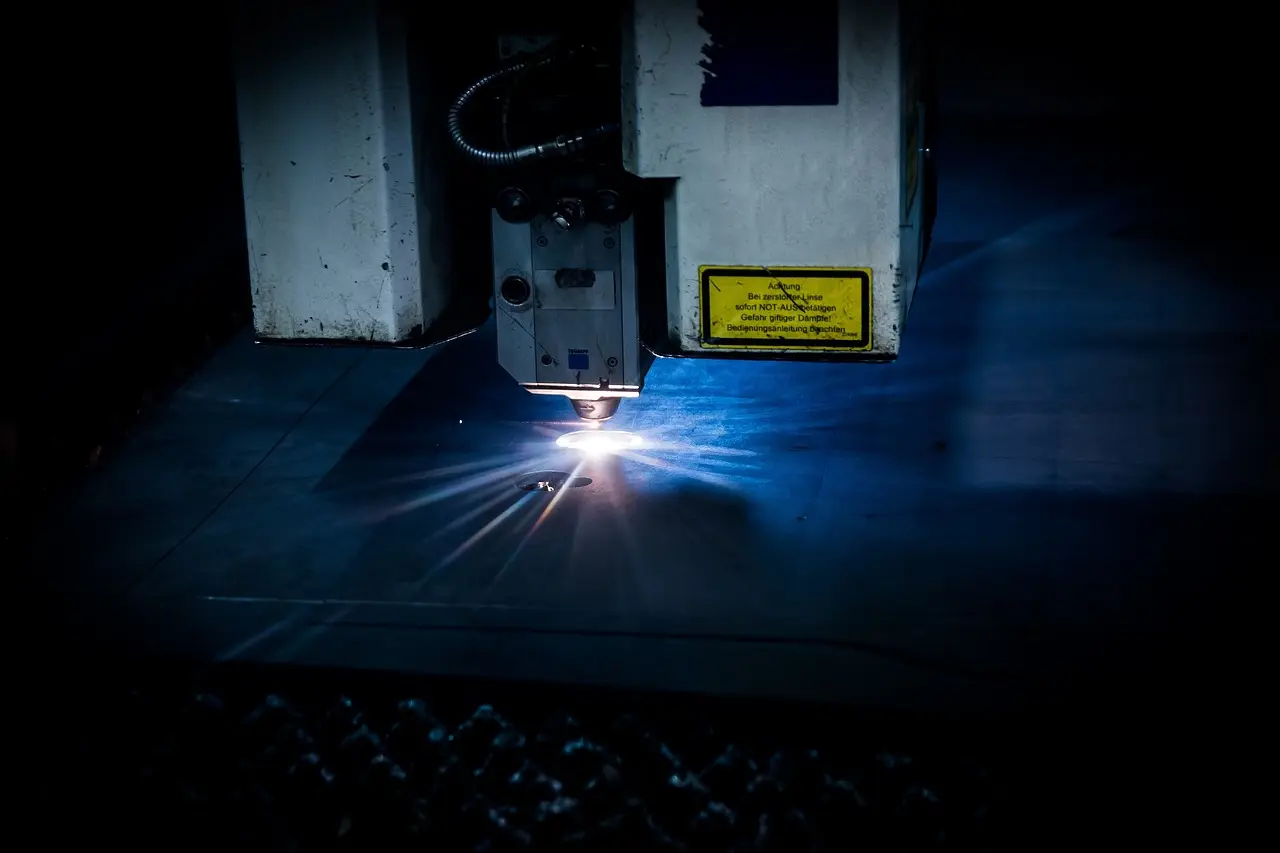
When production managers compare new versus used laser cutters, the invoice price is the weakest metric to anchor the decision. The real ROI calculation lives in throughput, uptime predictability, output consistency, and labor efficiency across the machine’s operating life. A used unit that cuts acceptable samples during a demo can still hide deferred maintenance, aging controllers, or degraded cooling loops that surface weeks later as scrap, missed shipments, and absorbed engineering time. Before committing capital, buyers must weigh commissioning risk, parts access, and workflow compatibility against the lower entry costâbecause the machine that disrupts scheduling discipline quietly erases its price advantage.
Why the Invoice Price Is the Wrong Place to Start the ROI Calculation
Every new-versus-used laser cutter discussion seems to begin with the purchase price. That is understandable, but it is not where the real financial decision lives. In a production environment, a laser cutter earns its keep through throughput, usable output, labor efficiency, repeatability, and delivery reliability. A machine that costs less upfront but interrupts the workflow, produces inconsistent edge quality, or consumes engineering time for troubleshooting will quietly erase its price advantage within the first year of operation.
The ROI calculation that matters on the shop floor includes far more than the capital expense. It includes installation and commissioning effort, downtime risk and recovery time, scrap and rework from unstable output, operator setup time between jobs, parts and service availability, and residual value at the point of replacement. A used machine can improve ROI if it lowers capital pressure without damaging those operating factors. A new machine usually improves ROI when the plant cannot afford instability, missed shipments, or quality drift.
Consider a typical scenario. A cabinet shop buys a used laser cutter for 40 percent less than the new equivalent. The machine cuts acceptable sample parts during the demonstration. Three weeks into production, the operator notices that edge quality drifts after two hours of continuous running. The cause turns out to be a degraded cooling loop that was not obvious during the short demo. The shop loses half a shift while a technician diagnoses the issue, then waits three days for a replacement pump. That single event consumes more value than the initial purchase savings in labor, missed delivery penalties, and rescheduling costs. This is not an unusual story. It is the standard failure mode of price-led buying.
Where the Economics Actually Change Between New and Used
The strongest way to compare the two options is to separate visible savings from hidden operating consequences. The table below lays out the decision areas that matter most in a production setting.
| Decision Area | New Laser Cutter | Used Laser Cutter | ROI Impact |
|---|---|---|---|
| Upfront Cash Requirement | Higher initial spend | Lower entry cost | Used equipment can shorten payback only if operating risk stays controlled |
| Commissioning and Ramp-Up | More predictable startup condition | Condition varies by prior use and maintenance history | Uncertain ramp-up delays revenue and consumes engineering time |
| Uptime Predictability | Usually easier to standardize early | Often depends on wear level and inspection quality | More downtime raises cost per good part |
| Service and Spare Parts | Usually clearer support path | May depend on controller age, local parts access, and third-party service | Slow repairs can erase initial savings quickly |
| Software and Controls | More likely to fit current workflow expectations | Compatibility can be limited or outdated | Older controls can slow setup, repeat jobs, and training |
| Output Consistency | Easier to stabilize across operators | Can vary if motion, optics, cooling, or alignment are not in good condition | Variation increases scrap and rework |
| Financing and Warranty Position | Commonly easier to structure | Often more limited or more conditional | Financing flexibility can matter as much as nominal purchase price |
| Depreciation Exposure | Higher initial value drop | Lower depreciation risk if bought carefully | Used machines can win when resale discipline matters |
This is why used equipment is not automatically the budget winner and new equipment is not automatically the ROI winner. The answer changes with workload, maintenance capability, and tolerance for interruption.
When a New Laser Cutter Usually Delivers Better Long-Term ROI
New equipment usually becomes the stronger ROI decision when the laser is expected to function as a reliable production asset rather than a low-cost capacity add-on. That is especially true when the business depends on daily output, customer-visible finish quality, or repeated job consistency. In those conditions, the value of a new machine comes less from the word new and more from the lower uncertainty around startup condition, support, and process stability.
New machines often produce stronger long-term ROI in situations such as:
- The laser will run regularly rather than occasionally
- The plant has low tolerance for missed delivery dates
- Multiple operators or shifts will share the machine
- Output consistency matters more than absolute lowest capex
- Engineering time is too valuable to spend on troubleshooting inherited problems
In practical terms, a new laser cutter often protects ROI through smoother commissioning, easier standardization, cleaner documentation, and lower exposure to deferred maintenance. That does not eliminate downtime or operating cost, but it usually reduces the number of unknowns during the first years of ownership.
For growing shops, that predictability can matter more than the purchase gap itself. A cheaper machine that disrupts quoting accuracy, job scheduling, or rework rates can quietly become the more expensive option.
Think about a shop that runs two shifts and quotes jobs based on a standard cutting time per sheet. If the used machine runs 15 percent slower because of worn motion components or an older controller that processes files less efficiently, every quote becomes slightly wrong. The shop either eats the difference or re-quotes and loses work. Over a year, that 15 percent penalty on a machine running 4,000 hours is the equivalent of losing 600 hours of productive capacity. That is not a rounding error. That is a full-time operator position worth of output.
New equipment also tends to come with current software that matches the file formats and nesting routines the shop already uses. This matters more than many buyers expect. Older controllers may require file conversion steps, limit the size of the job file, or lack the parameter memory that lets operators recall proven settings for a specific material and thickness. Every extra step in the setup routine is labor that does not add value to the part.
When a Used Laser Cutter Can Still Be the Smarter Investment
Used equipment can deliver excellent ROI when the buyer is disciplined and the production environment can tolerate more uncertainty. A used laser cutter is often worth serious consideration when:
- Machine utilization will be moderate rather than constant
- The workflow is stable and technically familiar
- The shop has maintenance capability in-house or trusted local support
- The machine can be inspected under power before purchase
- Critical wear, alignment, and cooling condition can be verified
- The business values lower depreciation risk and faster capital recovery
In those situations, a used machine can lower the breakeven point without putting the plant in a fragile operating position. That is particularly true for buyers who understand the process well enough to identify whether the machine’s condition matches the intended workload.
Consider a small sign shop that runs a laser for perhaps 15 hours per week. The jobs are varied, the tolerances are moderate, and the owner personally handles maintenance. A used machine with a known service history can be an excellent fit. The lower entry cost means the machine pays for itself after fewer billable hours. The owner can inspect the optics, check the alignment, and verify the cooling system before committing. If a component fails, the owner can repair it directly or call a local technician who knows the platform. In this context, the used machine is not a gamble. It is a calculated purchase backed by the buyer’s own competence.
The mistake is not buying used. The mistake is buying used as if lower price alone guarantees stronger ROI.
The Hidden Costs That Most Often Destroy Used-Equipment Savings
Most disappointing used-machine purchases fail for the same reason: the buyer compared price tags, not operating conditions. The biggest hidden costs usually come from five areas.
Deferred maintenance. A machine may cut sample parts well enough during a brief demonstration and still carry unresolved wear in motion components, optics, cooling systems, extraction support, or electrical stability. Those problems do not always appear immediately, but they tend to appear at the worst time: once the machine enters the schedule. A laser tube that has been running at reduced power for months may still produce acceptable cuts on thin material. The same tube will struggle on thicker stock, producing charred edges and requiring multiple passes. The seller may not even be aware of the degradation because they stopped pushing the machine to its limits.
Controller and software age. Older control platforms can limit file handling, slow job setup, complicate recipe consistency, or make operator training harder than expected. Even when the machine still cuts, the workflow friction can be significant. A controller that cannot store material profiles forces the operator to re-enter power, speed, and frequency settings for every job. That is not a one-time cost. It is a recurring tax on every setup for the life of the machine. If the shop runs 20 jobs per week, and each setup takes an extra ten minutes because of manual parameter entry, that is more than 170 hours of lost labor per year.
Parts access. A used machine with uncertain spare-parts availability can turn a minor fault into a long outage. That single factor can outweigh a large portion of the initial purchase savings. A focus lens or a cooling pump may be a relatively inexpensive component, but if the supplier no longer stocks it and the only source is a salvage operation with a two-week lead time, the machine sits idle. Every day of idle time on a machine that was supposed to generate revenue is a direct hit to the ROI calculation.
Installation and retrofit cost. Used equipment sometimes needs more than transport and power connection. Buyers may face additional spending on ventilation, cooling, electrical adjustment, guarding, fixture updates, or software workarounds before the machine performs reliably. A machine from a facility with three-phase power may need a phase converter in a shop that only has single-phase service. An older machine may lack the safety guarding required by the buyer’s insurance policy. These costs are rarely included in the advertised price, and they can add up to a significant portion of the difference between new and used.
Unstable quality. If a used machine introduces more burn marks, inconsistent edge quality, registration drift, or repeat-job variation, the true cost shows up as extra labor and lost usable output rather than as a clean line item on the invoice. A machine that requires the operator to babysit every cut, adjusting power settings mid-job to compensate for drift, is not saving labor. It is consuming it. The operator who should be preparing the next job is instead standing at the laser, watching for quality problems.
What Buyers Should Check Before Calling a Used Machine a Bargain
If long-term ROI is the goal, a used machine should be evaluated with the same discipline used for any production bottleneck asset. Buyers should verify:
- Actual production history rather than only age
- Current operating condition under real cutting or engraving load
- Service records and replacement history where available
- Availability of spare parts, consumables, and technical support
- Controller version and practical workflow compatibility
- Cooling, extraction, and alignment condition
- Reason for sale and whether the machine was replaced for capacity or for reliability problems
Just as important, the buyer should match inspection depth to business risk. If the laser is expected to handle customer-facing work on a daily schedule, the cost of a poor inspection is much higher than the cost of a more thorough pre-purchase evaluation.
Ask the seller for a production log if one exists. Request the maintenance records. Find out when the laser tube was last replaced and what the estimated remaining life is. A laser tube is a consumable with a finite lifespan, and replacing it can cost a significant portion of the machine’s purchase price. If the tube is near the end of its life, the effective cost of the used machine is the purchase price plus the tube replacement cost. That changes the comparison.
Also ask about the extraction system. Laser cutting produces smoke and particulate that must be removed from the cutting area. An undersized or poorly maintained extraction system can cause inconsistent cuts, dirty optics, and a hazardous work environment. If the used machine requires extraction upgrades, that cost belongs in the ROI calculation.
Run a test with the actual materials the shop will process. Do not accept a demonstration on thin acrylic if the shop plans to cut 18mm plywood. The machine may perform well on one material and poorly on another. The test should include the thickest material, the most detailed geometry, and the longest continuous run the shop expects to produce. That is the only way to see how the machine behaves under realistic load.
A Simple Decision Framework for Long-Term ROI
The choice becomes clearer when buyers connect machine type to operating context. The table below summarizes the situations that tend to favor each option.
| Your Situation | New Usually Makes More Sense | Used Can Make Sense |
|---|---|---|
| High schedule pressure | Yes | Only if condition and support are unusually clear |
| One machine must carry core production | Yes | Only with strong maintenance confidence |
| Low to moderate utilization | Not always | Often |
| In-house maintenance capability is limited | Yes | Rarely |
| In-house maintenance capability is strong | Sometimes | Often |
| Output quality is customer-visible and repeat-critical | Yes | Only after rigorous validation |
| Budget pressure is high but downtime is tolerable | Sometimes | Often |
| Depreciation control matters more than perfect predictability | Sometimes | Often |
This is the practical point many buyers miss: ROI is not only about how quickly the machine pays for itself. It is also about how much operational instability the plant must absorb before it does.
How to Calculate the Real Cost Per Good Part
One of the most useful exercises for any buyer is to calculate the cost per good part for both options. This moves the discussion away from the purchase price and toward the metric that actually drives profitability.
Start with the total cost of ownership over a five-year horizon. For a new machine, this includes the purchase price, installation, training, routine maintenance, consumables, and expected downtime. For a used machine, include the purchase price, any retrofit or repair work identified during inspection, the expected remaining life of the laser tube and other wear components, and a contingency for unexpected failures. Be honest about the contingency. A used machine with unknown service history deserves a larger contingency than one with complete records.
Then estimate the number of good parts the machine will produce per year. This is not the theoretical maximum throughput. It is the realistic output after accounting for setup time, material handling, quality checks, and downtime. A new machine might produce 95 percent of its theoretical capacity in the first year. A used machine with some wear might produce 80 percent. That difference compounds over five years.
Divide the total cost by the total good parts. The result is the cost per good part. In many cases, the used machine looks attractive on paper until this calculation is done. A 30 percent purchase price savings can disappear entirely when the used machine produces 15 percent fewer parts per year and requires 20 percent more maintenance labor.
This calculation also helps buyers identify the breakeven point. If the used machine costs $20,000 less than the new equivalent, and the shop produces 2,000 parts per year, the used machine saves $10 per part in capital cost. But if the used machine produces 5 percent more scrap, and each scrapped part costs $15 in material and labor, the scrap penalty is $1,500 per year. Over five years, that is $7,500. The used machine still wins, but the margin is thinner than the price difference suggested.
If the used machine also requires an extra 30 minutes of setup per job, and the shop runs 200 jobs per year, that is 100 hours of labor. At $50 per hour fully loaded, that is $5,000 per year. Over five years, that is $25,000. Now the used machine is more expensive than the new one, despite the lower purchase price.
This is why the purchase price is the wrong starting point. The cost per good part is the metric that reflects reality.
The Best Choice Depends on Whether You Are Buying Capacity or Certainty
New equipment usually buys certainty. Used equipment usually buys capacity at a lower entry cost.
If the plant needs a dependable laser process that supports scheduling discipline, repeatable quality, and easier operator management, new equipment often produces the better long-term return despite the higher initial price. If the plant needs incremental capacity, understands the technology, and can manage maintenance and validation risk internally, a used laser cutter can produce very attractive ROI. But that result comes from careful screening, not from price alone.
The decision also depends on where the shop is in its growth cycle. A startup with limited capital and a founder who understands laser technology may be better served by a used machine that frees up cash for other investments. An established shop with customer commitments and a reputation for on-time delivery may find that the cost of uncertainty is higher than the savings from buying used.
There is also a middle path worth considering. Some buyers purchase a used machine as a secondary unit, keeping the primary production on a newer machine. This spreads the risk. If the used machine fails, the shop can shift work to the primary unit while the repair is made. This arrangement can work well for shops that have grown to the point where a second machine is justified but the budget does not support two new units.
For shops evaluating laser cutters and engravers for wood, acrylic, and similar non-metal materials, the same logic applies. The question is not which option is cheaper. The question is which option will produce acceptable parts, on schedule, with the least avoidable friction over the life of the investment. That is the version of ROI that matters in production.
Before making the final decision, write down the shop’s specific requirements: expected weekly hours, material types and thicknesses, quality standards, operator skill level, maintenance capability, and tolerance for downtime. Then evaluate each option against those requirements. A machine that meets the requirements at a lower cost is the better investment. A machine that fails the requirements at any price is not an investment at all. It is a liability.
The buyers who get this decision right are the ones who treat the laser cutter as a production tool with a specific job to do, not as a bargain to be captured. They know the machine’s role in the workflow, they understand the cost of failure, and they choose accordingly. That discipline is what separates a good ROI from a costly mistake.