Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
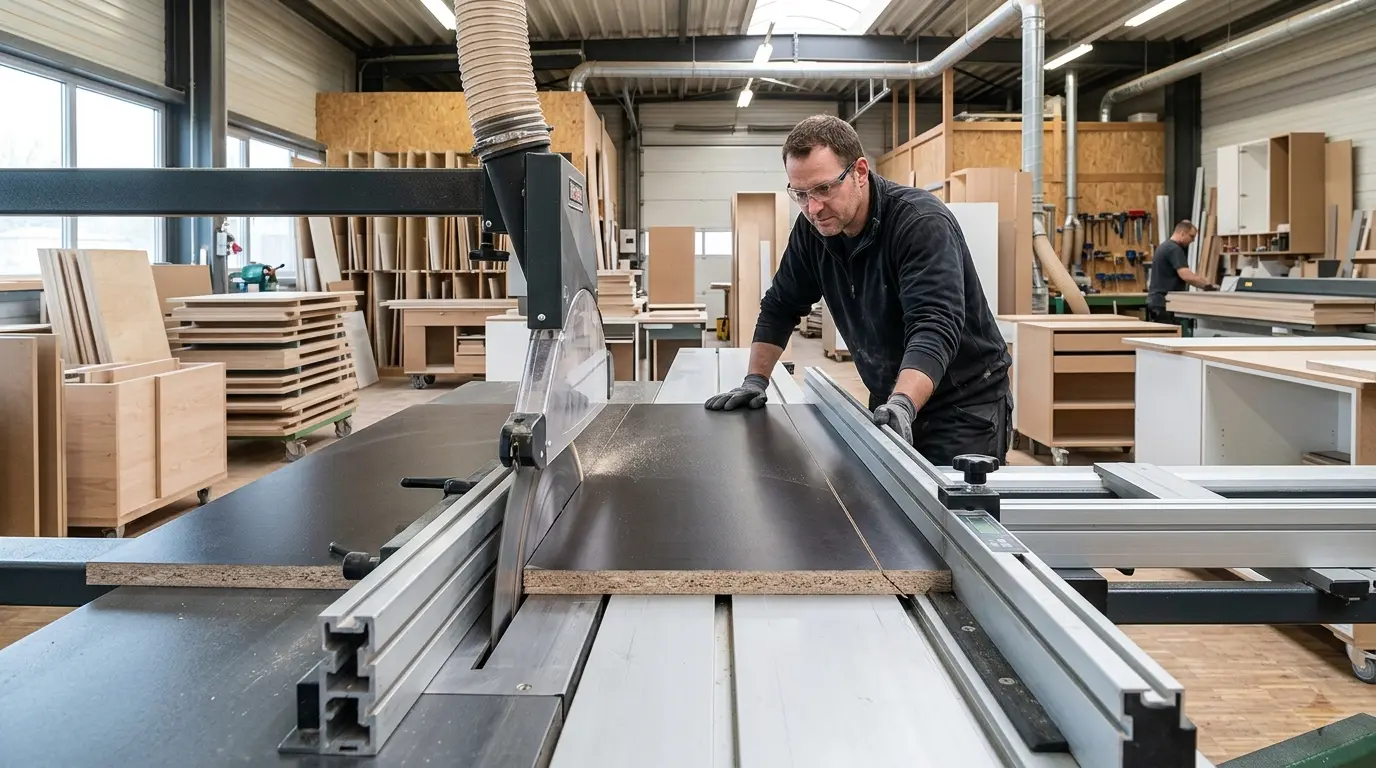
Cabinet shops often buy panel saws by comparing spec sheets, yet the real failure point is upstream: the daily part mix, downstream tolerance chain, and material flow decide whether the machine pays back. This article walks through the production logic that should precede any purchase—how rectangular part repetition, half-millimeter drift into edgebanding and drilling, sheet handling weight, and batch discipline determine true throughput. For factory managers and procurement teams, the decision hinges on workflow fit, not headline speed, and the evaluation framework here forces that comparison before capital is committed.
Start With the Part Mix, Not the Machine Specs
The decision to buy a panel saw should begin with a clear look at what actually comes off your cutting table every day. If your cabinet production is built around repeated rectangular parts—carcass sides, tops, bottoms, shelves, and partitions cut from melamine-faced board, MDF, plywood, or particleboard—a dedicated panel saw can turn the front end of your line into a stable, predictable operation.
If, however, your work is heavily custom, shape-driven, or changes constantly from job to job, the value equation shifts. In that environment, flexibility matters more than pure sizing efficiency. Buyers often make their first mistake here: comparing saws before confirming what percentage of daily output is genuinely repetitive cabinet work. That number should drive the conversation, not the brochure.
Walk through a typical week and tally the cut list. Count how many parts are rectangles with square edges versus parts that require shaped profiles, angled cuts, or non-standard dimensions. In most cabinet shops, the rectangular share lands somewhere between 70 and 90 percent of total parts. That range tells you whether a panel saw will be running constantly or sitting idle while you handle the odd-shaped work on another machine. A shop at 70 percent repetition still benefits from a panel saw, but it needs a secondary cutting solution for the remainder. A shop at 90 percent repetition can justify a more capable saw with automated features because the machine will earn its keep every shift.
The mistake we see most often is a buyer who starts with a budget and a brand preference, then tries to make the production case fit the machine. Reverse that order. Define the part mix first, then the required tolerances, then the throughput, and only then look at machines. The spec sheet will make more sense when you already know what you need it to do.
Cutting Accuracy Is a Downstream Decision
In cabinet manufacturing, a cut is not an isolated event. It is the first step in a chain that includes edgebanding, drilling, hardware fitting, and final assembly. A part that leaves the saw with slight size variation does not stay at the saw. It carries into the edgebander, where inconsistent panel width creates poor adhesive contact or visible glue lines. It carries into the drilling machine, where hole positions shift relative to the panel edge. It carries into assembly, where operators compensate by forcing parts together or shimming gaps.
That is why the most important performance measure is not cycle time in isolation. It is whether the saw sends parts forward with the consistency needed for:
- Cleaner edge finishing with fewer rejects
- Predictable hole positioning and hardware fit
- Less manual measuring and checking before the next operation
- Fewer re-cuts and mismatched cabinet components
- Smoother assembly without operator compensation
A slightly slower saw that holds tolerance across a full shift is worth more than a faster machine that drifts or requires constant adjustment. When buyers focus only on headline speed, they miss the bigger production issue: a controlled front end reduces interruptions everywhere downstream.
Consider what happens when a panel saw produces parts that vary by half a millimeter across a batch. The edgebander applies a 1mm PVC edge. On a part that measures 600.5mm instead of 600mm, the edgebander still applies the strip, but the adhesive bond at the leading and trailing corners becomes inconsistent. The part then moves to the drilling machine, where the CNC program assumes a 600mm width. Hole positions shift by that same half millimeter. At assembly, the cabinet back panel no longer aligns perfectly with the side panels. The installer on site has to adjust hinges or trim filler strips. That half millimeter at the saw has now cost you labor in three downstream operations and potentially a field callback.
The tolerance story is not just about the saw’s rated accuracy. It is about how that accuracy holds when the blade dulls, when the operator is on hour seven of a shift, and when the material batch changes from one supplier to another. A machine with a rigid frame, a stable scoring blade, and a reliable fence system will hold tolerance longer than a lighter machine that flexes under load. Ask the manufacturer what their accuracy claim is based on—a single test cut or a full production run. Then ask for references from shops running similar material and part mixes.
Material Handling Often Decides Real Productivity
Cabinet production does not gain much from a cutting upgrade if sheet handling, part unloading, and batch organization stay messy. Large boards are awkward, labor-intensive, and easy to turn into a bottleneck if the saw area is not planned as part of the wider workflow.
Before you evaluate saw specifications, walk the floor and answer these questions:
- How do full sheets enter the cutting area? Is there a clear path from storage to the saw, or does material weave through other workstations?
- How are cut parts sorted by cabinet batch or order? Is there a staging area, or do parts pile up on the saw table waiting for someone to move them?
- Where do offcuts go so they do not interfere with active production? Is there a defined scrap flow, or do remnants accumulate and block access?
- How much operator time is spent moving material instead of releasing parts? Track this for a day and you will have a concrete number.
- Does the saw reduce labor pressure, or simply move the pressure to unloading and sorting?
In many cabinet shops, labor waste comes less from the blade itself and more from repeated lifting, repositioning, checking, and reorganizing. A panel saw becomes more valuable when it supports cleaner material flow rather than just faster cutting in place. If your bottleneck is loading and unloading, a faster cut cycle will not solve it.
Let us put some numbers on this. A standard 18mm melamine sheet weighs roughly 40 to 45 kilograms depending on dimensions. A cabinet shop cutting 30 sheets per day moves about 1,300 kilograms of material just in raw board. Add the cut parts—each carcass side, shelf, and partition gets handled at least once more when it leaves the saw. That is another 1,300 kilograms of movement. Total material handling per day approaches 2,600 kilograms. If an operator can comfortably handle about 500 kilograms per hour of sustained work, you are looking at over five hours of pure material movement per day. A panel saw with a powered roller table, an air-flotation table, or an automatic feeder can cut that handling time by 30 to 50 percent. That is the real productivity gain, not the difference between a 12-second and an 8-second cut cycle.
The layout question matters just as much. If sheets come from a storage rack on the opposite side of the shop, every sheet travels through the middle of the production floor. That creates congestion, increases the risk of surface damage, and forces other operators to work around the material flow. A dedicated material path from storage to the saw, with a clear exit route for finished parts, is worth more than an extra meter of cutting capacity on the machine itself.
Batch Logic and Changeovers Must Match the Machine
Cabinet factories often assume that higher-volume machinery automatically improves output. In reality, the result depends on how orders are organized.
Panel saws are strongest when the business can group work into stable batches, standard module families, or recurring cabinet formats. That structure lets the cutting area operate with less interruption and keeps downstream processes fed in an orderly way. If you can cut all 600mm-wide carcass sides in one run, then all 400mm shelves in the next, the saw pays for itself through reduced setup and better flow.
If the production model changes sizes and specifications constantly, the buying decision needs more caution. Frequent changeovers do not automatically rule out a panel saw, but they make job preparation, part identification, and release discipline more important. A factory that cannot maintain order around changing cut lists will not capture the full value of a dedicated panel-sizing machine.
The real issue is not whether changeovers exist—every factory has them. The issue is whether the order mix still gives the saw enough structured work to improve the line as a whole. If you are cutting 30 different panel sizes in a single morning with no logical grouping, a panel saw will not fix that underlying disorganization.
Think about changeover time in concrete terms. A manual panel saw with a digital readout and a mechanical fence takes about two to three minutes to set up for a new dimension. An automated saw with a programmable fence and a push-through system can change dimensions in under thirty seconds. If you are running 20 different sizes per day, that is the difference between 40 to 60 minutes of setup time versus 10 minutes. Over a week, that is three to four hours of cutting time recovered. Over a year, that is over 150 hours of additional productive capacity from the same machine.
But the batch logic question goes beyond setup time. It affects how parts flow to the next operation. If you cut all carcass sides first, then all shelves, the edgebander can run continuously on one width before changing over. If you cut mixed sizes in a single run, the edgebander has to change settings constantly, which slows it down and increases the risk of setup errors. The panel saw decision is therefore not just about the saw itself—it is about whether the cutting schedule supports stable downstream runs.
For shops that cannot achieve perfect batching, look for a saw with features that reduce changeover pain. A programmable fence with stored cutting patterns, a digital positioning system, and a software package that generates optimized cut lists can all help. These features do not eliminate the need for batch discipline, but they reduce the penalty for mixed runs.
Reduce Operator Dependency, Don’t Hide It
Another major selection factor is how much your current cutting process depends on individual operator skill. In cabinet production, that dependency is a hidden risk.
If one experienced operator carries too much of the accuracy burden, you will see unstable results across shifts, inconsistent quality during busy periods, and slow onboarding for new staff. A panel saw investment often makes the most sense when management wants cutting quality to be more process-driven and less dependent on manual correction.
This matters especially in growing cabinet businesses. A cutting method that works with one highly capable operator may not scale cleanly when volumes rise, shifts expand, or labor turnover increases. The better buying question is whether the saw helps standardize output across normal production conditions, not just under ideal conditions with your best person at the controls.
Consider the difference between a manual sliding table saw and a semi-automatic panel saw. On a manual machine, the operator positions the fence, sets the stop, aligns the sheet, and pushes it through the blade. Accuracy depends on how carefully the operator performs each step. Fatigue, distraction, or rushing all introduce variation. On a panel saw with a programmable fence and a powered pusher, the operator loads the sheet, enters the dimension, and the machine positions the fence automatically. The human element shifts from precision positioning to loading and unloading. That is a fundamental change in the skill requirement.
For a shop with two shifts, this matters even more. The second shift often has less experienced operators. If the saw requires the same skill level as the day shift, you will see quality drift after 5 p.m. A machine that automates positioning removes that risk. The second shift operator can achieve the same accuracy as the day shift operator because the machine handles the critical positioning.
The labor market reality also plays into this decision. Experienced panel saw operators are hard to find and expensive to retain. If your cutting process depends on one or two people with specialized knowledge, you are exposed to turnover risk. A more automated saw reduces that exposure. It does not eliminate the need for a competent operator—someone still has to load sheets, manage the cut list, and handle the output—but it lowers the skill ceiling required for consistent results.
Evaluate the Workflow, Not Just the Machine
For cabinet production, the most useful evaluation is usually not a feature-by-feature machine comparison. It is a workflow comparison. Use this framework to assess whether a panel saw fits your operation:
| What to Evaluate | Why It Matters in Cabinet Production | What to Ask Internally |
|---|---|---|
| Part Repetition | Determines whether a dedicated panel-sizing process will be used often enough to matter | Are most daily parts rectangular and repeated, or highly variable? |
| Downstream Sensitivity | Shows how much cutting variation affects the rest of the line | Do edge processing, drilling, or assembly regularly absorb sizing errors? |
| Material Handling | Affects labor efficiency, pace, and organization around the saw | Is the current bottleneck cutting itself, or loading, unloading, and sorting? |
| Batch Discipline | Determines whether the saw can support stable production flow | Can jobs be grouped in a way that keeps cabinet parts organized? |
| Labor Model | Clarifies whether the factory needs less operator-dependent cutting | Are results too dependent on one skilled person or one shift? |
| Floor Layout | Decides whether the saw improves flow or creates congestion | Can sheets enter and finished parts leave the area without confusion? |
| Growth Direction | Prevents buying for today only and missing future production reality | Is the factory moving toward more standardization, more volume, or more customization? |
Factories that answer these questions clearly usually make better saw decisions than factories that start with brochure comparisons.
Let us walk through how this framework plays out in a real production scenario. A mid-sized cabinet shop runs about 40 cabinets per week, mostly kitchen and bathroom units. The part mix is roughly 80 percent rectangular carcass components and 20 percent custom pieces like angled panels, curved ends, or decorative elements. The shop currently cuts everything on a sliding table saw with a single experienced operator. The edgebander runs behind the saw, and the drilling machine sits further down the line.
The workflow evaluation reveals several issues. First, the operator spends about 40 percent of the shift measuring, marking, and repositioning sheets rather than cutting. Second, the edgebander frequently stops because parts arrive with slight size variations that require manual adjustment. Third, the drilling machine operator has to re-measure every part before drilling because hole positions are inconsistent. Fourth, the shop has a second shift coming online next quarter, and the current operator will not be available for all shifts.
In this scenario, a panel saw with a programmable fence and a powered pusher addresses all four issues. It reduces setup time, improves dimensional consistency, and lowers the skill requirement for accurate cutting. The saw does not solve the material handling problem—the shop still needs a better staging area and a clear path for finished parts—but it removes the biggest source of downstream variation.
Now consider a different scenario. A custom cabinet shop produces mostly one-off pieces for architects and interior designers. Each job has different dimensions, different materials, and different edge treatments. The shop cuts about 15 sheets per day, but every sheet has a unique cut list. The owner is considering a panel saw because a sales representative told them it would improve efficiency.
The workflow evaluation tells a different story. The part repetition is low—maybe 30 percent of parts are repeated within a single job, and almost nothing repeats across jobs. The downstream sensitivity is moderate, but the real bottleneck is not cutting accuracy—it is the design and quoting process that happens before any material is cut. A panel saw would sit idle for long periods while the shop handles custom shapes on a CNC router or a manual saw. The investment would not pay back because the machine would not be used enough to justify its cost.
In this scenario, the better investment is a CNC nesting machine that can handle both rectangular parts and custom shapes, or a well-managed sliding table saw with a digital readout for occasional accuracy needs. The panel saw is the wrong tool for this production model, not because it is a bad machine, but because it does not match the workflow.
What Usually Matters Less Than Buyers Think
Some factors are important, but they are often given too much weight compared with the production basics above:
- The most aggressive speed claim, without checking whether the rest of the line can keep up
- A machine’s visual size or appearance, without confirming that cabinet part flow actually justifies it
- Buying for occasional peak demand instead of the daily production pattern
- Treating cutting as a standalone department instead of part of a cabinet-making system
- Assuming more automation always means better results, even when job organization is weak
These points are not irrelevant. They are just secondary. In cabinet manufacturing, the biggest gains usually come from repeatability, workflow control, and stable downstream handoffs.
Take the speed question as an example. A saw that cuts a 2.5-meter sheet in 12 seconds versus one that takes 18 seconds sounds like a 50 percent improvement. But if the operator spends 40 seconds loading and unloading each sheet, the total cycle time is 52 seconds versus 58 seconds—an 11 percent difference, not 50 percent. And if the downstream operations cannot keep up with the faster feed rate, the saw will simply create a pile of parts waiting for the edgebander. The speed advantage disappears into work-in-process inventory.
The automation question deserves similar scrutiny. A fully automated panel saw with a loading system, a cutting sequence, and an unloading stacker can run with minimal operator intervention. But that automation only pays off if the shop has enough volume to keep the machine running continuously. A shop cutting 10 sheets per day will not benefit from a system designed for 100 sheets per day. The machine will spend most of its time idle, and the maintenance cost will exceed the labor savings.
The peak demand trap is also common. A shop that handles a surge of work in the spring and then drops to half volume in the summer may be tempted to buy a saw sized for the peak. That decision leaves the machine underutilized for most of the year. The better approach is to size the saw for the average production level and manage peak demand with overtime or temporary capacity.
When Another Cutting Approach May Be the Better Fit
A panel saw is not the best answer in every cabinet environment. Another approach may make more sense when:
- The shop handles mostly one-off custom work
- Irregular or nested shapes are a large share of production
- The main problem is not front-end cutting, but a later bottleneck
- The business needs maximum flexibility more than stable high-volume sizing
- The order mix changes so often that structured batching is difficult to maintain
This is an important discipline point for buyers: the right machine is the one that solves the real production constraint. In some factories, that will clearly be a panel saw. In others, the smarter move may be a more flexible cutting workflow. If your shop is producing one-off custom cabinets with irregular dimensions, a CNC nesting machine or even a well-managed sliding table saw may serve you better than a dedicated panel saw that thrives on repetition.
The CNC nesting route deserves a closer look for shops with a high share of custom work. A nesting machine cuts parts directly from a full sheet using a router spindle, which means it can produce rectangular parts and irregular shapes in the same program. The tradeoff is that nesting machines are generally slower than panel saws for straight-line cuts on rectangular parts. A nesting machine might take 30 seconds to cut a part that a panel saw produces in 10 seconds. But if 40 percent of your parts are irregular shapes that a panel saw cannot handle at all, the nesting machine becomes the more versatile option.
The sliding table saw route makes sense for shops that need accuracy but not high volume. A modern sliding table saw with a digital readout and a scoring blade can hold tolerances of a few tenths of a millimeter when operated carefully. The setup time is longer than a panel saw, but for a shop cutting 10 to 15 sheets per day, the difference is manageable. The capital cost is significantly lower, which matters for a shop that is still growing and may not have the cash flow to support a larger investment.
There is also the option of combining approaches. Some shops run a panel saw for the bulk of their rectangular parts and a CNC router for custom shapes and nested cutting. This hybrid approach requires more floor space and a higher total investment, but it gives the shop the best of both worlds: high throughput on standard parts and flexibility for custom work. The decision comes down to whether the volume of custom work justifies the second machine.
Production Takeaway: Panel Saws for Cabinet Production
For cabinet production, what matters most in a panel saw decision is usually not the saw alone. It is the fit between the saw and the factory’s real operating model.
If the work is built around repeated rectangular parts, if downstream processes depend on stable sizing, and if the business needs cleaner material flow with less operator-dependent variation, a panel saw is often a logical investment. If the factory is still highly custom, highly irregular, or loosely organized around changing jobs, the gains may be smaller than expected.
The practical test is simple: judge the machine by the quality of the line it creates after the cut. In cabinet manufacturing, that is where the real value shows up. If you are evaluating dedicated panel saws for your cabinet line, start with the workflow questions above before you compare specifications. The answers will tell you more about the right machine than any spec sheet will.
Before you sign the purchase order, run one more check. Take your current cut list for a typical week and simulate how it would run on the saw you are considering. Count the number of setups, the total cutting time, and the material handling steps. Then do the same simulation for the next-best alternative. The comparison will not be perfect—you are estimating, not measuring—but it will force you to think through the production reality rather than the sales pitch. That exercise alone is worth the time you invest in it.