
 Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
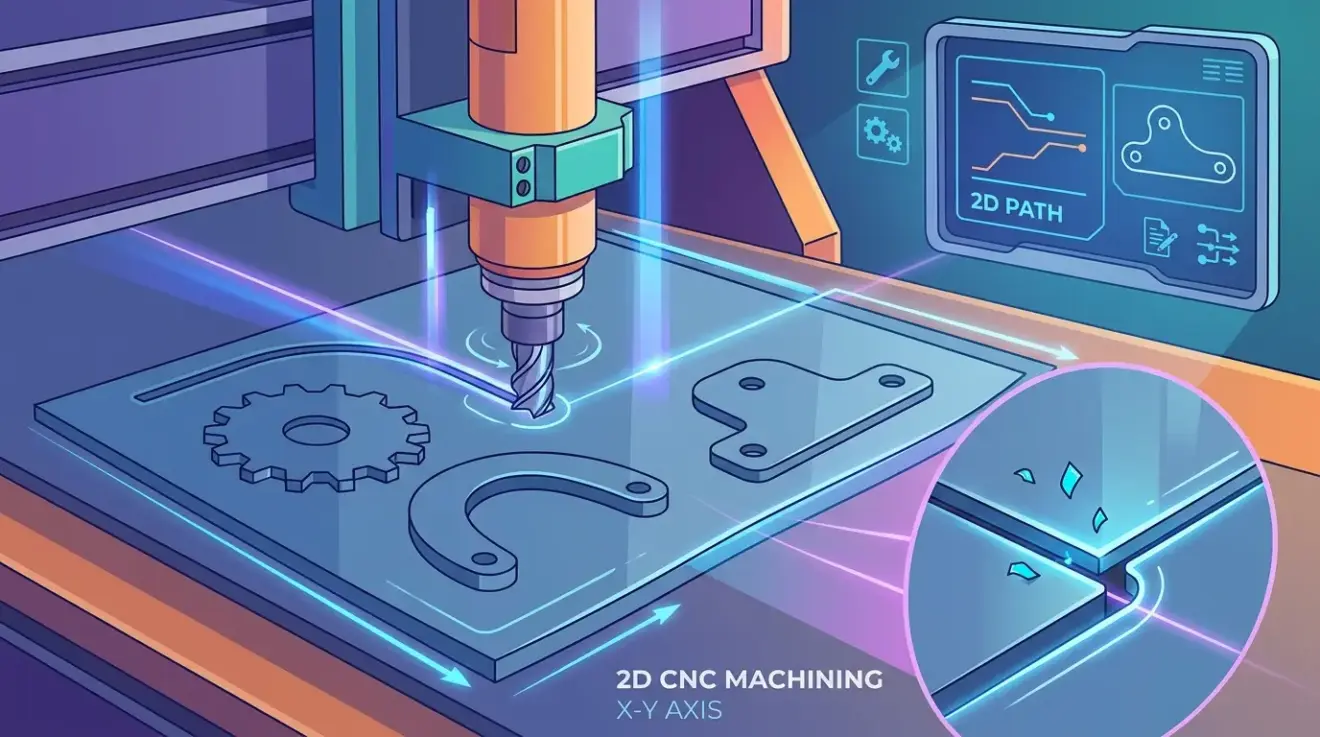
What Is 2D CNC Machining?
Saturday, 25 April 2026
Mislabeling flat or profile-driven parts as 3D work inflates quoting time, complicates CAM prove-out, and adds fragile setup steps that the geometry never required. This article cuts through the floor-level confusion between true 2D, 2.5D, and 3D classifications, showing why that distinction drives machine selection, tooling strategy, and inspection burden. For shops cutting panels, brackets,
- Published in Blog
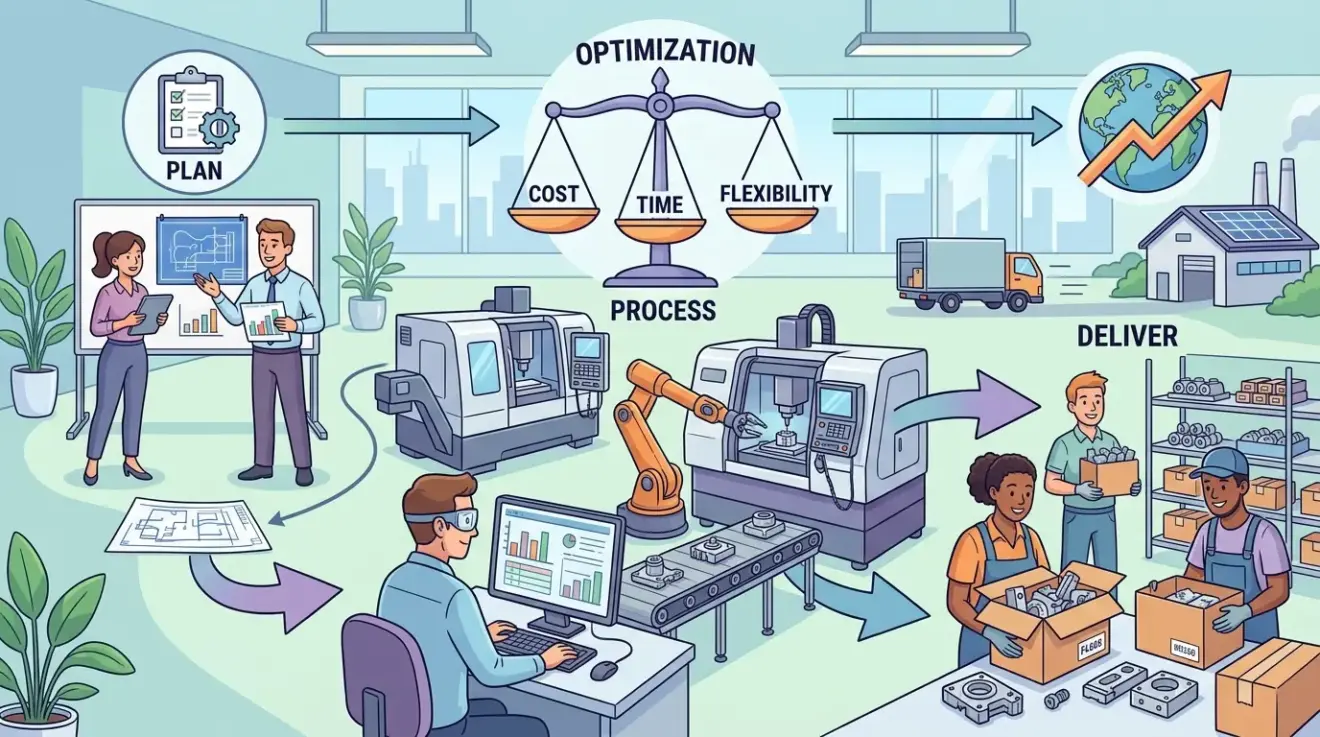
Small Batch CNC Machining: How to Balance Cost, Lead Time, and Flexibility
Saturday, 25 April 2026
Small-batch CNC machining fails more often in the quoting office and the scheduling queue than at the spindle, yet most buyers still evaluate suppliers purely on cycle time and price per part. This article confronts the real coordination problem: setup burden, drawing clarity, part-family grouping, and revision control determine cost and lead time long before
- Published in Blog
Stainless Steel Laser Cutter: What To Look For In A Production Machine
Saturday, 25 April 2026
Stainless steel fabrication punishes weak machine selection faster than carbon steel work because visible parts headed for kitchen equipment, architectural panels, or elevator cabs will not tolerate discolored edges, burrs, or batch-to-batch geometry drift. A machine that impresses during a controlled demo can still fail when nested thin-gauge sheets, dense contours, and repeat orders expose
- Published in Blog
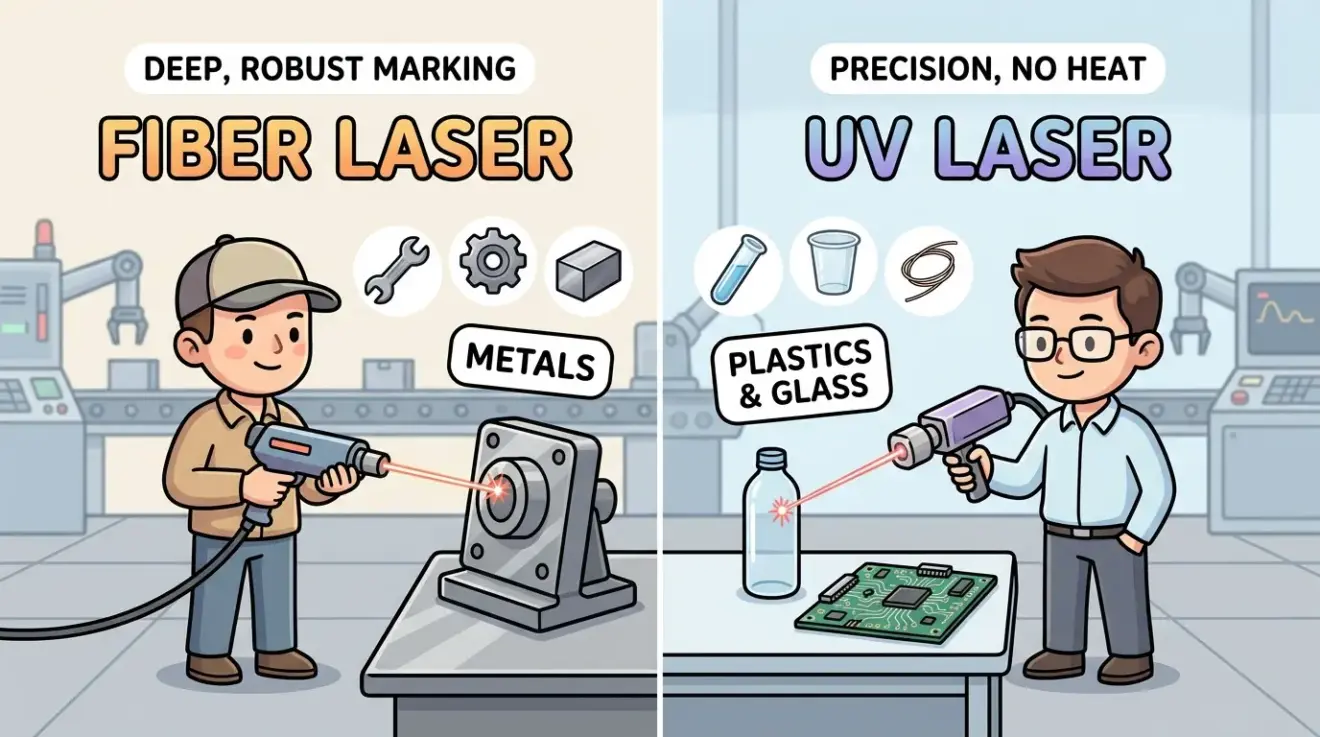
Fiber Laser Marking Machine vs UV Laser Marking Machine: Which Fits Your Production Workflow?
Saturday, 25 April 2026
Selecting between fiber and UV laser marking is a production-fit decision that hinges on how each wavelength interacts with your actual material surface, not on which technology sounds more advanced. Get the match wrong and the consequences surface quickly on the line: discoloration on coated parts, heat damage on thin plastics, or codes that pass
- Published in Blog
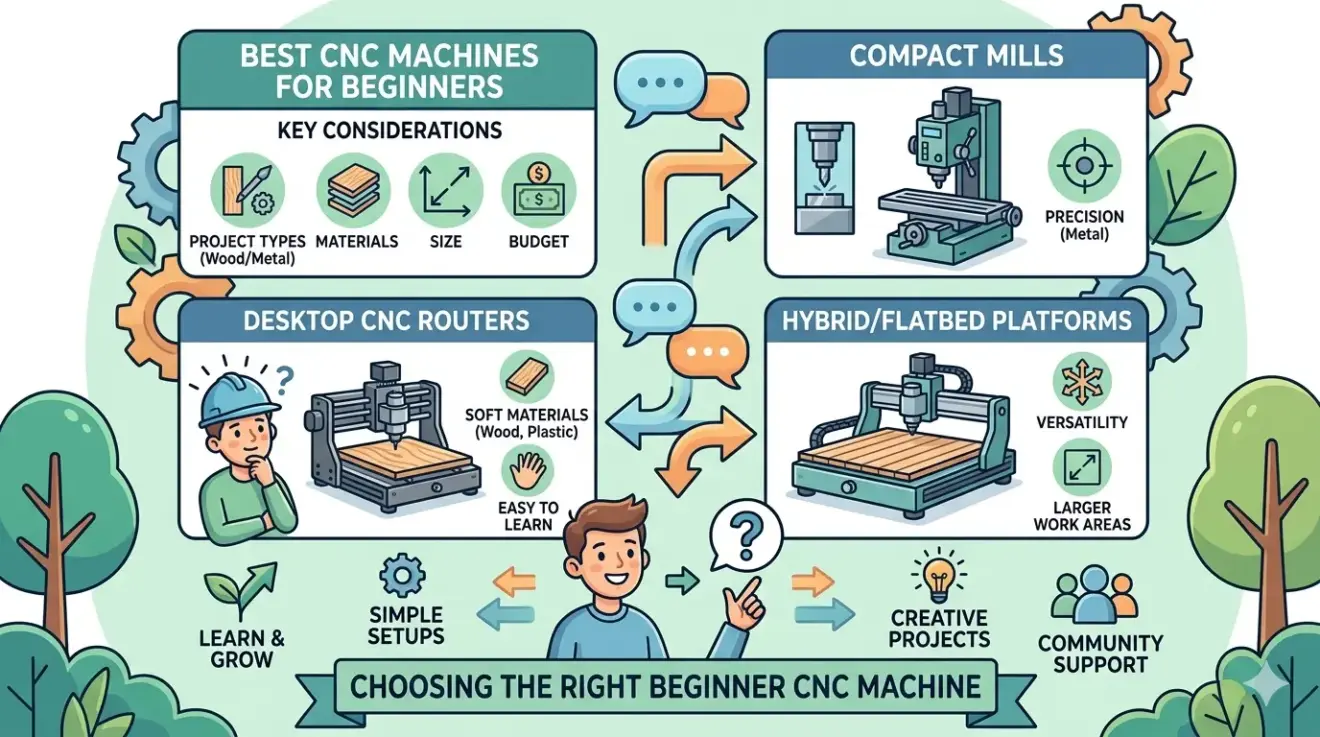
Best CNC Machines for Beginners: Router, Mill, or Desktop Platform?
Friday, 24 April 2026
First-time CNC buyers often assume “beginner” defines a single machine type, but the label hides a sharper problem: a sign shop cutting sheet goods, a prototype team machining small metal parts, and a classroom teaching fundamentals are entering three different trades. Choosing by popularity or price instead of by material format and workflow teaches the
- Published in Blog
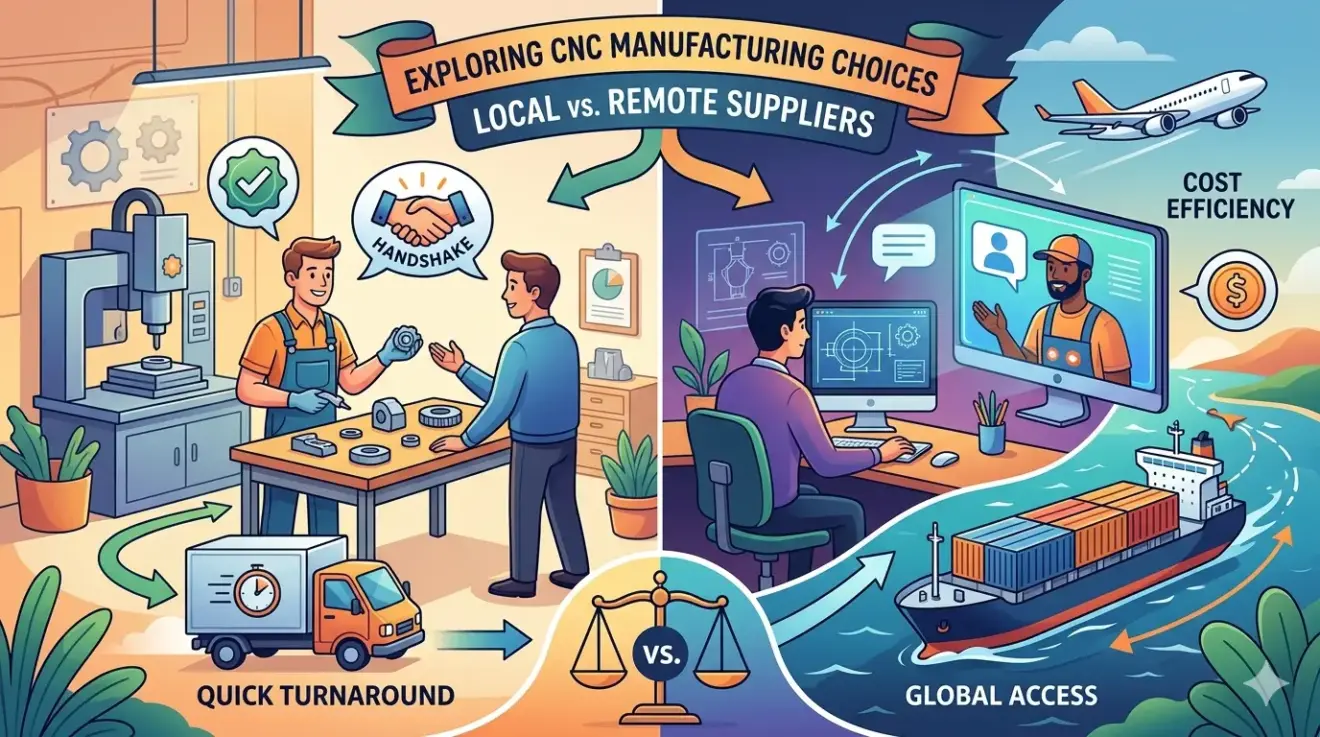
CNC Services Near Me vs Remote Suppliers: Which Is Better for Your Project?
Friday, 24 April 2026
Most CNC sourcing debates start with a map, but the real fault line is correction cost. When a part is still teaching you something—a cosmetic face that surprises, a tolerance stack that drifts, a fit issue that only appears at assembly—distance changes the economics of every recovery loop. Local suppliers shorten the time between discovery
- Published in Blog
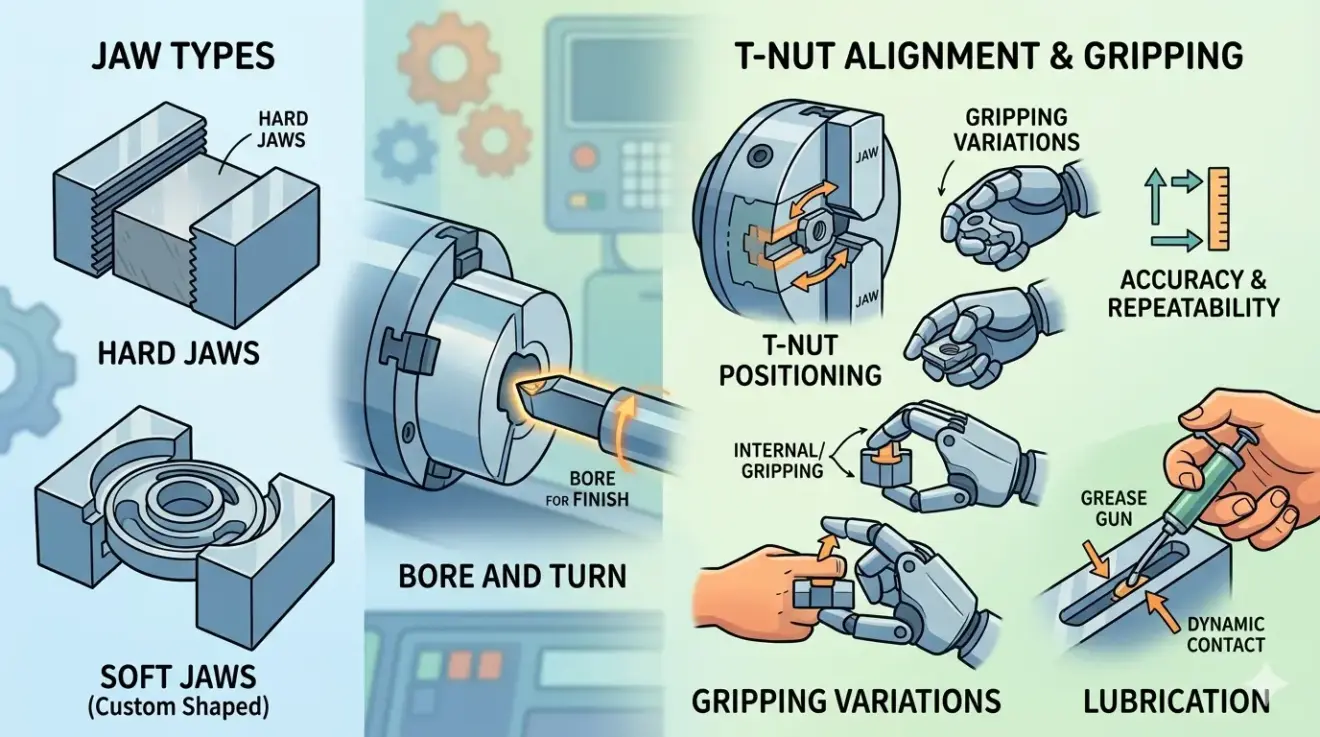
What Is CNC Jaw Setting?
Friday, 24 April 2026
CNC jaw setting rarely announces itself as the culprit when turned parts drift, chatter, or show taper; it masquerades as program error, insert wear, or spindle trouble, sending shops down the wrong diagnostic path. This article forces that issue into the open by treating chuck-jaw preparation as a formal process-control step rather than a setup
- Published in Blog
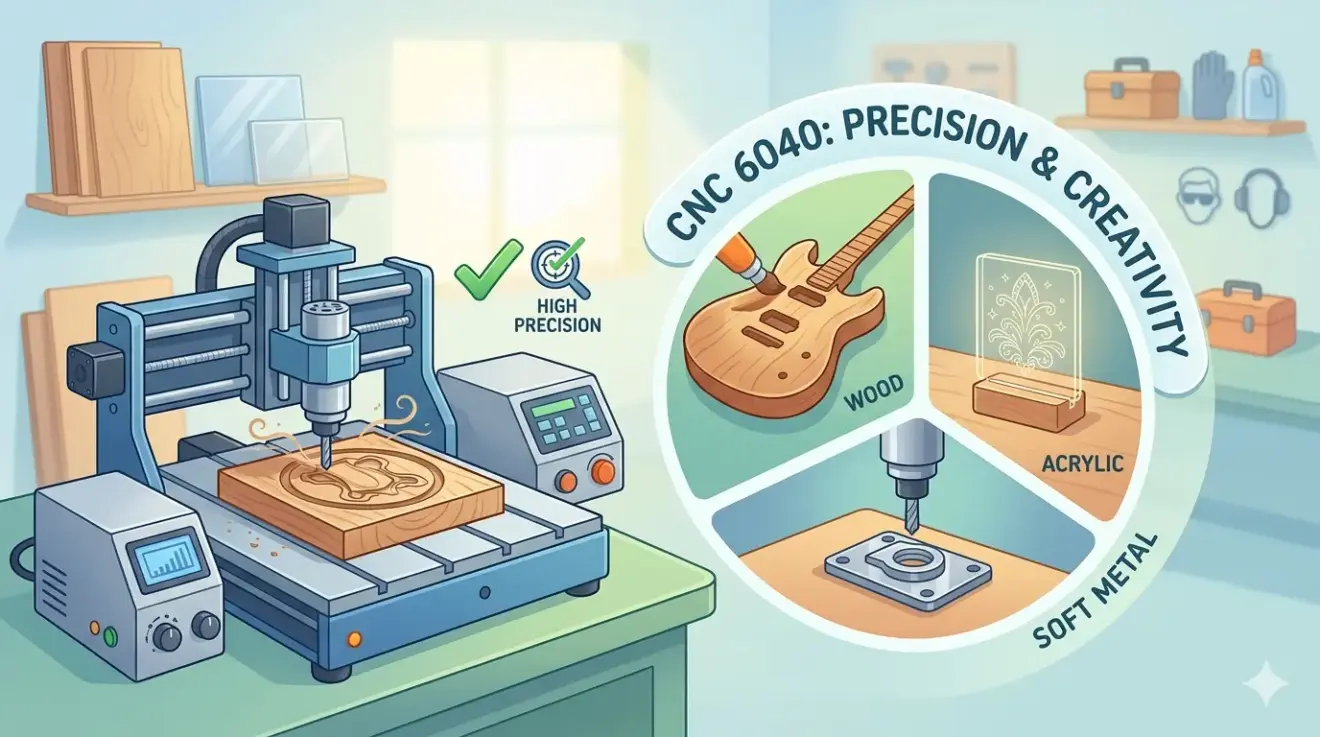
CNC 6040 Router Guide: Capacity, Accuracy, and Typical Use Cases
Friday, 24 April 2026
Buyers often treat the 6040 label as a promise of greater capability, but it is really just a nominal work-zone envelope that says nothing about usable table space, rigidity under load, or repeatable accuracy. Before you commit to this size class, you need to audit how much of that travel survives real clamping, dust-shoe clearance,
- Published in Blog
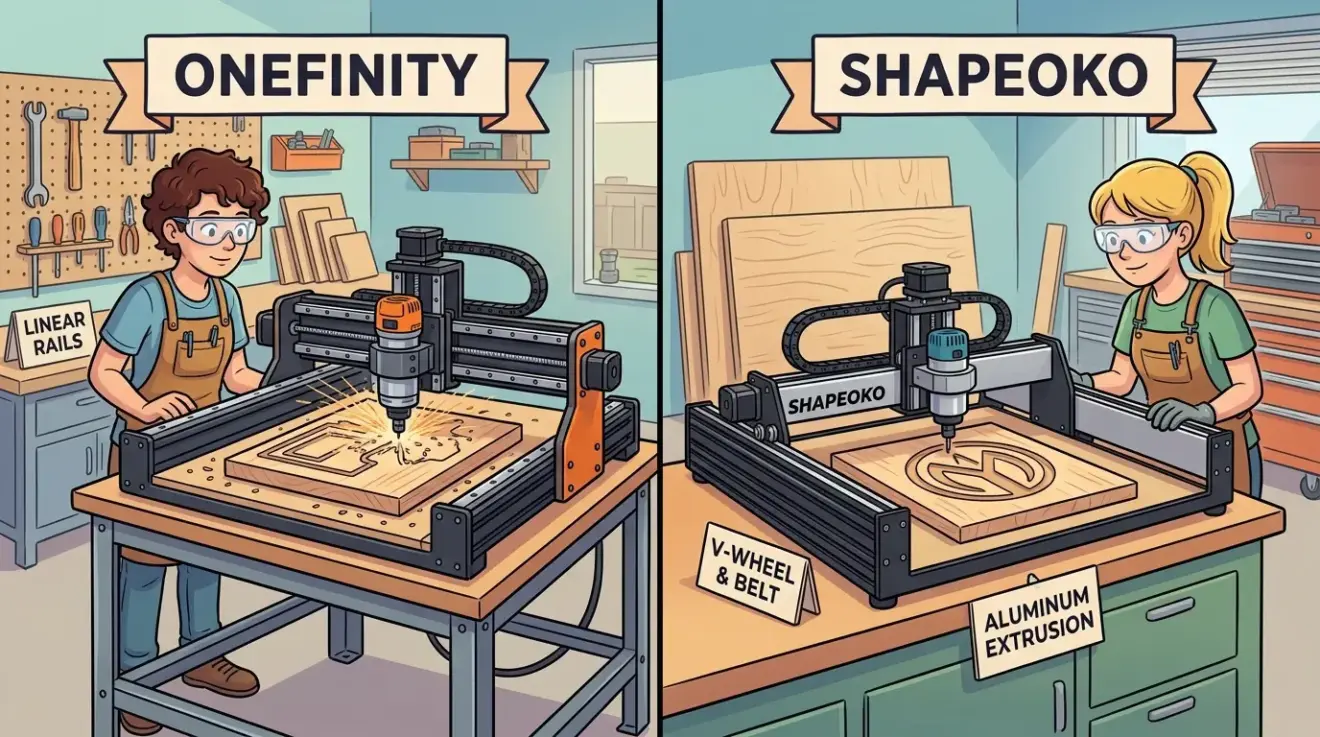
Onefinity CNC vs Shapeoko: Which Hobby CNC Platform Fits Better?
Friday, 24 April 2026
Before weighing Onefinity against Shapeoko on rigidity or community size, buyers in the hobby-to-light-shop CNC class need to settle a more practical question: which platform matches how you will actually work, learn, and troubleshoot over months of use. This comparison is not about winning a spec-sheet battle. It is about whether you prefer a hands-on
- Published in Blog
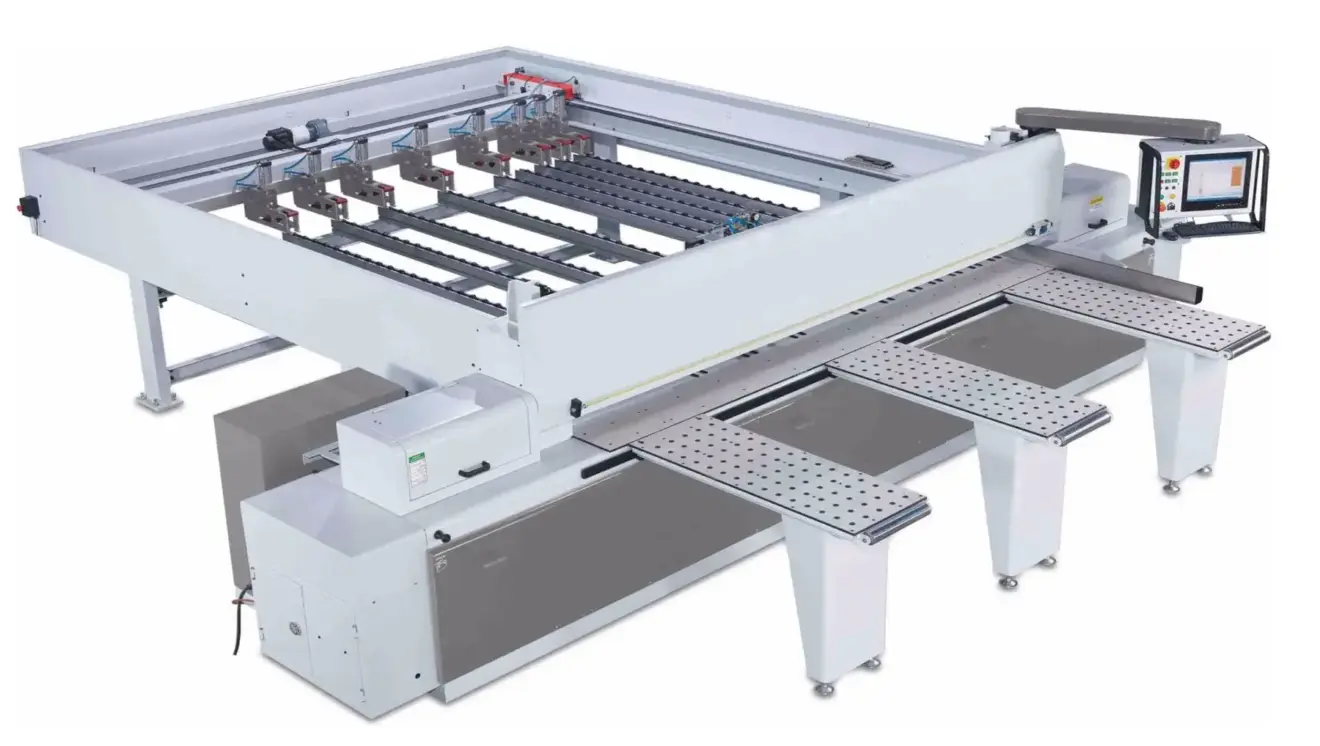
Panel Saw vs. Beam Saw: What Is the Real Difference?
Friday, 24 April 2026
When you request quotes for panel-sizing equipment, the terms “panel saw” and “beam saw” often appear interchangeably, yet that loose vocabulary can derail your entire procurement strategy. This article cuts through the naming confusion to clarify that a beam saw is a specific, automated subset within the broader panel-saw category, distinguished by its rigid beam,
- Published in Blog
CNC Lab, CNC Exchange, and Small-Market CNC Search Terms: What Buyers Are Actually Looking For
Friday, 24 April 2026
Small-market CNC search terms like “CNC lab” and “CNC exchange” rarely reflect an actual machine requirement. Instead, they expose a buyer stalled between four distinct paths: learning the technology, screening used equipment, shortlisting new machinery for a defined workload, or outsourcing production entirely. The problem is that all four searchers type nearly identical queries and
- Published in Blog
What Is a CNC Writing Machine?
Friday, 24 April 2026
The buying question comes before comparing gantries, axes, or control interfaces, define the actual output your shop needs. A CNC writing machine places visible lines, symbols, or text on a surface without removing material, while routers cut away stock and engravers alter the surface itself. Confusing these categories leads to costly missteps: a router optimized
- Published in Blog
How to Choose Edge Banding Equipment for PVC, ABS, and Melamine Applications
Friday, 24 April 2026
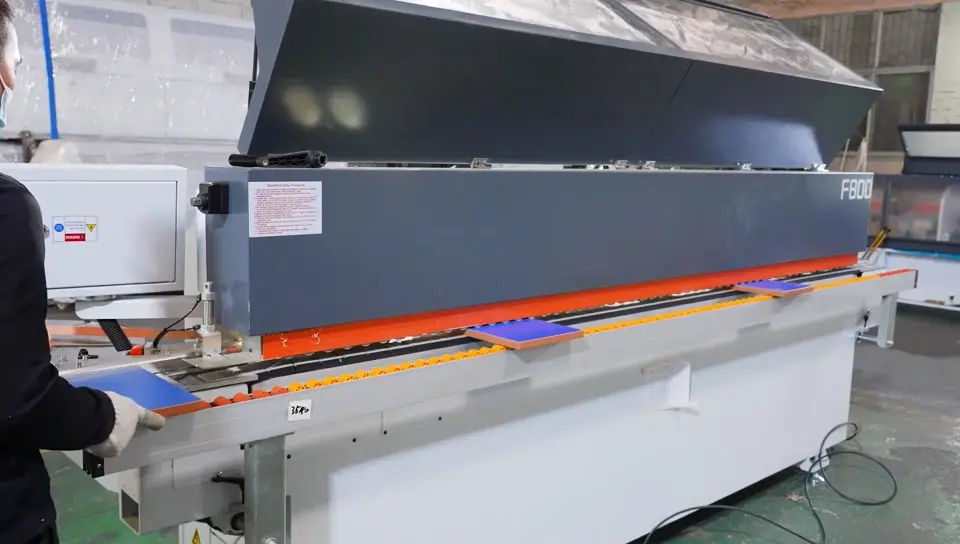
Selecting edge banding equipment for a mixed PVC, ABS, and melamine panel line fails when buyers prioritize automation levels over the finish standard each material demands. The machine must handle PVC’s volume-driven adhesion needs, ABS’s stricter visible-edge appearance, and melamine’s low tolerance for upstream saw defects—all while reducing manual scraping and rework. Before comparing feature
- Published in Blog
What Makes Industrial CNC Equipment Worth The Investment?
Friday, 24 April 2026
Every panel-processing shop that still relies on manual setup knows the hidden tax: operators re-measure drifted batches, edgebanders compensate for half-millimeter width swings, and assembly crews shim parts that should fit. Individually, these corrections seem minor; cumulatively, they become structural cost buried in labor, rework, and material loss. This article walks through the real investment
- Published in Blog
3018 CNC Milling Aluminum: What Actually Works on a Small Machine
Friday, 24 April 2026
Before you tune spindle speeds or debate feed rates on a 3018, the real decision is whether your aluminum part belongs on that frame at all. This article separates realistic desktop work—learning coupons, small flat brackets, and one-off prototypes—from jobs that will collapse into chatter, chip recutting, and operator overload. It identifies the four failure
- Published in Blog
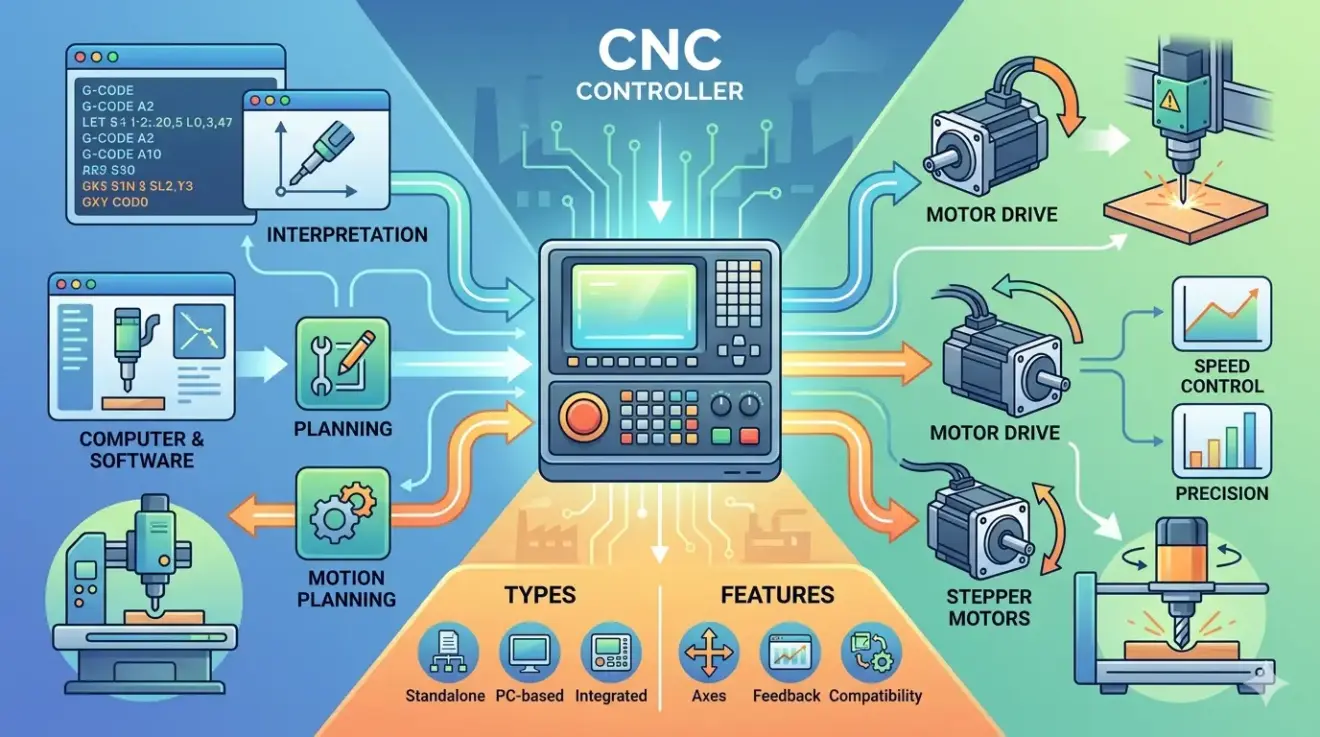
CNC Controller Explained: What It Does and How to Choose One
Friday, 24 April 2026
Every CNC machine purchase ultimately hinges on the control layer, yet it is often the least-examined line in a quote. This article cuts through interface hype to show why machine state clarity, motion blending, alarm recovery, and peripheral integration determine whether a router, cabinet line, or stone cell runs predictably across shifts. Buyers must weigh
- Published in Blog
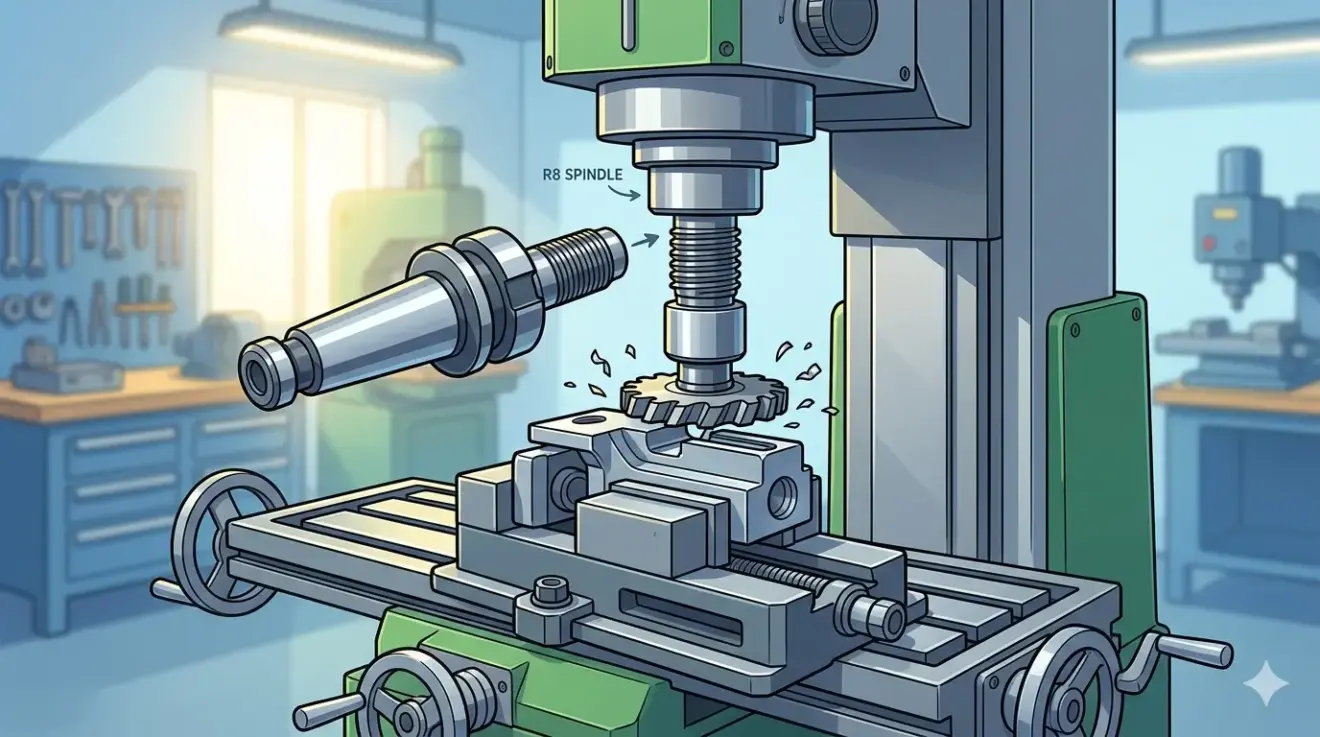
What Is an R8 Milling Arbor?
Friday, 24 April 2026
When you evaluate a used Bridgeport-style knee mill, toolroom mill, or benchtop CNC retrofit, the R8 spindle interface reveals the machine’s true operating model before you ever cut a part. This article explains why the arbor’s drawbar retention and load path signal a manual, operator-centered workflow rather than a production machining-center environment. Buyers who ignore
- Published in Blog
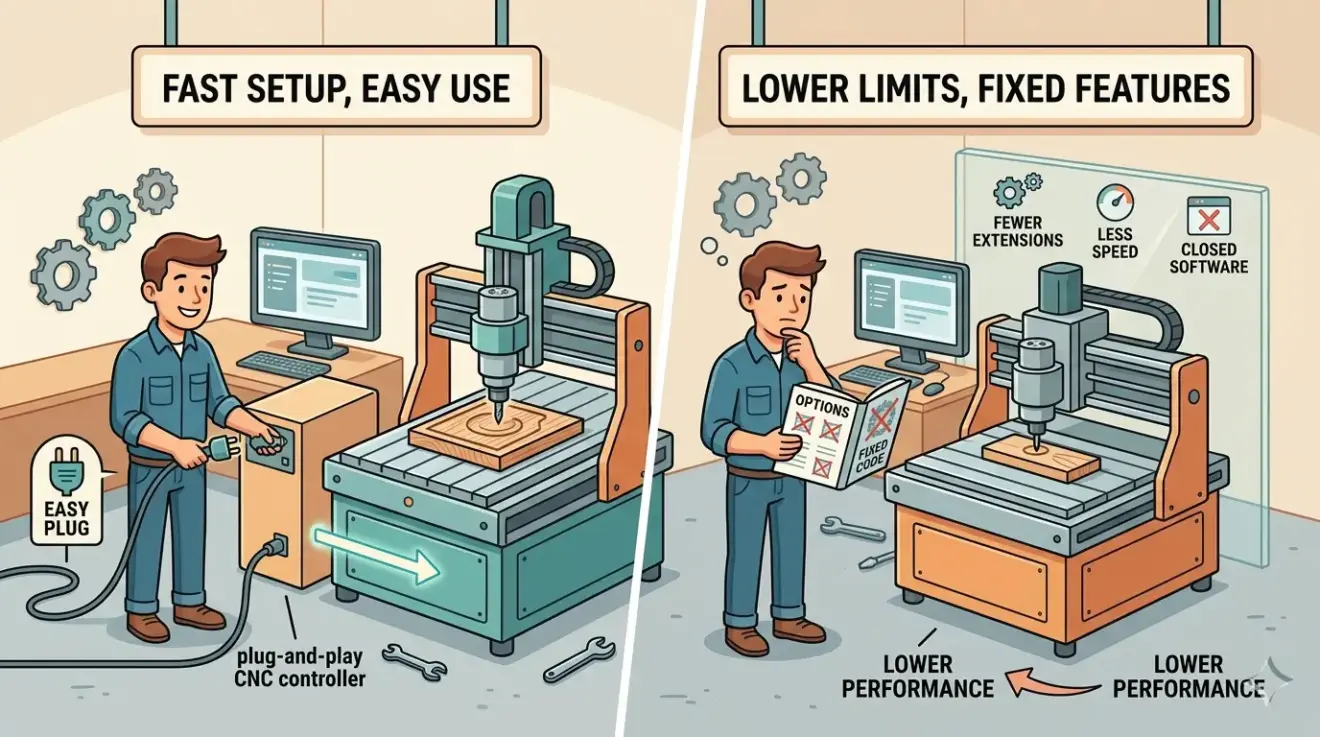
Plug-and-Play CNC Controllers: What They Save and What They Limit
Friday, 24 April 2026
Most shops comparing plug-and-play CNC controllers are not shopping for electronics; they are trying to escape project drag caused by stalled retrofits, new builds, or control cabinets that have become bottlenecks. The real decision is about who carries the complexity burden. Packaged controllers compress dozens of design choices around board compatibility, driver matching, and wiring,
- Published in Blog
How to Choose a Panel Saw Machine for Plywood, MDF, and Melamine Processing
Friday, 24 April 2026
Every cabinet shop, casework plant, or furniture factory that processes plywood, MDF, and melamine faces the same reality: the panel saw is the first quality gate in the entire production flow. If the saw produces panels that vary in width by half a millimeter, the edge bander struggles, the boring machine drills misaligned holes, and
- Published in Blog
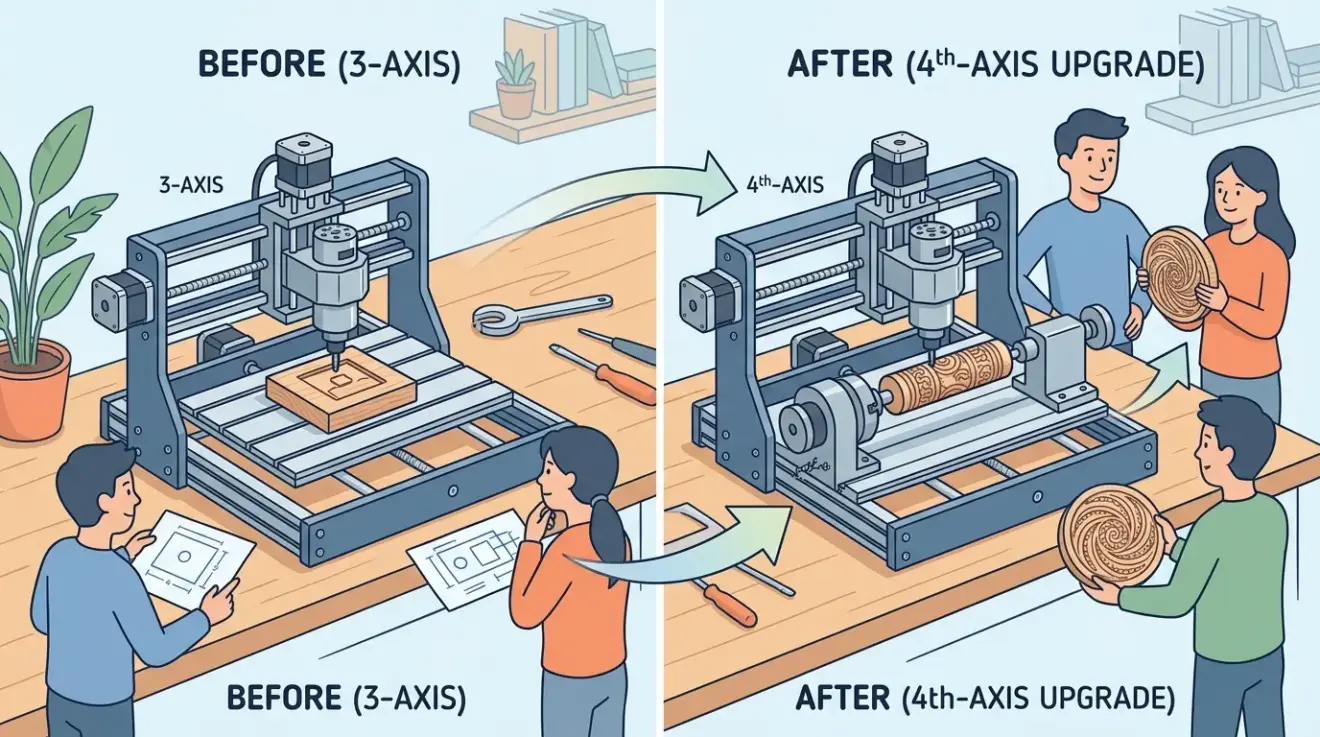
3018 4th Axis Upgrade Guide: Is It Worth Adding Rotary Capability?
Friday, 24 April 2026
Adding a rotary kit to a 3018 router is a classic trap: the hardware looks like a cheap path to cylindrical parts, but the real cost shows up later in calibration, clearance, and workflow friction. The decision hinges on whether you need indexed positioning for small round stock or true coordinated 4-axis cutting. Before you
- Published in Blog
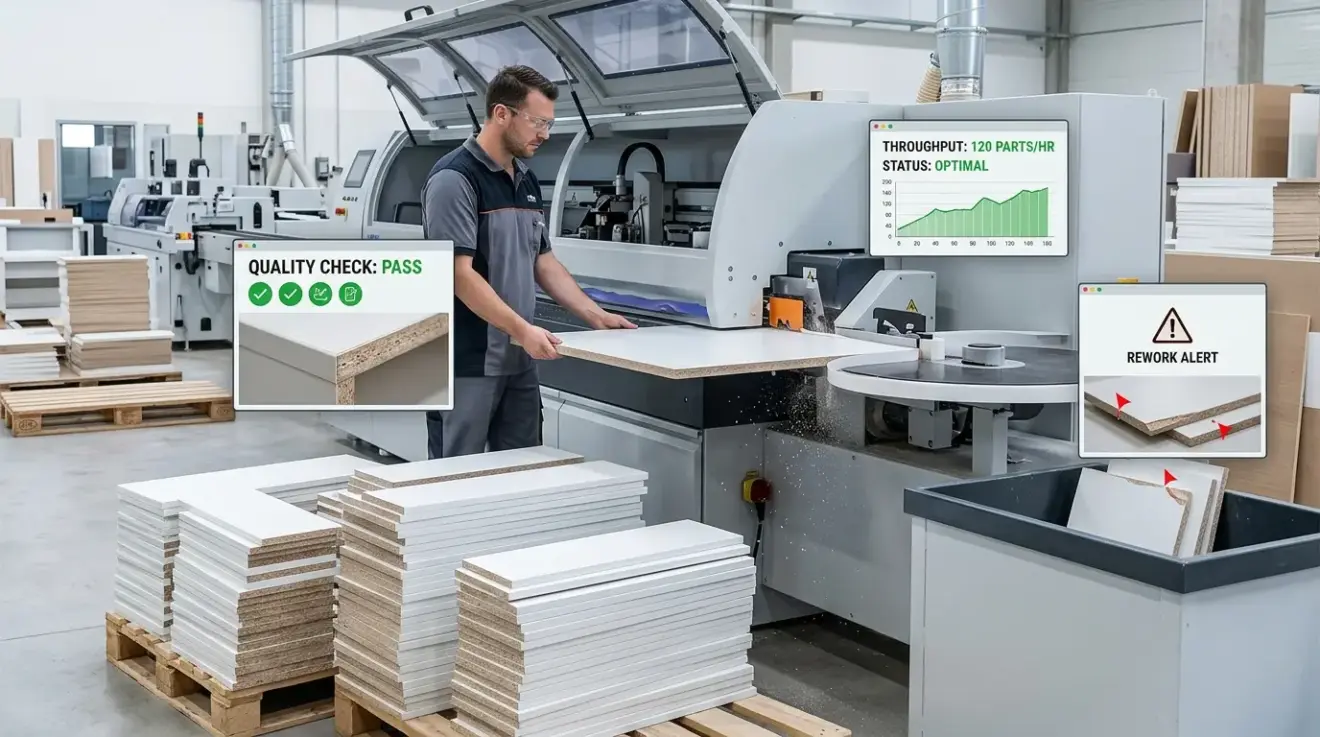
Edgebanding for Cabinet Production: What Affects Quality, Throughput, and Rework?
Friday, 24 April 2026
Edgebanding in cabinet production is where upstream panel quality, material selection, and finishing discipline converge into a single measurable outcome: rework. A chipped melamine face from a dull saw blade, an adhesive temperature mismatch, or an unplanned changeover between edge thicknesses will surface as visible glue lines, corner defects, or hand touch-up labor that was
- Published in Blog
Tegara 690X, PM-940M, and Other Small Mill Platforms: What Buyers Should Compare
Friday, 24 April 2026
Small mill buyers routinely compare travel numbers and model names while ignoring the ownership path each platform demands. This article separates three distinct routes—heavier toolroom-style mills, purpose-built compact CNCs, and retrofit or open-build systems—and shows why that distinction matters more than table size. The real decision hinges on control philosophy, coolant and chip strategy, and
- Published in Blog
Fiber Laser Marking Machine Applications for Industrial Parts
Friday, 24 April 2026
When machined housings, brackets, shafts, and fabricated frames move through inspection, assembly, and shipment, the mark on each part is the only thread linking it to its production records. Labels peel, ink smears, and stamps wear, forcing operators to stop and re-identify components manually while scanners reject unreadable codes. That is why fiber laser marking
- Published in Blog
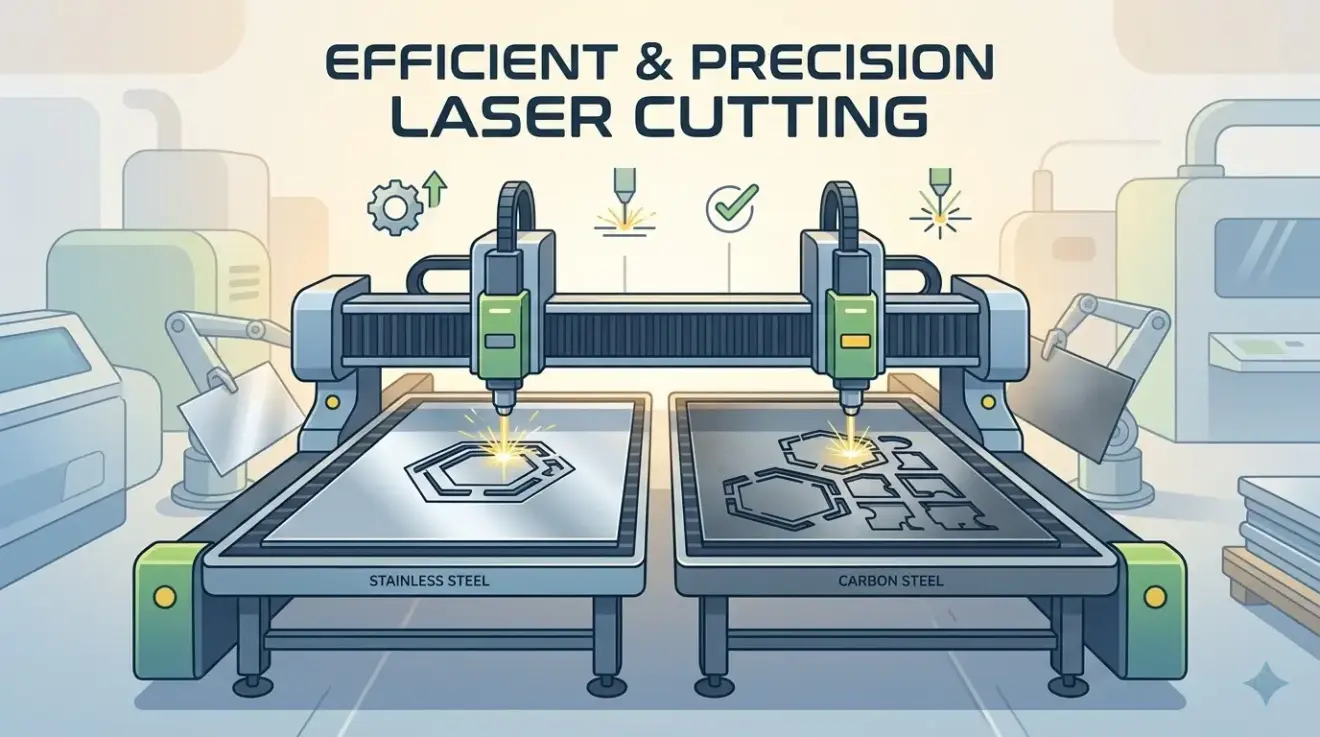
Industrial Laser Cutter for Stainless Steel and Carbon Steel
Thursday, 23 April 2026
Most mid-range fiber lasers will cut both stainless and carbon steel, but that capability alone does not solve the real problem: these materials push the process in opposite directions. Stainless jobs reward clean, low-oxidation edges for visible parts, while carbon steel work shifts priorities toward throughput, thickness range, and operating cost. A machine tuned for
- Published in Blog
CNC Plasma Table Buying Guide for Metal Cutting Shops
Thursday, 23 April 2026
Most metal cutting shops start a plasma table purchase by comparing bed sizes and traverse speeds, but those numbers rarely predict whether the machine will actually fit the production floor. This guide pushes the decision back to the cutting cell itself: how plate flows in, how operators load and clear the bed, how much cleanup
- Published in Blog
How to Choose an Acrylic Laser Cutter for Fabricators and Sign Makers
Thursday, 23 April 2026
Most acrylic laser purchases are approved on the strength of a single polished demo part, yet that sample reveals almost nothing about how a system will hold edge appearance, dimensional repeatability, and throughput across a real production week. Sign shops and acrylic fabricators evaluate output differently—one lives on visible edge clarity, the other on assembly
- Published in Blog
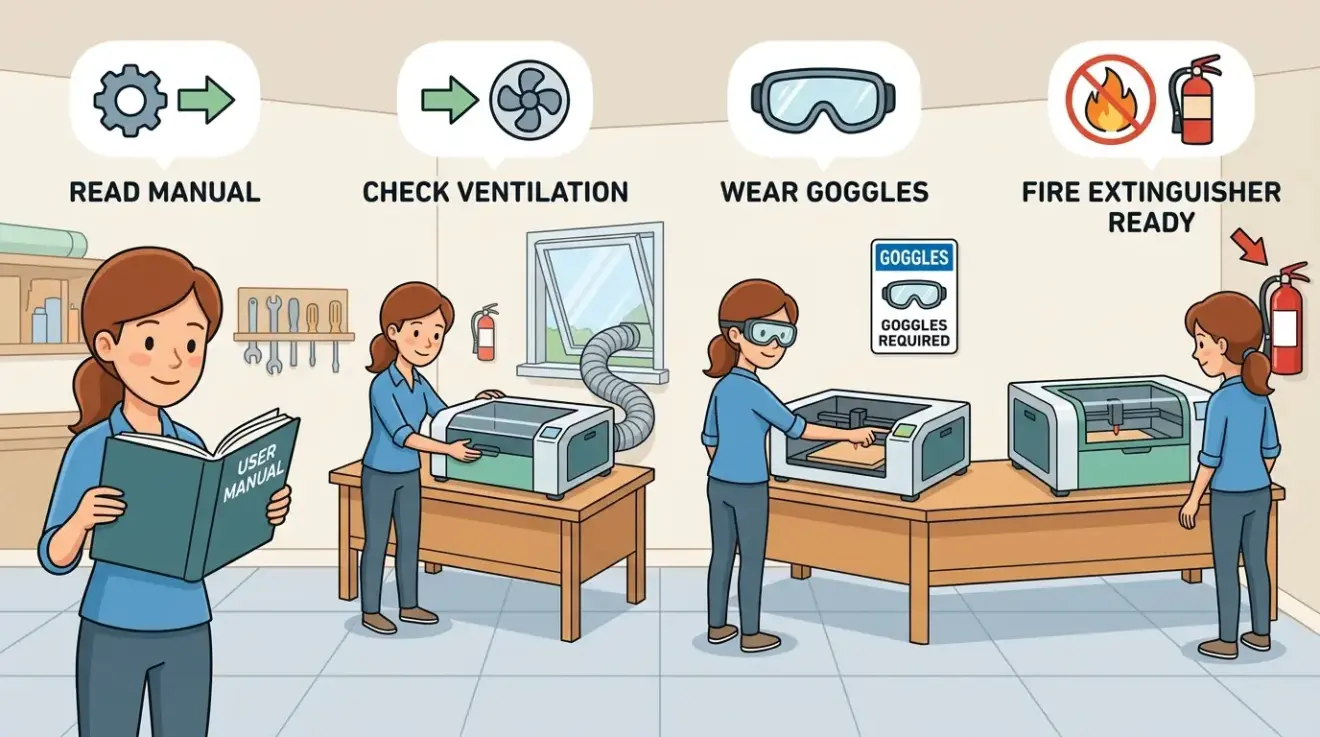
Home Laser Cutter Safety Guide for New Users: What To Control Before the First Cut
Thursday, 23 April 2026
Compact laser cutters bring production capability into spaces never designed for heat, smoke, and residue, yet the hazards sit outside the beam path: unknown material chemistry, overwhelmed extraction, combustible clutter, and unsupervised runs. Before you touch speed and power tables, you must control ventilation capacity, verify every sheet’s composition, and build a shutdown routine that
- Published in Blog
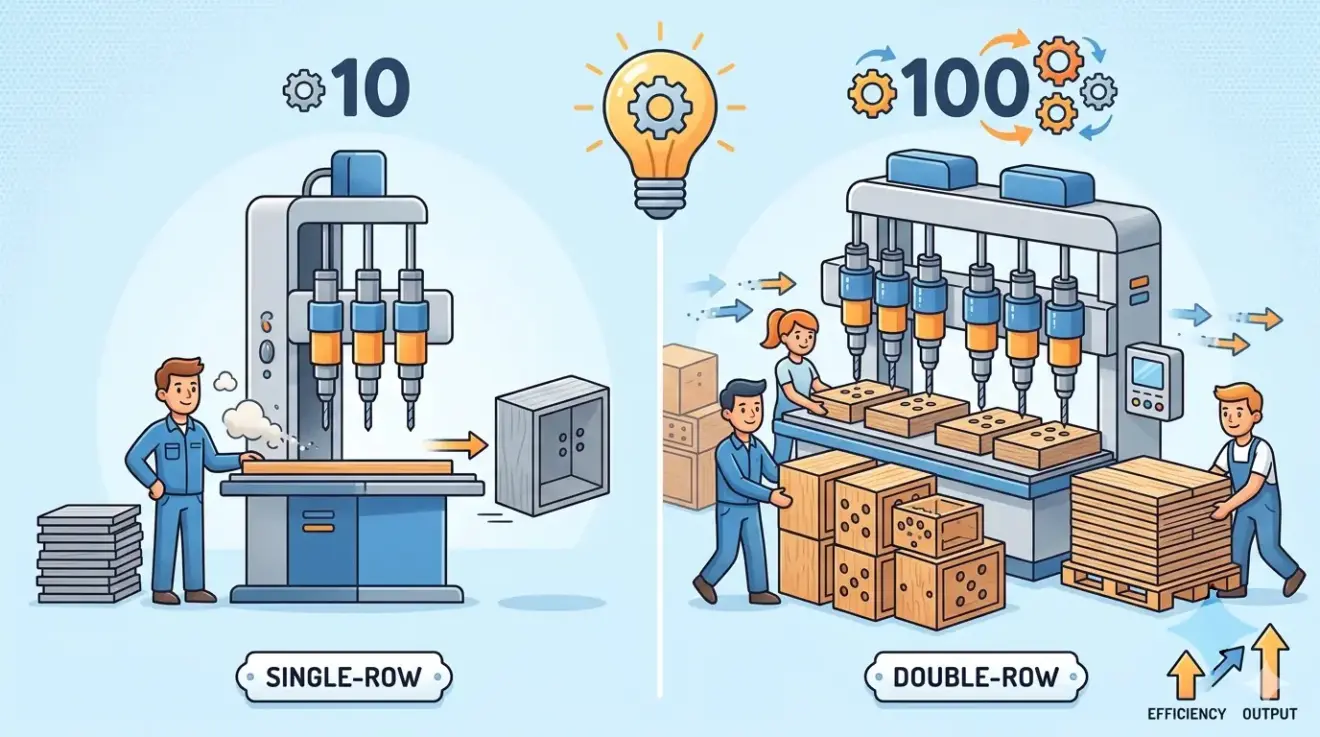
Single-Row vs. Double-Row Boring Machine: Which Configuration Matches Your Output?
Thursday, 23 April 2026
When cabinet panels pile up at the drilling station, the bottleneck is rarely spindle speedâit is how many times an operator must pick up, rotate, re-measure, and re-clamp each part before it moves toward assembly. That handling burden is exactly what separates single-row from double-row boring machines. The row count decision should hinge on your
- Published in Blog
DIY CNC Machine: What to Build Yourself and What to Buy Ready-Made
Thursday, 23 April 2026
Before you price out linear rails and ball screws, the real decision is whether you are buying a learning project or production capacity. Most DIY CNC cost comparisons ignore design time, debugging hours, compatibility surprises, and lost schedule trust when a machine fails to hold repeatability. That is why the article pushes you to define
- Published in Blog
CNC Router Machine Explained: Best Uses in Woodworking and Panel Processing
Thursday, 23 April 2026
Before you commit budget to a CNC router, you need to know whether your bottleneck is shape complexity or straight-line throughput. This article cuts through the marketing language to show why a router is a coordinate-based cutting platform, not just a fancier panel saw. It explains when the machine earns its keep by compressing handoffs
- Published in Blog
Woodpecker CNC and Similar Desktop Routers: What Buyers Should Expect
Thursday, 23 April 2026
Desktop routers like the Woodpecker sell access to CNC, not industrial output, and the gap between those two expectations is where most buying mistakes surface. This article forces a practical reclassification: small-format machines are entry-to-light-duty tools whose real cost appears in operator attention, setup time, repeatability limits, and dust discipline once commercial queues tighten. Before
- Published in Blog
Benchman VMC 5000, Maho 600, Devlieg 2B 36, and Legacy CNC Mills: When Older Machines Still Make Sense
Thursday, 23 April 2026
Older CNC mills like the Benchman VMC 5000, Maho 600, and Devlieg 2B 36 attract buyers with low listing prices, but that number never reflects the true cost of ownership. Rigging, electrical prep, control cleanup, repairs, and verification cuts quickly reshape the economics, and the real decision hinges on whether your shop can sustain the
- Published in Blog
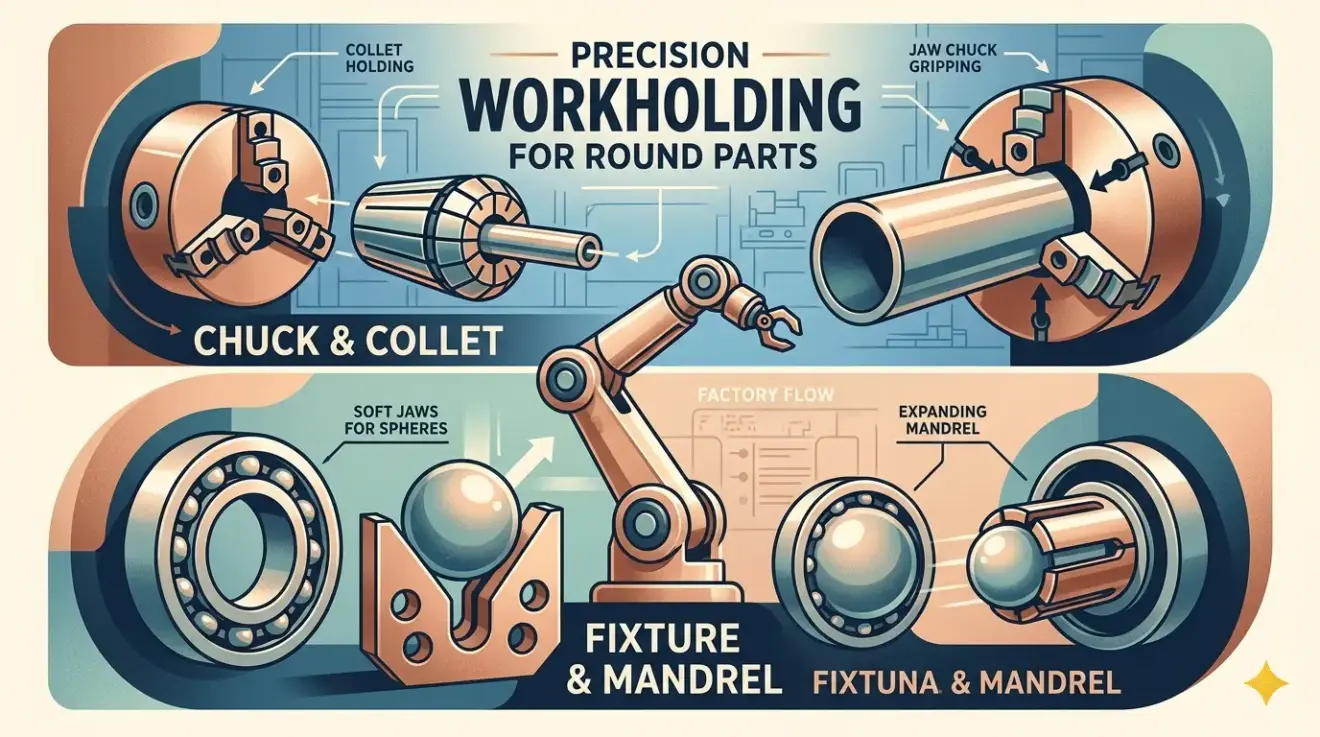
What Is Workholding for Round Parts?
Thursday, 23 April 2026
When a shaft shows runout, a thin sleeve comes out of round, or a second operation refuses to repeat, the machine and program are often healthy—the real culprit is the grip. This article addresses the production problem of preserving cylindrical truth under clamping and cutting loads, explaining why workholding decisions for round parts must be
- Published in Blog
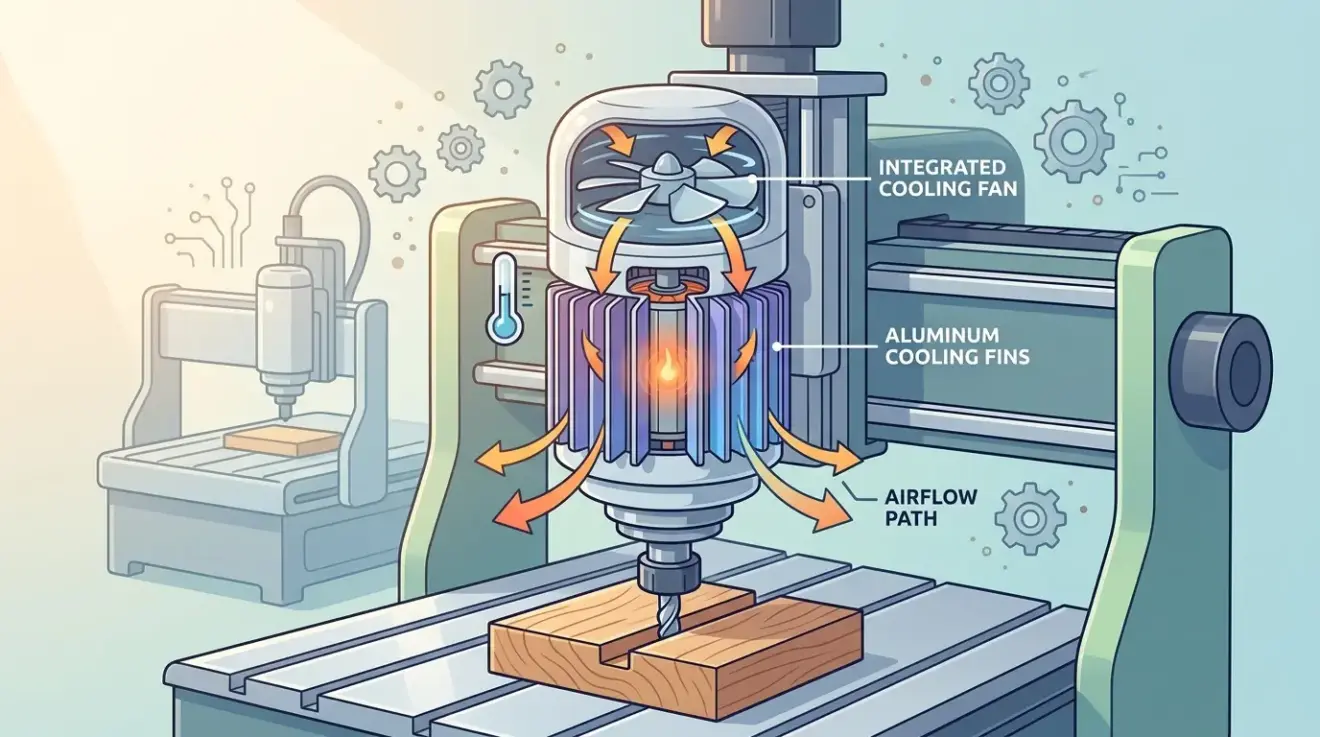
What Is an Air-Cooled CNC Spindle?
Thursday, 23 April 2026
Spindle cooling rarely gets the scrutiny it deserves until a long production run exposes the thermal consequences. Buyers compare power, speed, and collet systems first, then discover that an air-cooled spindle rejects heat into the machine enclosure and surrounding shop air rather than into a controlled liquid loop. That distinction becomes a real production constraint
- Published in Blog
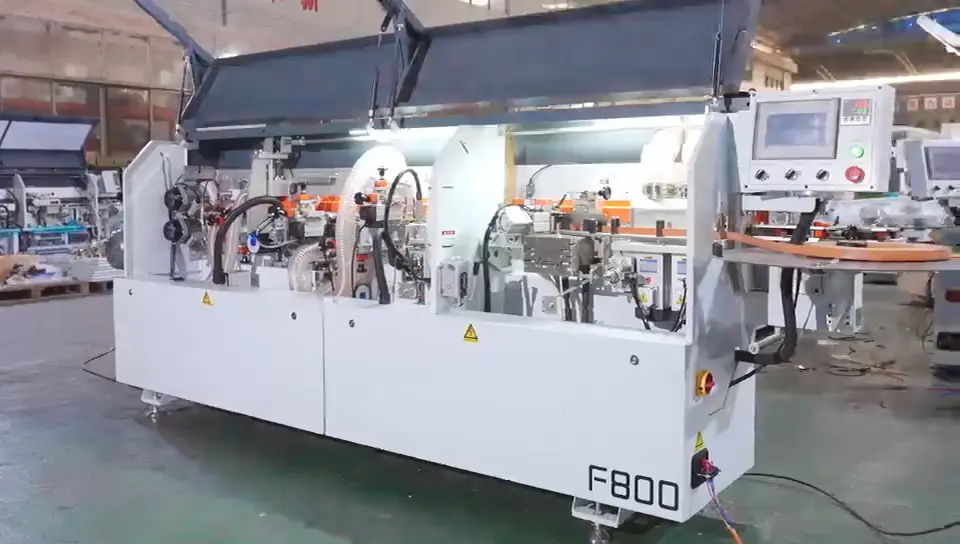
Edgebanders for Straight Panels vs. Shaped Panels: Choosing the Right Workflow
Thursday, 23 April 2026
Edgebander selection fails when buyers compare feed speeds and magazine capacities before classifying their actual part geometry. A shop running thousands of repeated rectangular panels needs stable, repeatable glue lines and consistent trimming, while a factory processing curved or radiused components faces a guidance and finishing problem that straight-line automation cannot solve. Forcing shaped parts
- Published in Blog
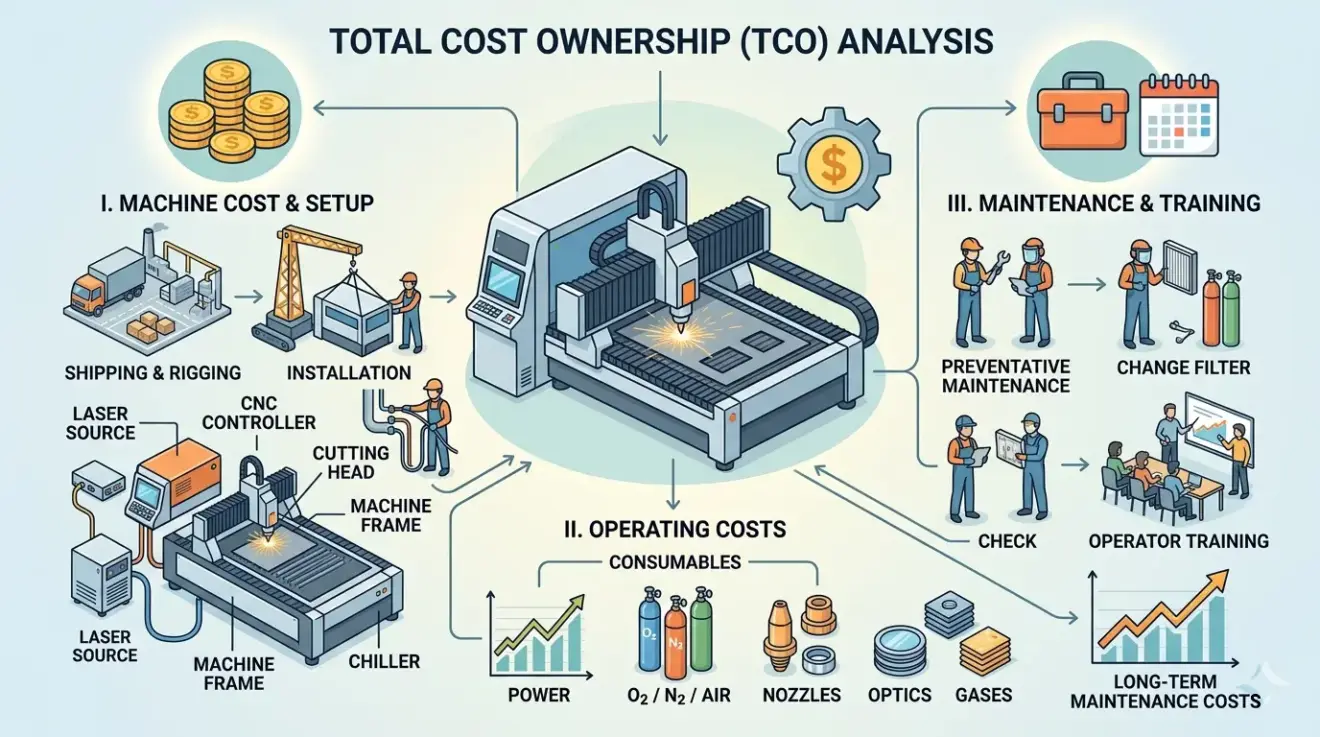
Industrial Laser Cutter Cost Breakdown: Machine, Installation, and Maintenance
Thursday, 23 April 2026
Comparing laser cutter quotes by sticker price alone hides the real investment: two machines with identical spec sheets can differ by tens of thousands of dollars once extraction, cooling, electrical upgrades, commissioning, and preventive maintenance are priced in. This breakdown separates total cost into three distinct buckets—machine package, installation and startup, and maintenance and uptime—so
- Published in Blog
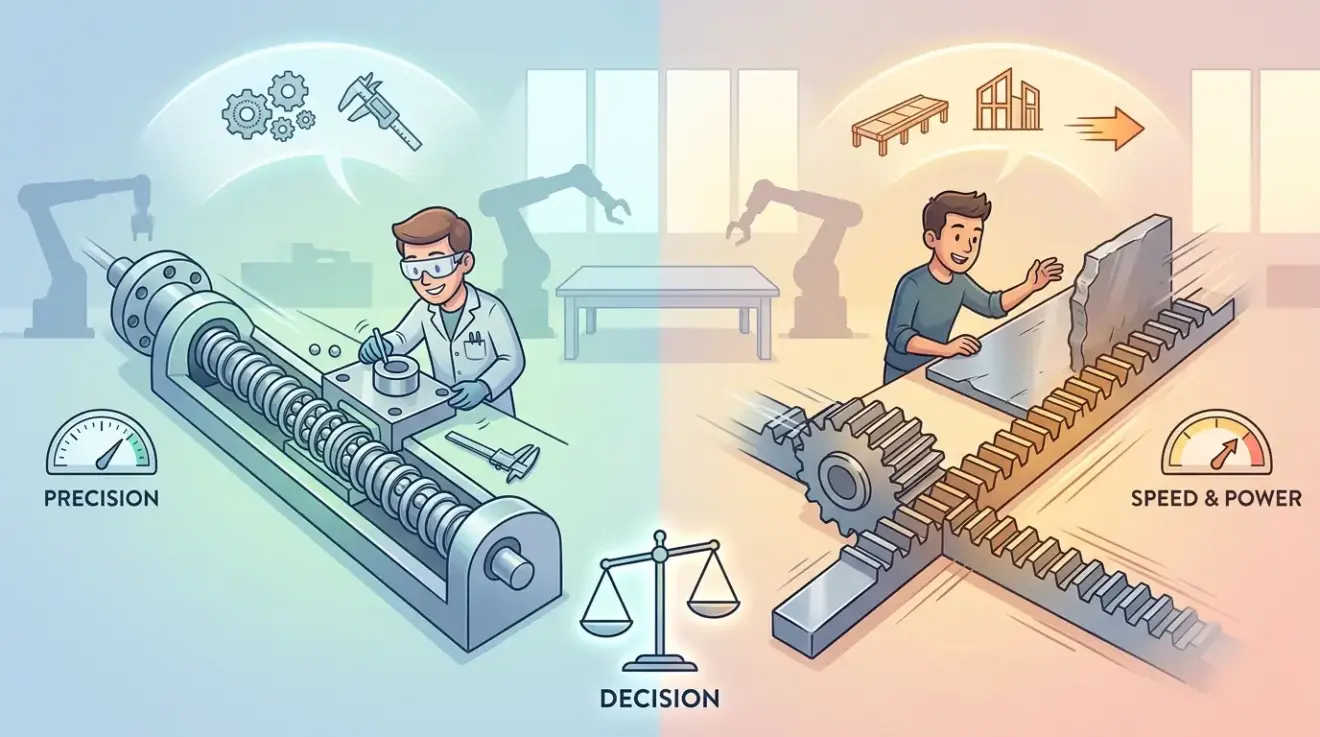
CNC Ball Screw vs Rack and Pinion: Which Drive System Fits Your Machine?
Thursday, 23 April 2026
Before you sign off on a router or machining-center quote, the drive system listed on the spec sheet is not a neutral detail—it is a direct statement about the machine’s intended axis span, moving mass, and daily duty cycle. This article cuts through the forum noise to help you match ball screw or rack and
- Published in Blog
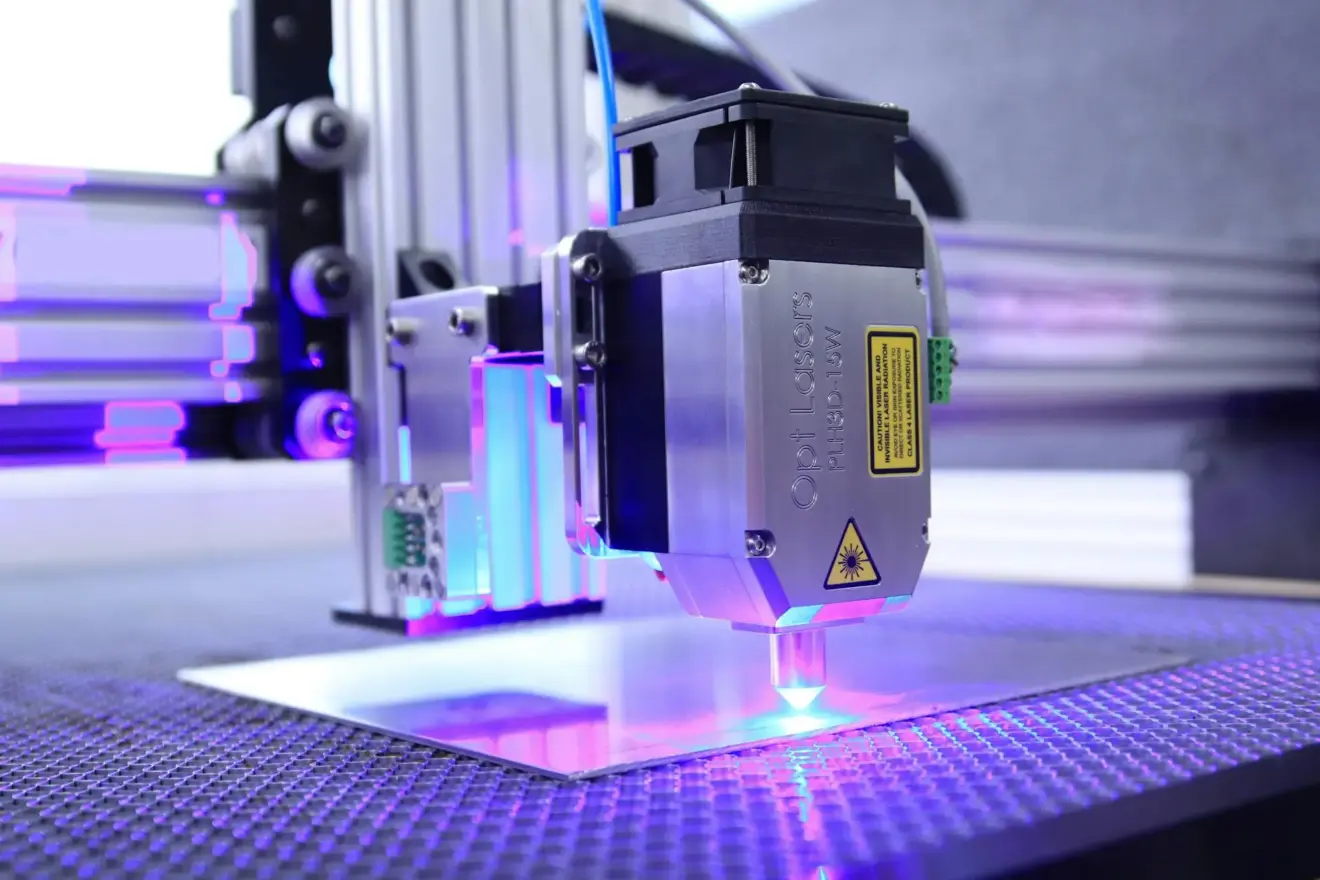
Glass Engraving Machines: Best Use Cases, Process Limits, and Material Tips
Thursday, 23 April 2026
Adding glass engraving to a shop floor usually fails not at the laser source but at the material interface: glass looks forgiving yet punishes assumptions about support, recipe stability, and finish variation. This article addresses the real production problem of treating glass like wood or acrylic, which generates scrap, rework, and quoting errors before the
- Published in Blog
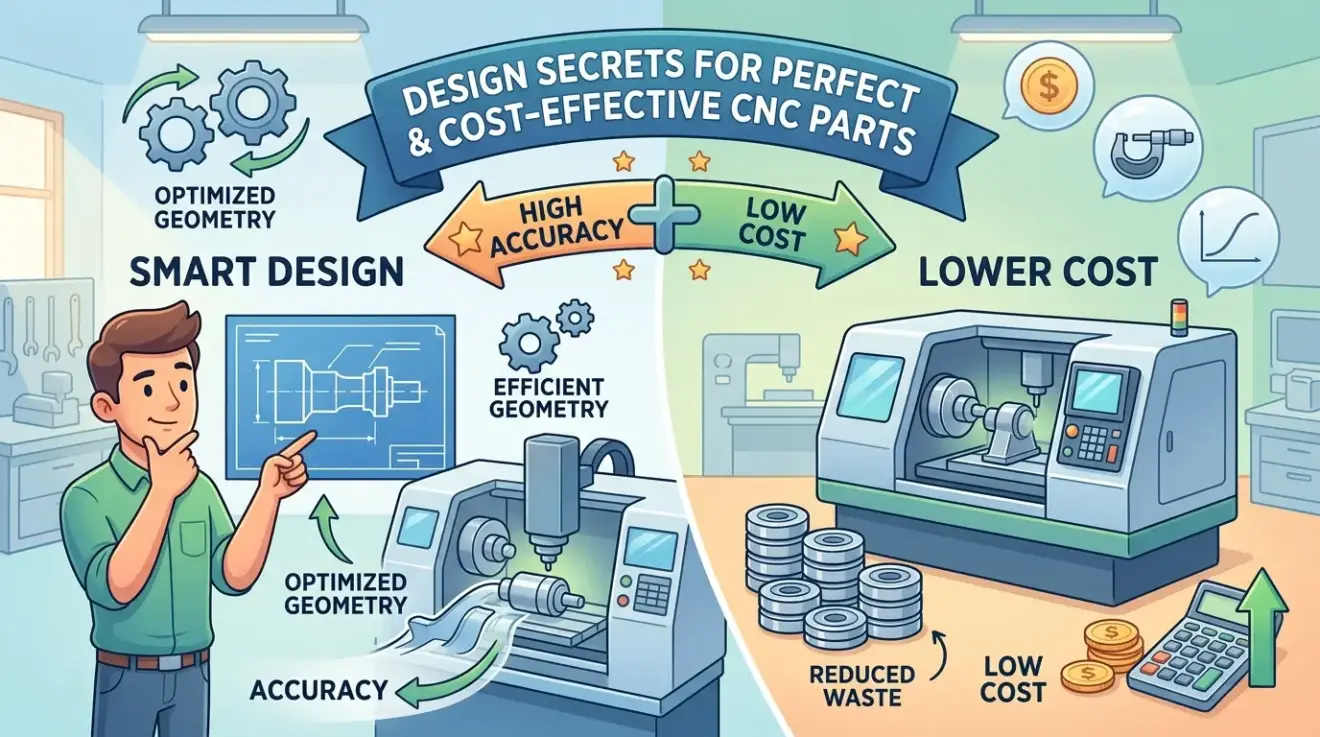
CNC Turned Parts: Design Tips for Better Accuracy and Lower Cost
Thursday, 23 April 2026
Before a turned-part drawing reaches the shop floor, its geometry has already decided whether the route will be stable or fragile. This article confronts the real cost drivers that hide inside seemingly simple prints: weak rigidity in slender sections, tight tolerances applied without functional justification, tool access blocked by shoulders and grooves, and secondary operations
- Published in Blog
CNC Milling Services: What to Check Before You Outsource Precision Parts
Thursday, 23 April 2026
Outsourcing precision CNC milling fails less often at the spindle and more frequently in the unspoken assumptions buried between drawing release and shipment acceptance. This article gives procurement teams and production engineers a practical pre-award checklist built around the real risks: undefined deliverable conditions, unnamed failure modes, vague setup logic, and quotes that hide managed
- Published in Blog