

 Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
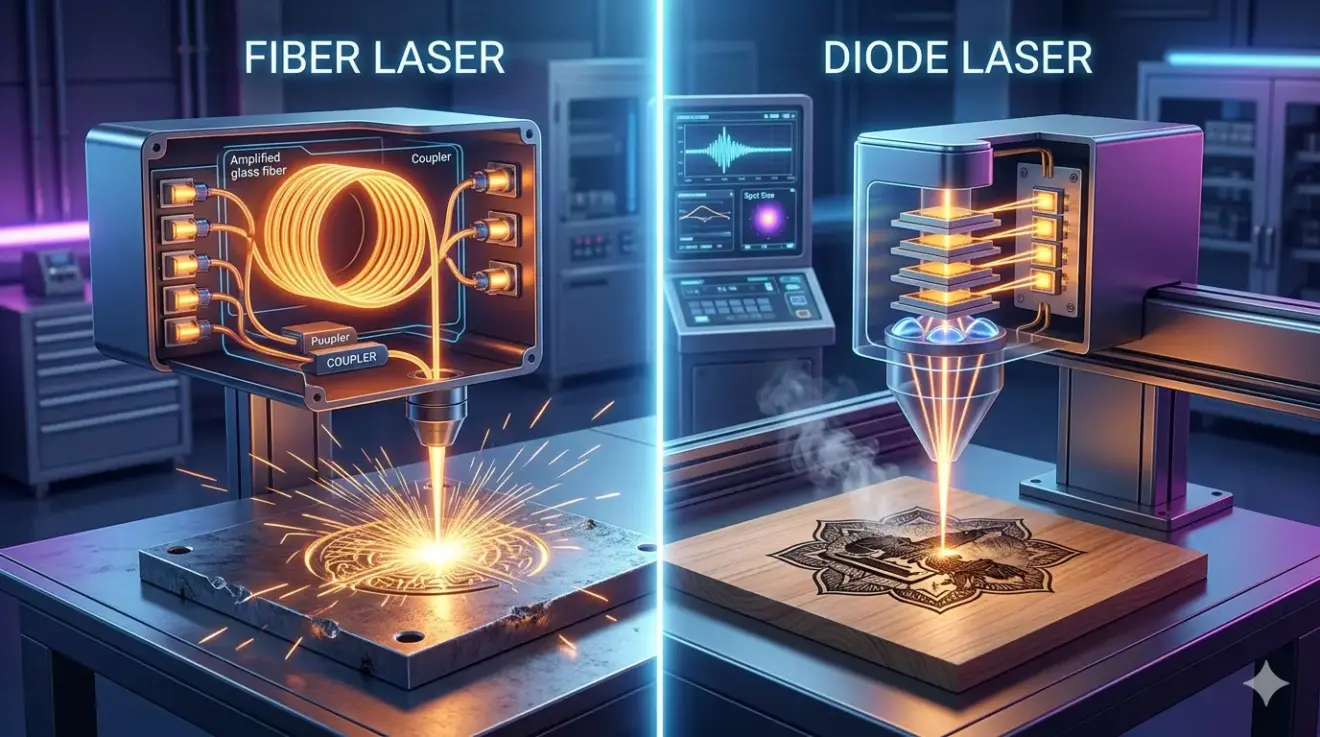
Fiber Laser vs Diode Laser: Which One Fits Your Engraving or Cutting Workflow?
Thursday, 23 April 2026
The production question comes before comparing wattage or price quotes, define the material family and duty cycle your shop actually runs. Fiber and diode lasers are not different power levels of the same tool; they serve distinct workflows, and misclassifying them leads to expensive bottlenecks. Fiber suits metal-first production, whether for permanent part marking or
- Published in Blog
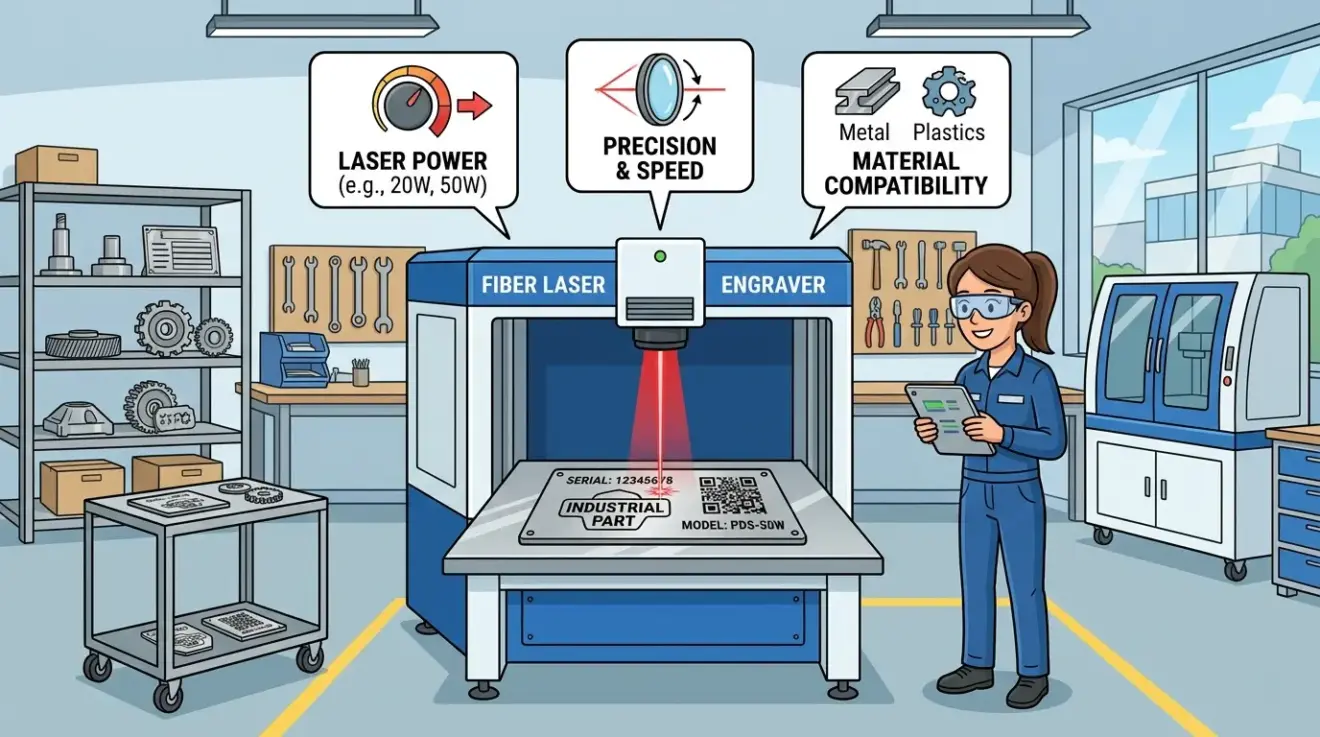
How To Choose a Fiber Laser Engraving Machine for Industrial Marking Applications
Thursday, 23 April 2026
Industrial marking decisions fail when buyers evaluate a sample mark instead of the production workflow that surrounds it. Serial numbers, data matrix codes, and part IDs must survive handling, coating, and downstream verification, yet many factories discover too late that a visually acceptable mark fails scanner checks or disappears during shot blasting. This article walks
- Published in Blog
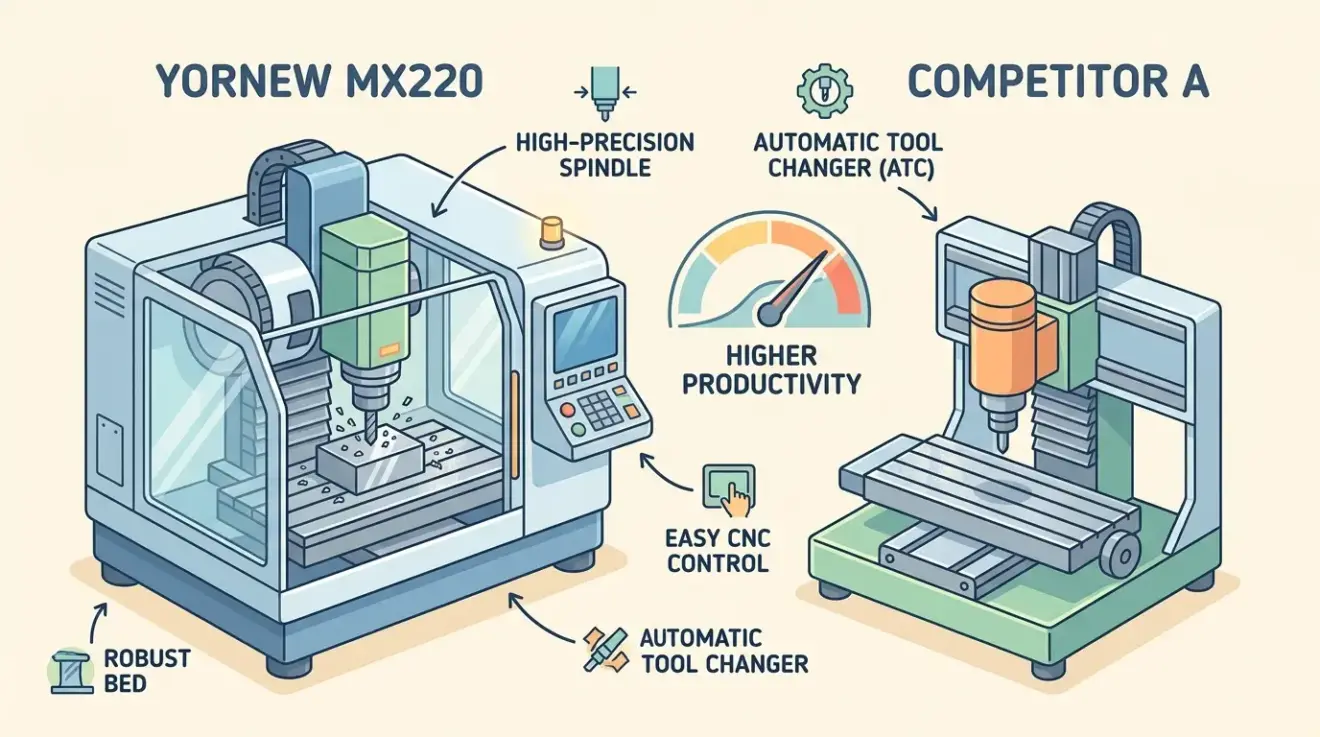
Yornew CNC Price Guide: MX220 and Other Small Mill Models Compared
Thursday, 23 April 2026
When buyers search for Yornew CNC pricing, particularly around MX220-style compact mills, they are usually not looking for a perfect market analysis. They want a clean number that says the machine is affordable, the risk is manageable, and the project can begin without a lengthy capital-equipment debate. The problem is that small-mill pricing rarely behaves
- Published in Blog
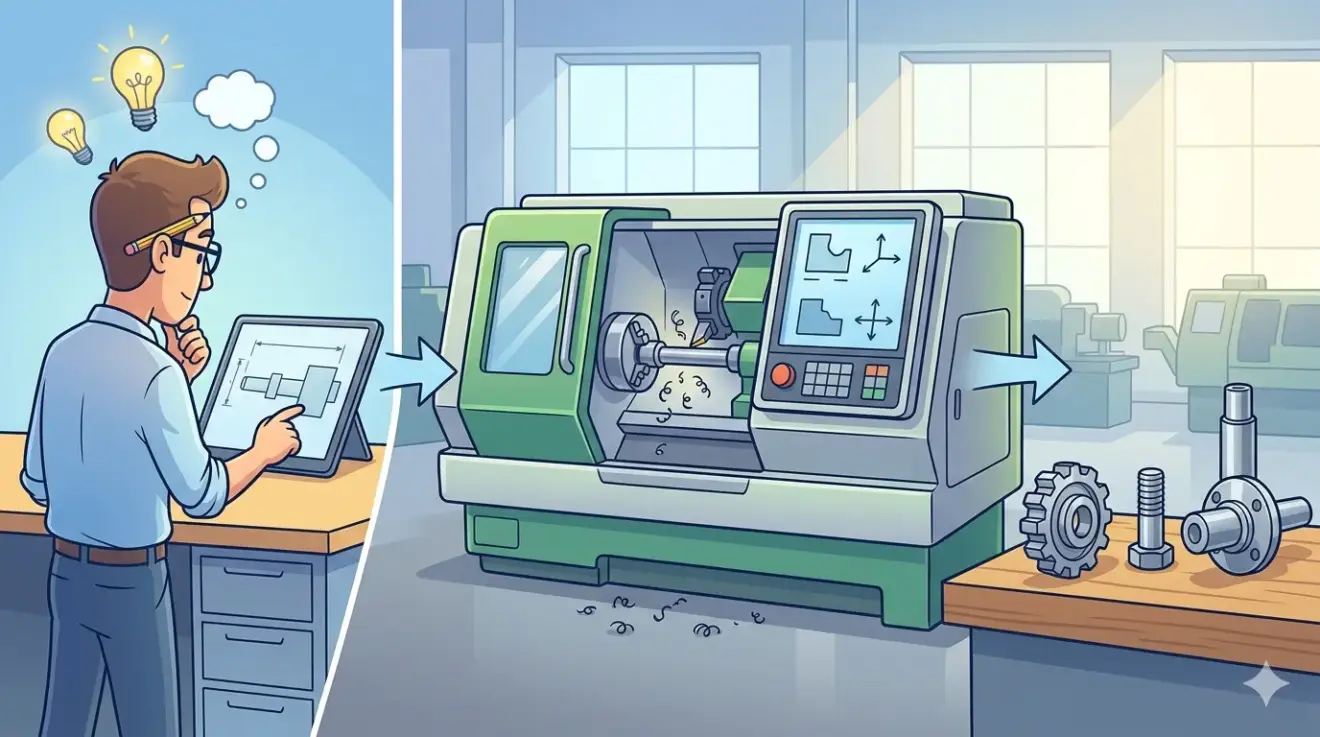
CNC Lathe Machine Buying Guide for Metal Part Production
Thursday, 23 April 2026
Most CNC lathe purchases fail not because the spindle is undersized, but because the shop never proved the recurring workload before comparing quotes. This guide forces buyers to reverse the typical process: disqualify the purchase case early, write a one-page workload brief, and map stock form, batch pattern, and tolerance burden together before any supplier
- Published in Blog
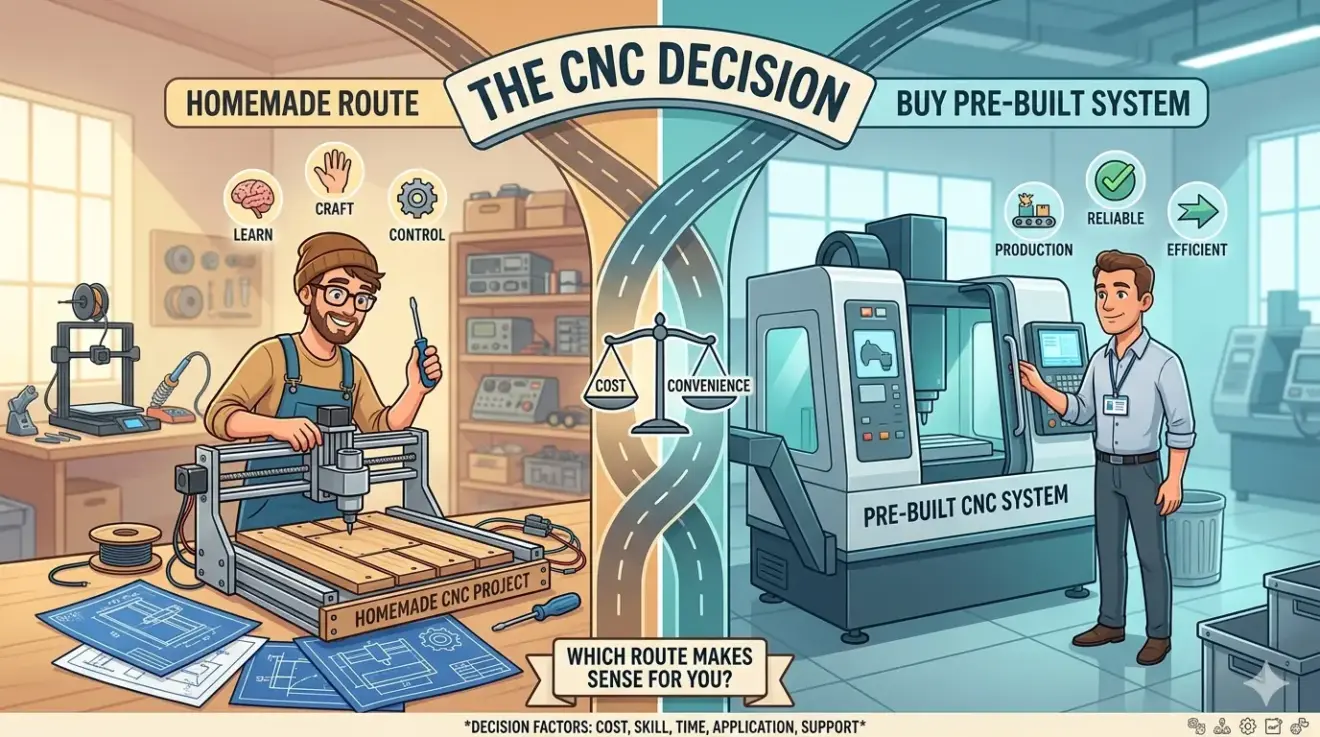
Homemade CNC Machines vs Buy-Built Systems: Which Route Makes Sense?
Thursday, 23 April 2026
Cabinet shops and small fabrication facilities keep circling the same fork in the road: assemble a CNC router from extruded aluminum and stepper motors, or sign for a turnkey system that cuts saleable parts within two weeks. The decision gets distorted when buyers compare component costs instead of time to stable output. A homemade build
- Published in Blog
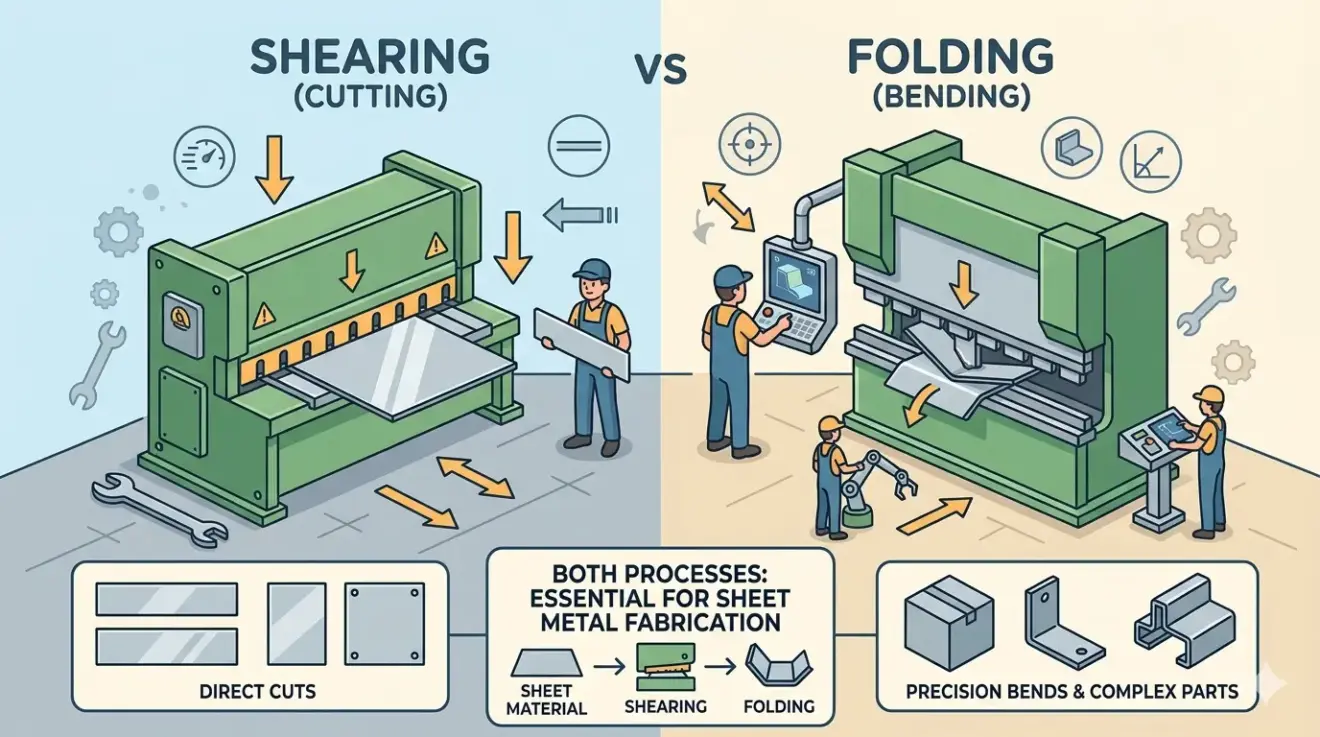
CNC Shearing Machine vs CNC Folding Machine: Which Sheet Metal Process Do You Need?
Thursday, 23 April 2026
Before comparing machine specs, trace a single part from raw sheet to finished component and locate where the friction actually starts. Shearing and folding are sequential tools, not substitutes: one disciplines blank preparation upstream, the other controls formed geometry downstream. The real buying decision is not which machine is more advanced, but which missing capability
- Published in Blog
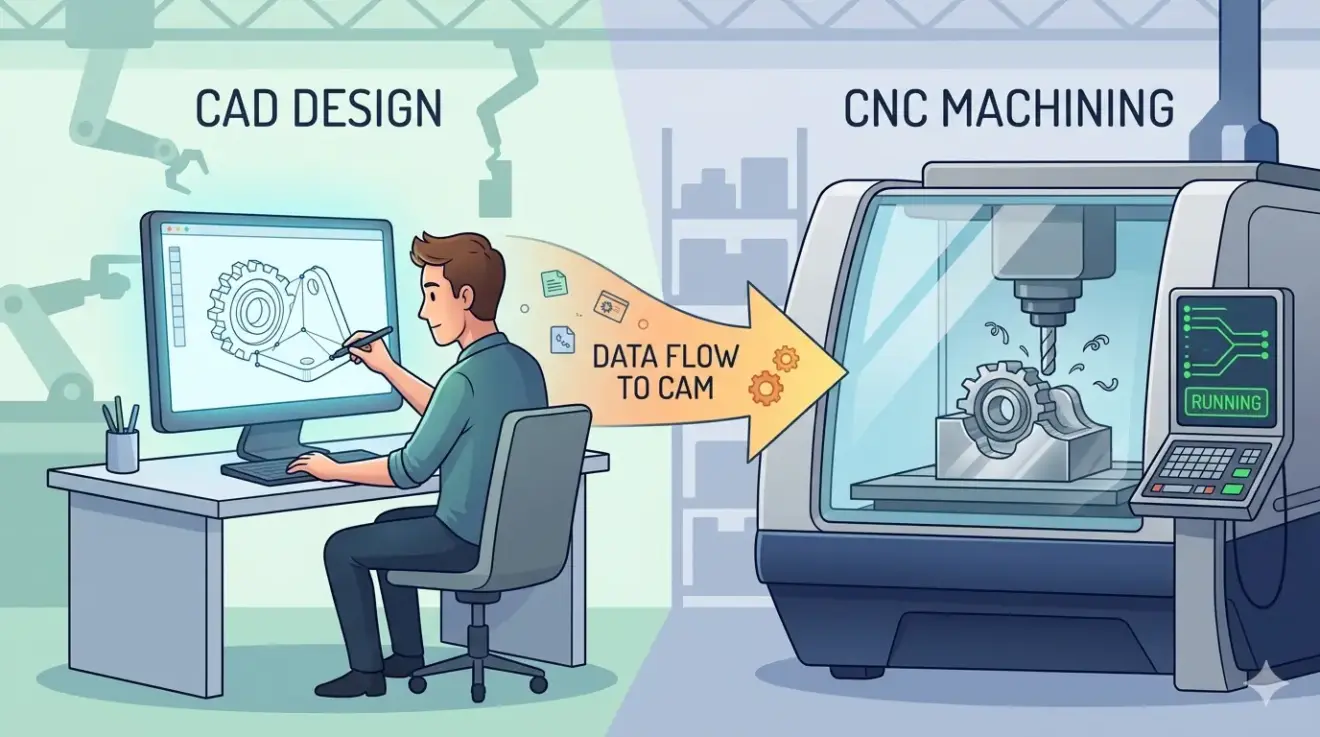
AutoCAD for CNC Workflows: Where It Fits and Where CAM Starts
Wednesday, 22 April 2026
Engineering releases a DWG marked “finished,” programming opens it and sees geometry that still cannot run. Both are right, and that gap is where production time disappears. This article draws the practical line between AutoCAD and CAM: drafting settles approved shape, revision clarity, and human-readable layout, while CAM decides tool order, lead-ins, stock logic, hold-down
- Published in Blog
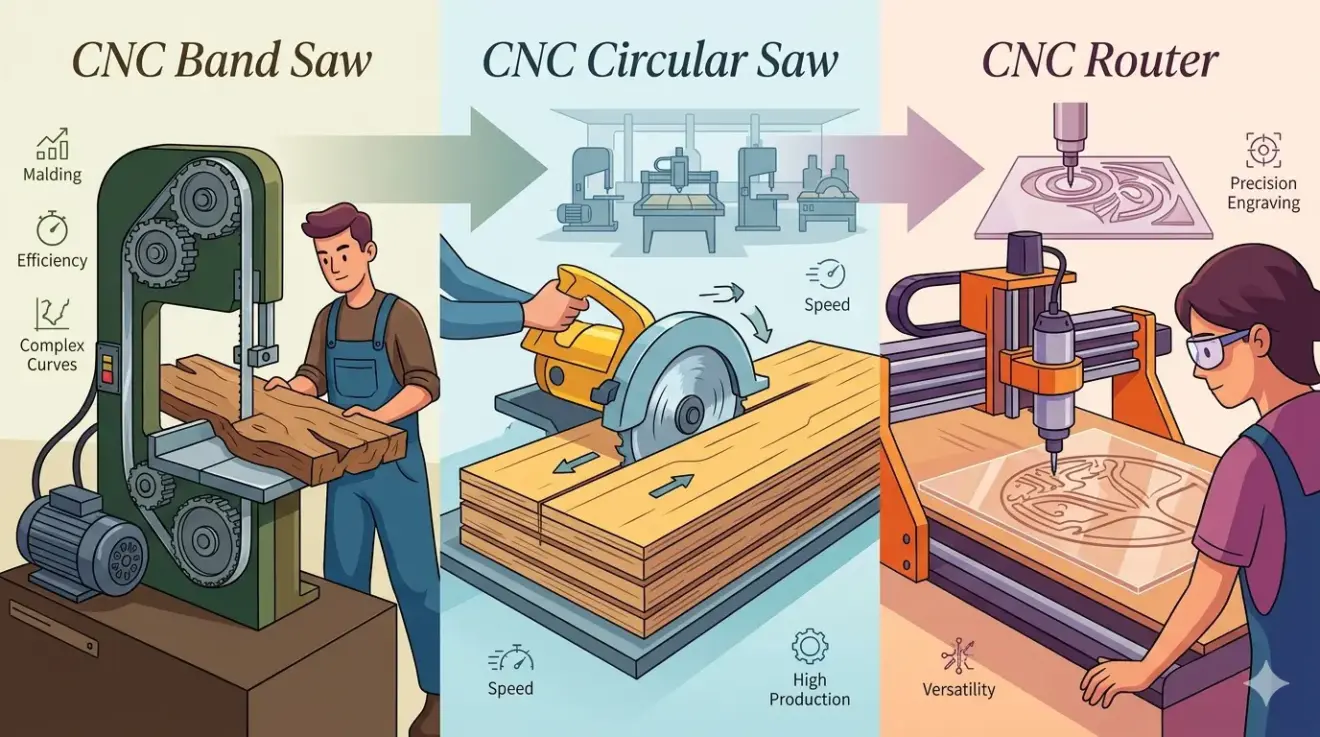
CNC Saw vs Band Saw vs Router: Which Cutting System Fits Your Workflow?
Wednesday, 22 April 2026
Define the workload before judging spindle power or feed rates, classify a month of your shipped parts into straight blanks, rough curved blanks, and feature-rich components that need holes, pockets, or cutouts. That sorting exposes which cutting logic—saw, band saw, or router—actually removes the most labor from your line. The real decision is not which
- Published in Blog
Acrylic Laser Cutter for Sign Making and Display Fabrication: What Matters Most in Production
Wednesday, 22 April 2026
Sign shops and display fabricators often approve a laser cutter around one polished demo part, then discover that the real weekly mix—illuminated faces, clear risers, branded inserts, short-run revisions—stresses the machine in ways the sample never revealed. The decision hinges on whether the system holds visible edge quality, dimensional repeatability, engraving clarity, and fast changeovers
- Published in Blog
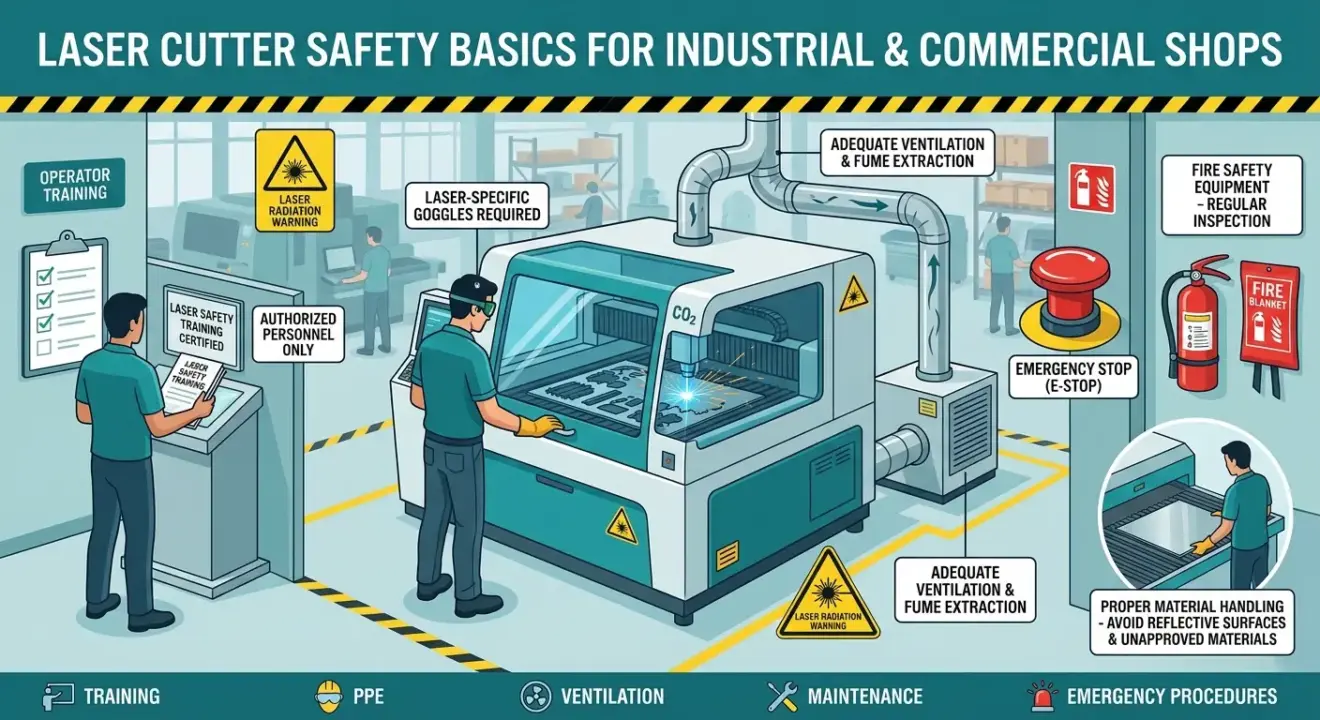
Laser Cutter Safety Basics for Industrial and Commercial Shops
Wednesday, 22 April 2026
Laser safety failures in production rarely begin with the beam itself; they start when an unverified substrate reaches the bed, extraction airflow drops unnoticed, or an operator walks away from a routine-looking job. Treating safety as a compliance checklist instead of a process-control discipline compounds risk alongside scrap, rework, and unplanned downtime. This article addresses
- Published in Blog
What Is Double Column Milling?
Wednesday, 22 April 2026
When a part family outgrows a standard vertical machining center, the first symptom is rarely a hard travel limit—it is a creeping loss of confidence across wide spans: finish drift, setup improvisation, and structural flex that smaller jobs never exposed. That is the point where double column milling stops being a catalog category and becomes
- Published in Blog
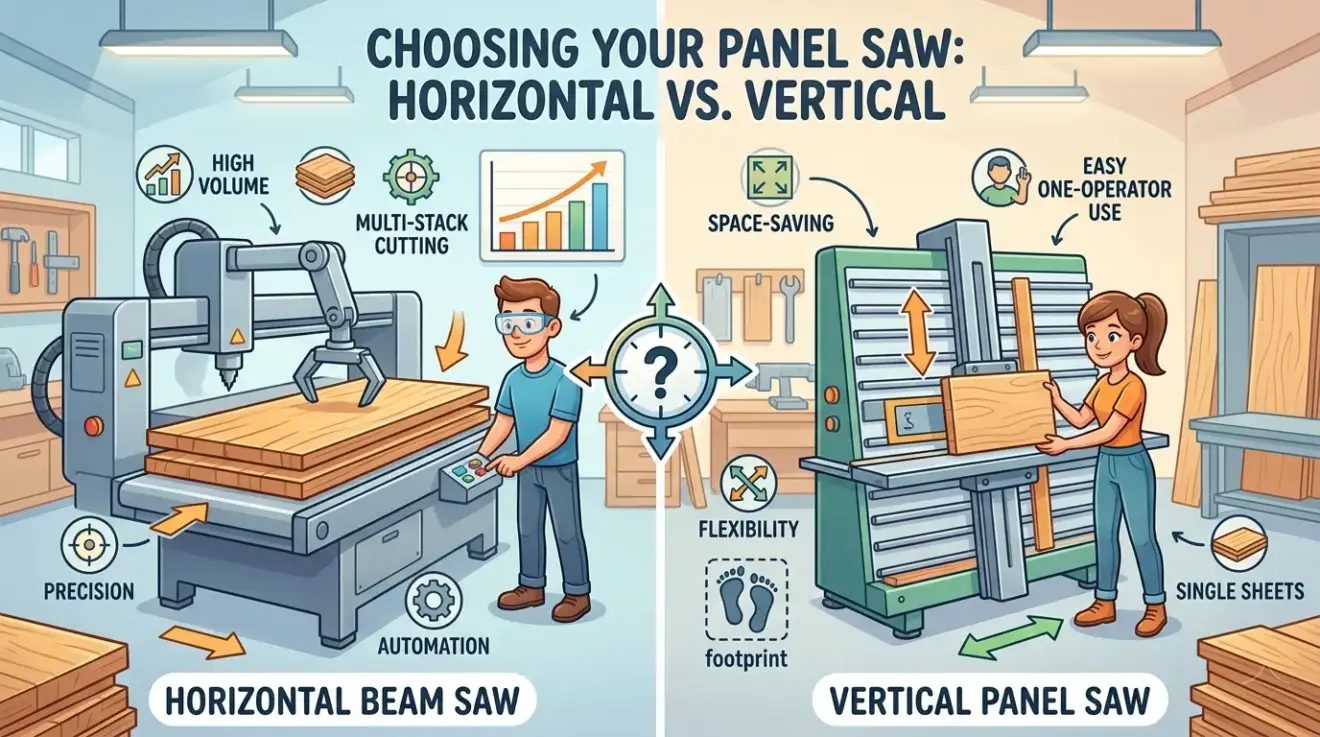
Horizontal Beam Saw vs. Vertical Panel Saw: Which One Fits Better?
Wednesday, 22 April 2026
Before comparing feed speeds or blade specifications, identify the actual production constraint that is slowing your line. This article addresses the real decision between a horizontal beam saw and a vertical panel saw: not which cuts straighter, but which removes the dominant friction from your workflow. For cabinet and furniture manufacturers, the choice determines whether
- Published in Blog
CNC Drilling Machines In Panel Furniture Manufacturing: Where They Fit Best
Wednesday, 22 April 2026
Drilling in panel furniture production is rarely the dramatic failure pointâit is the quiet accumulation of shifted hole rows, rechecked connector positions, and hinges that take longer to seat than they should. These small variations spread into slower assembly, mismatched cabinet parts, and rework on dowel or shelf-support locations. This article addresses the real selection
- Published in Blog
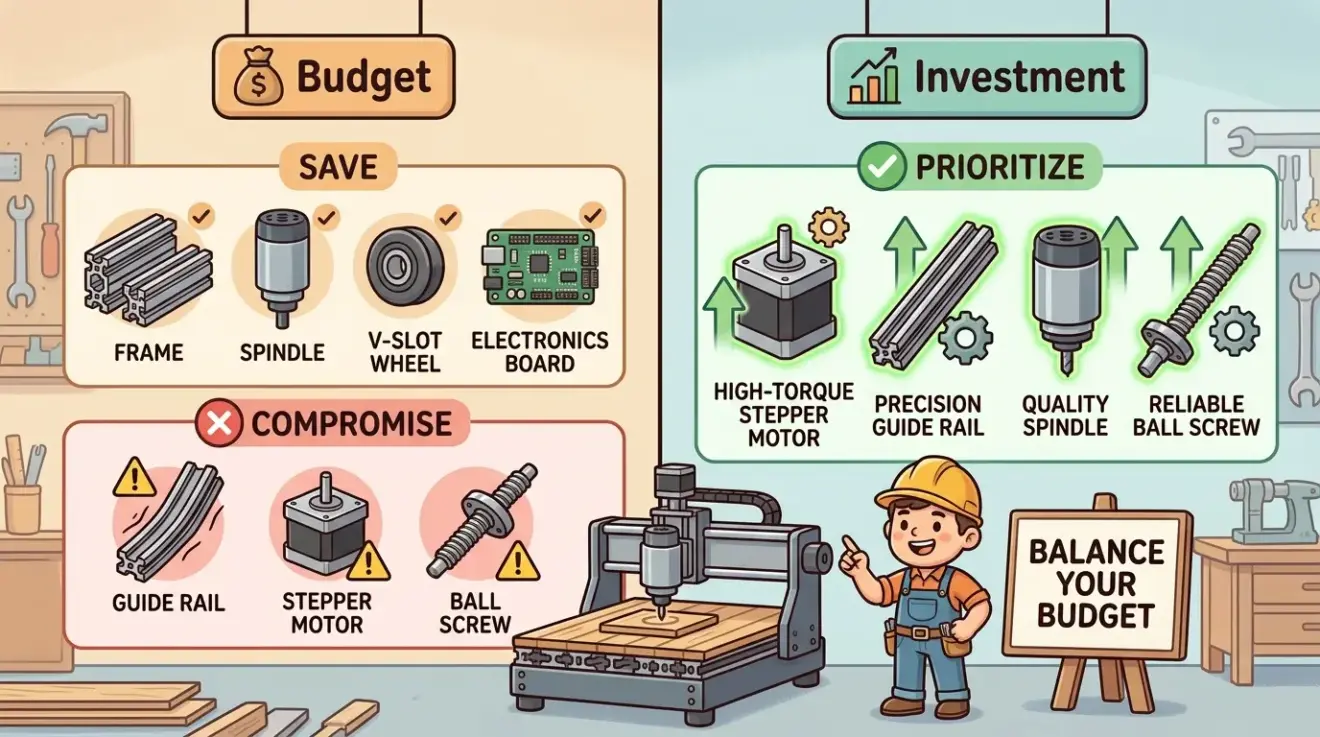
Budget CNC Machine Guide: Where to Save and Where Not to Compromise
Wednesday, 22 April 2026
Budget CNC procurement fails when buyers start with a price ceiling and work backward, turning the decision into specification shopping before defining what underperformance would actually cost the shop. A bad week on a customer-facing machine—delayed delivery, lost margin, operator distrust—is expensive even if the equipment technically runs. This guide forces a practical triage: sort
- Published in Blog
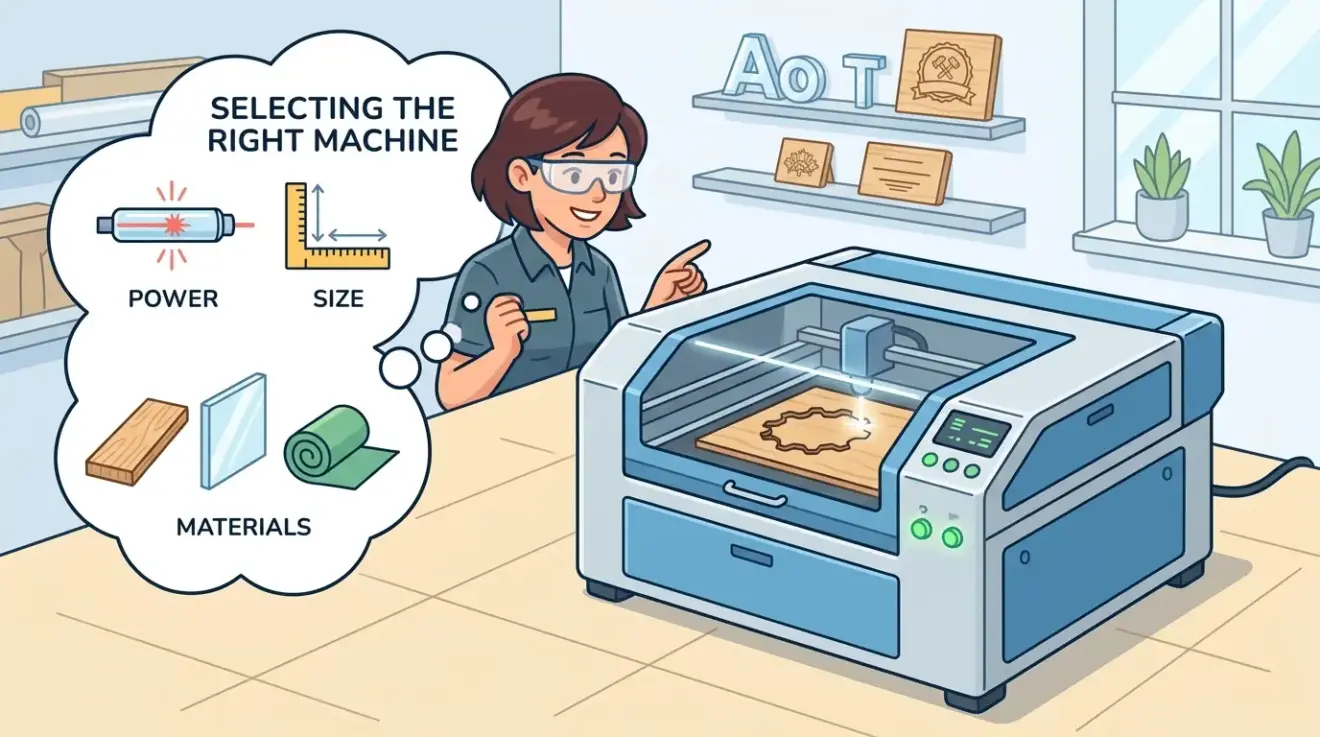
How To Choose the Right CO2 Laser Machine for Non-Metal Processing
Wednesday, 22 April 2026
Selecting a CO2 laser for non-metal work fails when the decision rests on a polished demo sample instead of the weekly production queue. Acrylic display parts, engraved wood panels, and plywood components each impose different demands on focus stability, extraction capacity, air assist, and motion control, so a machine that excels on one material often
- Published in Blog
How to Match Edge Banding Equipment to Different Panel Materials
Wednesday, 22 April 2026
Edge banding defects in cabinet and furniture plants usually surface as rework at the glue line, chipped corners at trimming, or a visible mismatch between the edgeband and board face that only appears after assembly. Operators adjust glue temperature or swap tape rolls, yet the defect rate drifts back because the root cause is a
- Published in Blog
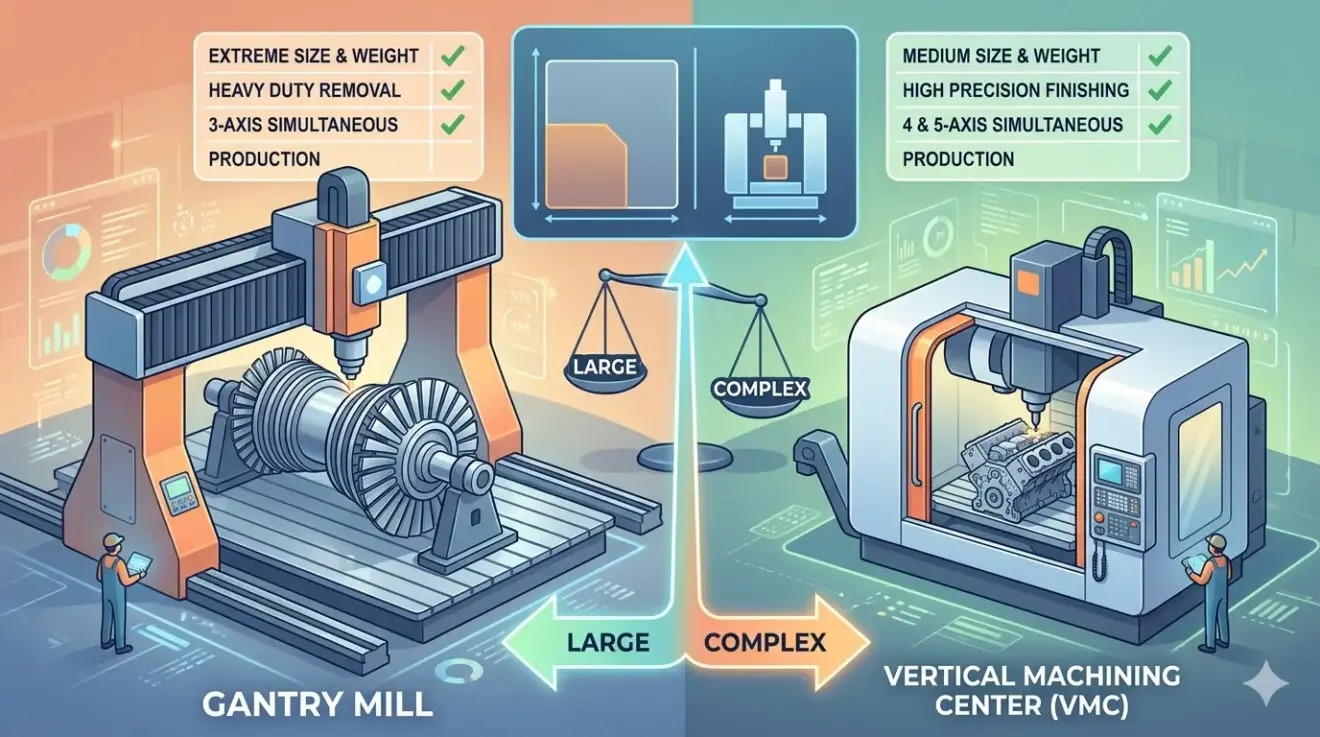
Gantry Mill vs Vertical Machining Center: Which One Fits Large-Part Production?
Wednesday, 22 April 2026
Large-part machining decisions rarely hinge on spindle specs alone; once a workpiece becomes heavy, wide, or awkward to reposition, the real burden shifts to loading, crane time, setup labor, and access. This article compares gantry mills against vertical machining centers by examining how each architecture meets the part, not just its axis travel. The critical
- Published in Blog
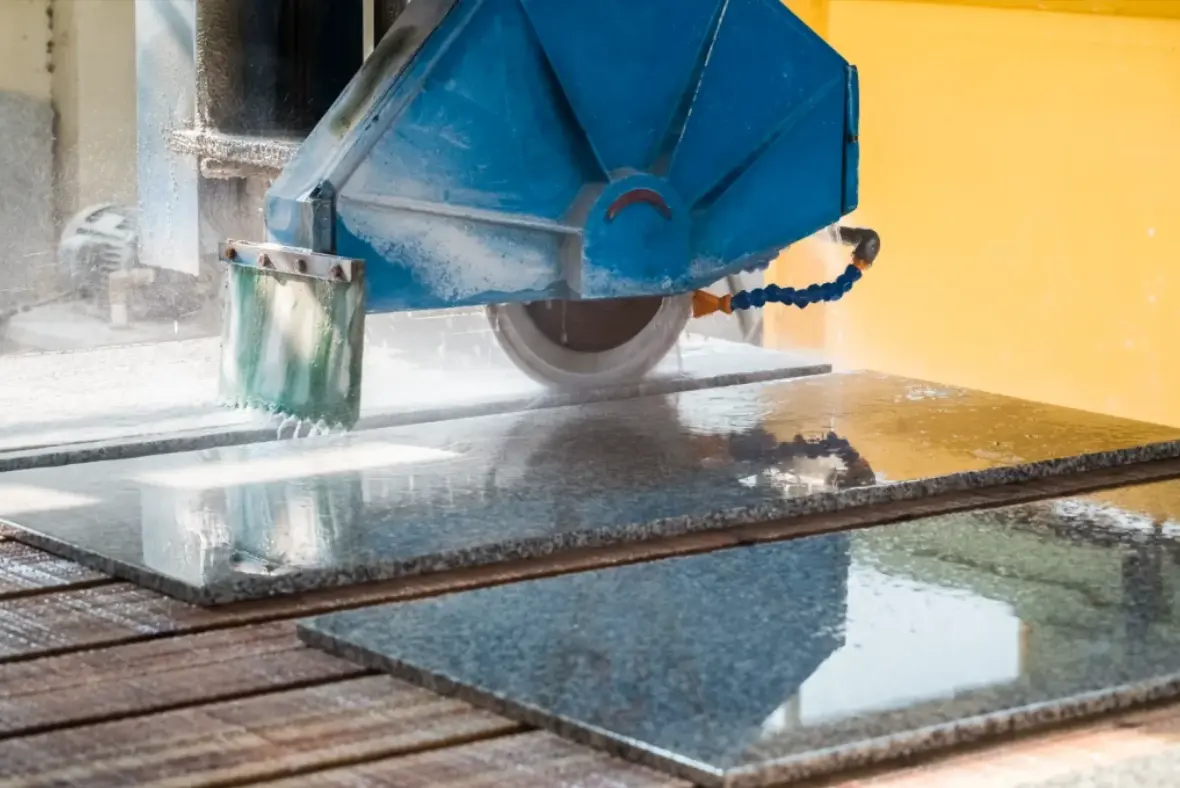
How to Choose a Stone CNC Machine for Custom Fabrication
Wednesday, 22 April 2026
Before comparing spindle power or axis counts, custom stone shops must first identify the production bottleneck that a CNC purchase is meant to solve. Inconsistent sink cutouts, excessive hand correction on edges, slow changeovers between quartz, marble, and granite jobs, and rework that surfaces only during polishing or installation are the real constraints that justify
- Published in Blog
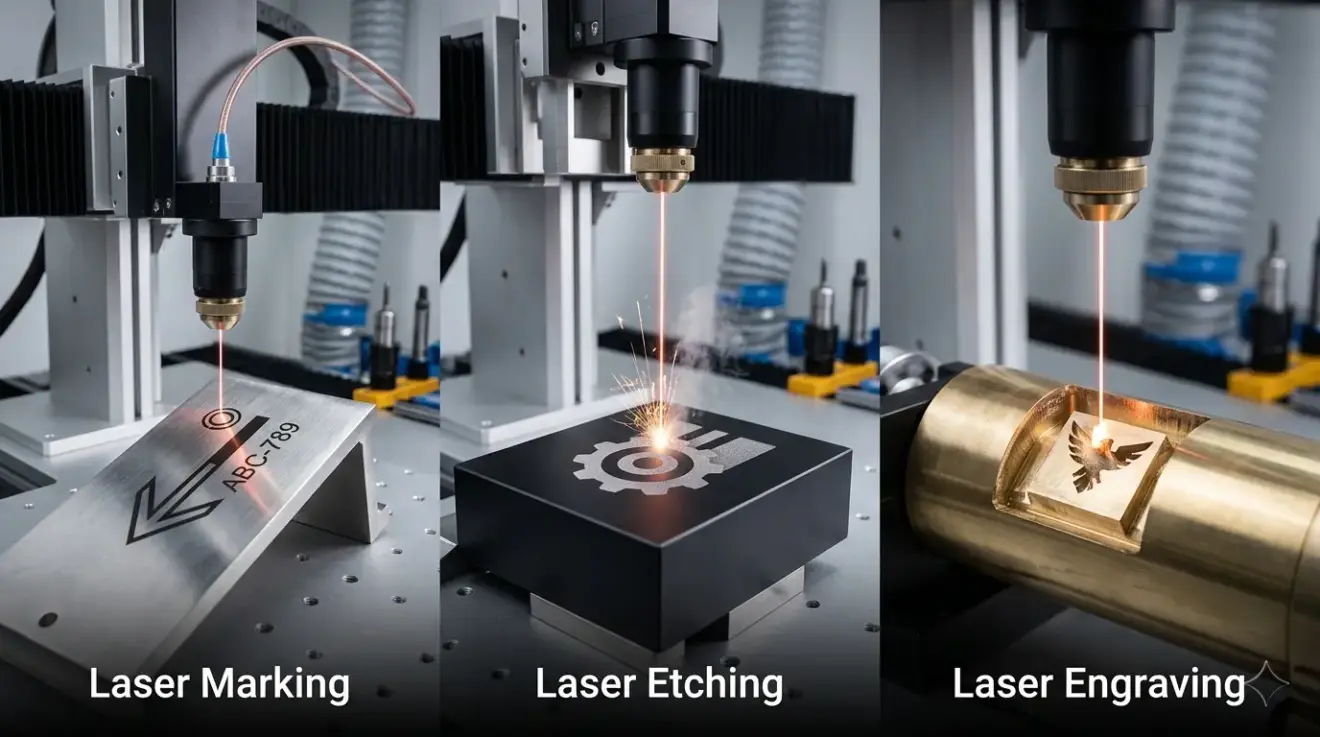
Laser Engraving vs Laser Marking vs Laser Etching: How to Choose the Right Process
Wednesday, 22 April 2026
When a production RFQ asks for “laser marking,” the actual job may demand anything from a deep brand recess in solid oak to a fast QR code on a coated panel—and choosing the wrong physical process means rejected parts, rework, and missed delivery dates. This article separates the three terms by what they do to
- Published in Blog
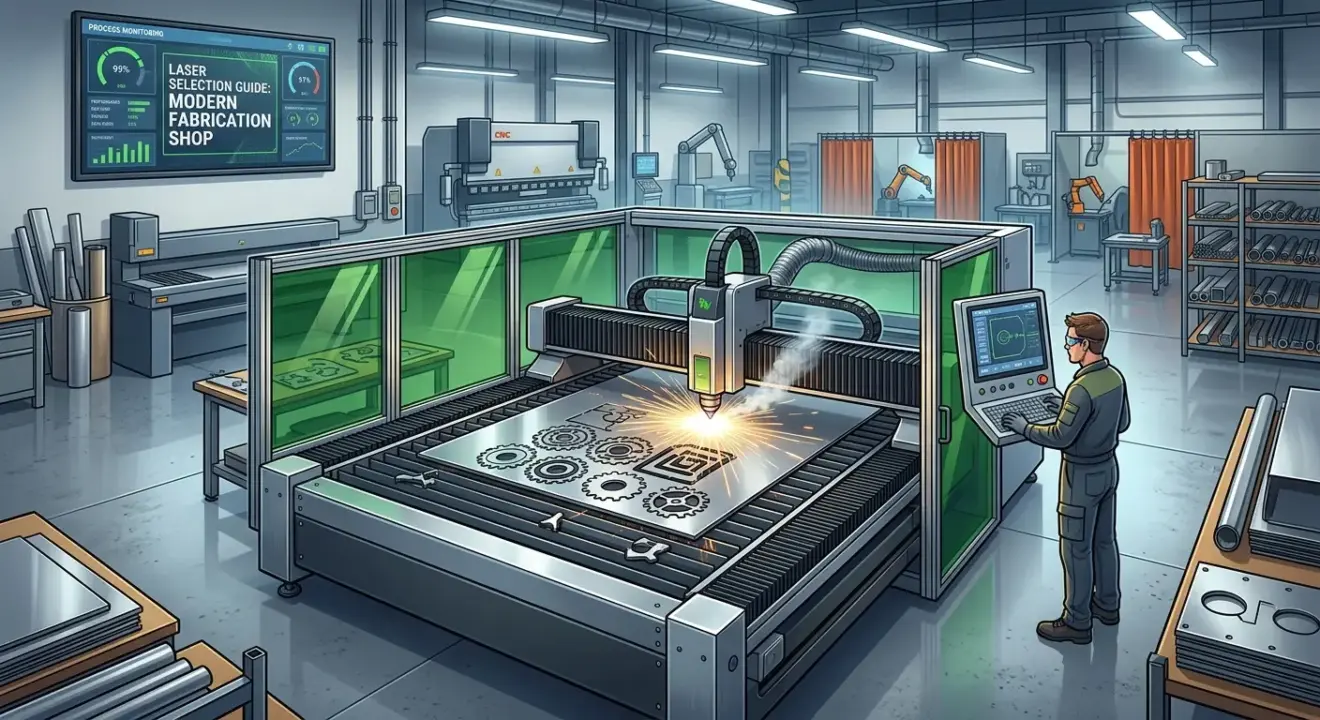
How to Choose the Right Laser Machine for a Modern Fabrication Shop
Wednesday, 22 April 2026
Before comparing wattage ratings or scanning spec sheets, define the production bottleneck your shop actually faces. This article walks fabrication managers through the real selection logic: matching laser type, power, and wavelength to your dominant material mix—acrylic, wood, veneers, or laminates—and separating cutting-heavy from engraving-heavy workflows. It forces honest evaluation of edge quality standards, changeover
- Published in Blog
Chevalier CNC, Kuraki Boring Mill, and Other Industrial Machines: How to Evaluate Specialist Brands
Wednesday, 22 April 2026
When a production manager enters a capital-equipment review already convinced that a Chevalier grinder or a Kuraki boring mill is the answer, the procurement process has already gone sideways. A respected nameplate does not solve a bottleneck; it only becomes relevant after you have proven that your part family demands a specialist machine class, that
- Published in Blog
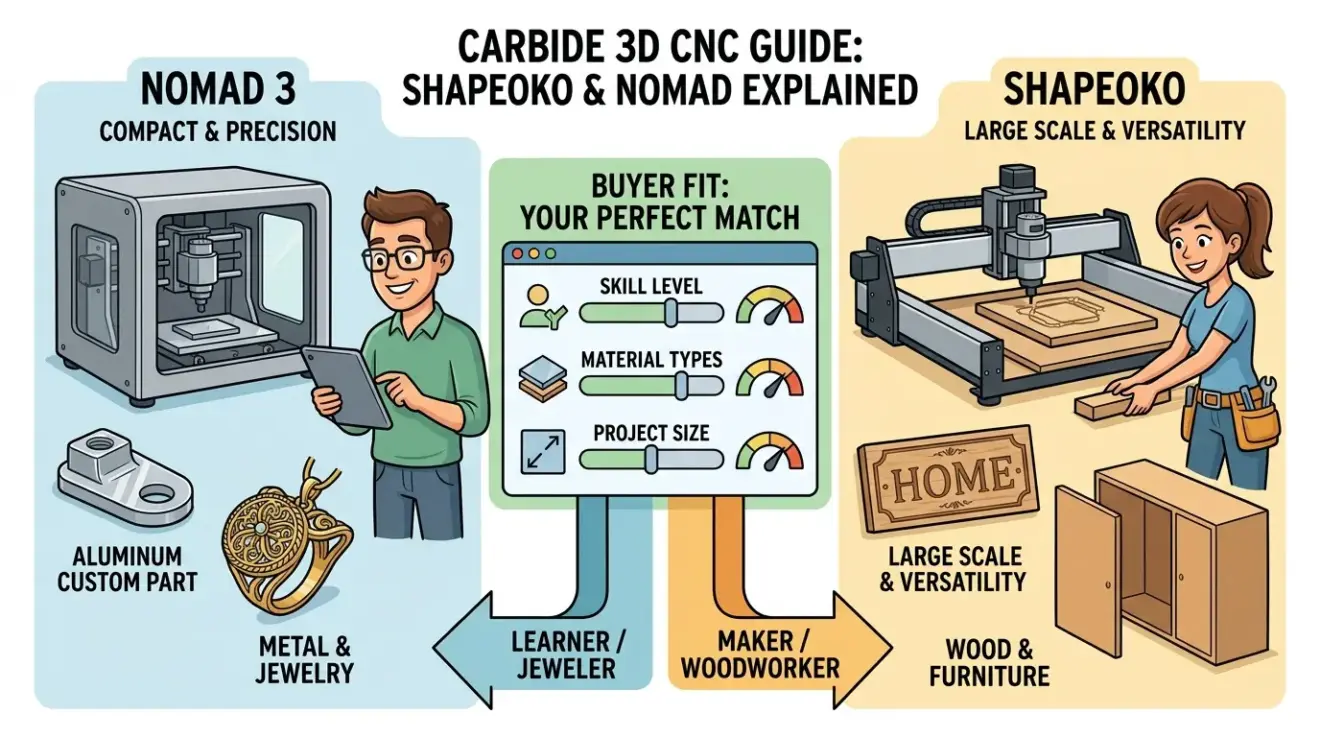
Carbide 3D CNC Machines Explained: Shapeoko, Nomad, and Buyer Fit
Tuesday, 21 April 2026
Buyers often lump Carbide 3D’s Shapeoko and Nomad into one brand decision, yet these machines solve fundamentally different weekly production problems. Shapeoko belongs to router logic—broad flat stock, sign blanks, jigs, and template work where hold-down, dust extraction, and spoilboard strategy dominate operator time. Nomad belongs to contained small-part milling—compact prototypes, engraving, and bench-scale fixtures
- Published in Blog
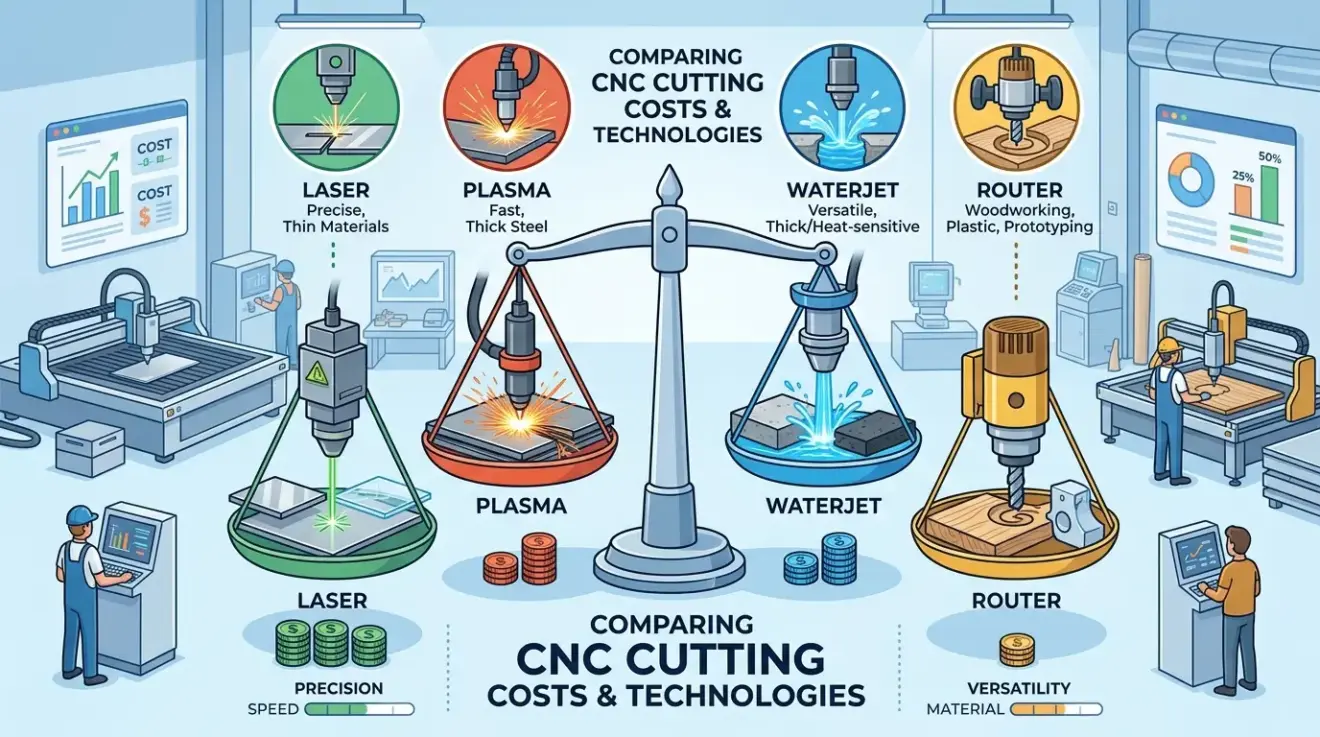
CNC Cutting Machine Price Guide: Comparing Laser, Plasma, Waterjet, and Router Costs
Tuesday, 21 April 2026
Sticker prices mislead because they ignore the infrastructure, consumables, and labor each cutting process demands once it hits the production floor. A router’s tooling and spoilboard burden, a laser’s ventilation and material-fit dependency, a plasma system’s fume handling and edge cleanup, and a waterjet’s abrasive and slurry management all shift the true cost picture dramatically.
- Published in Blog
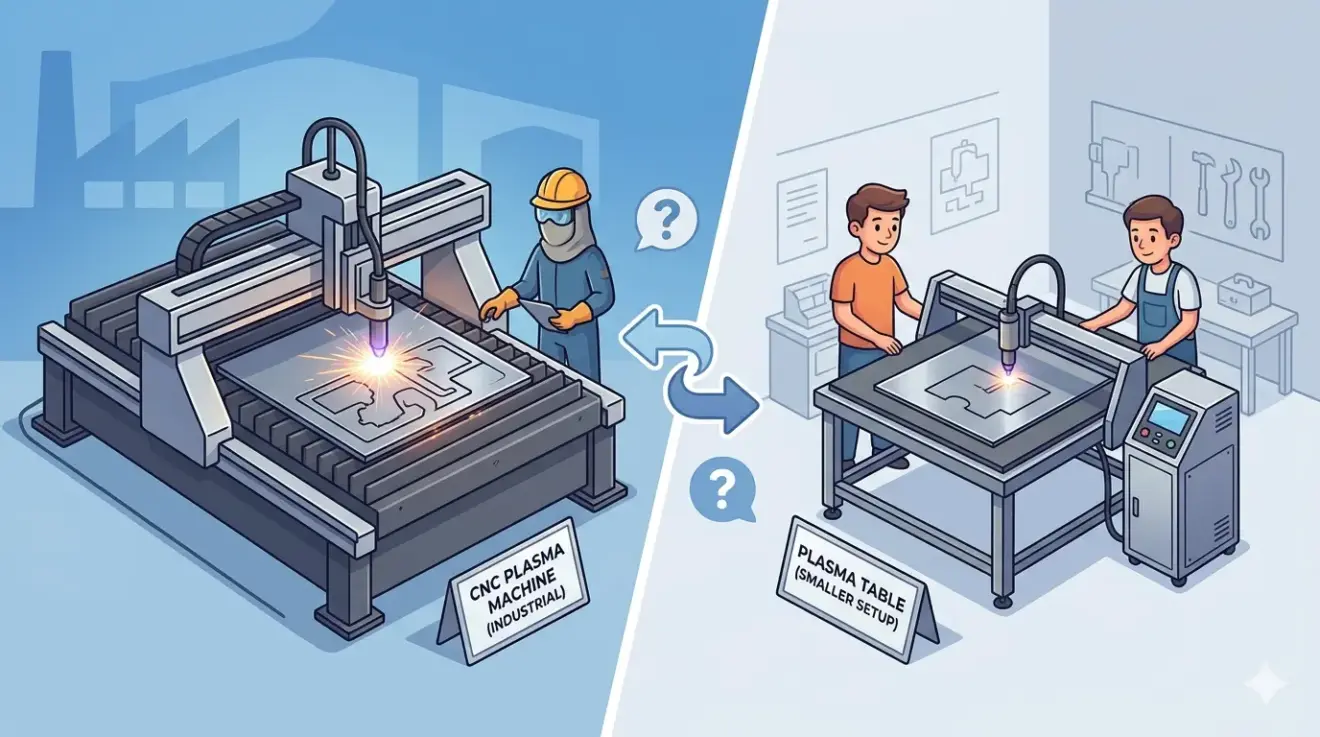
CNC Plasma Cutting Machine vs Plasma Table: Which Setup Should You Choose?
Tuesday, 21 April 2026
Fabrication buyers often stall at the quote stage because “plasma table” and “CNC plasma cutting machine” sound like different equipment classes when the torch physics are identical. The real distinction is scope: one label covers the flatbed platform, while the other implies the integrated production cell around it—motion, height control, software, extraction, and startup support.
- Published in Blog
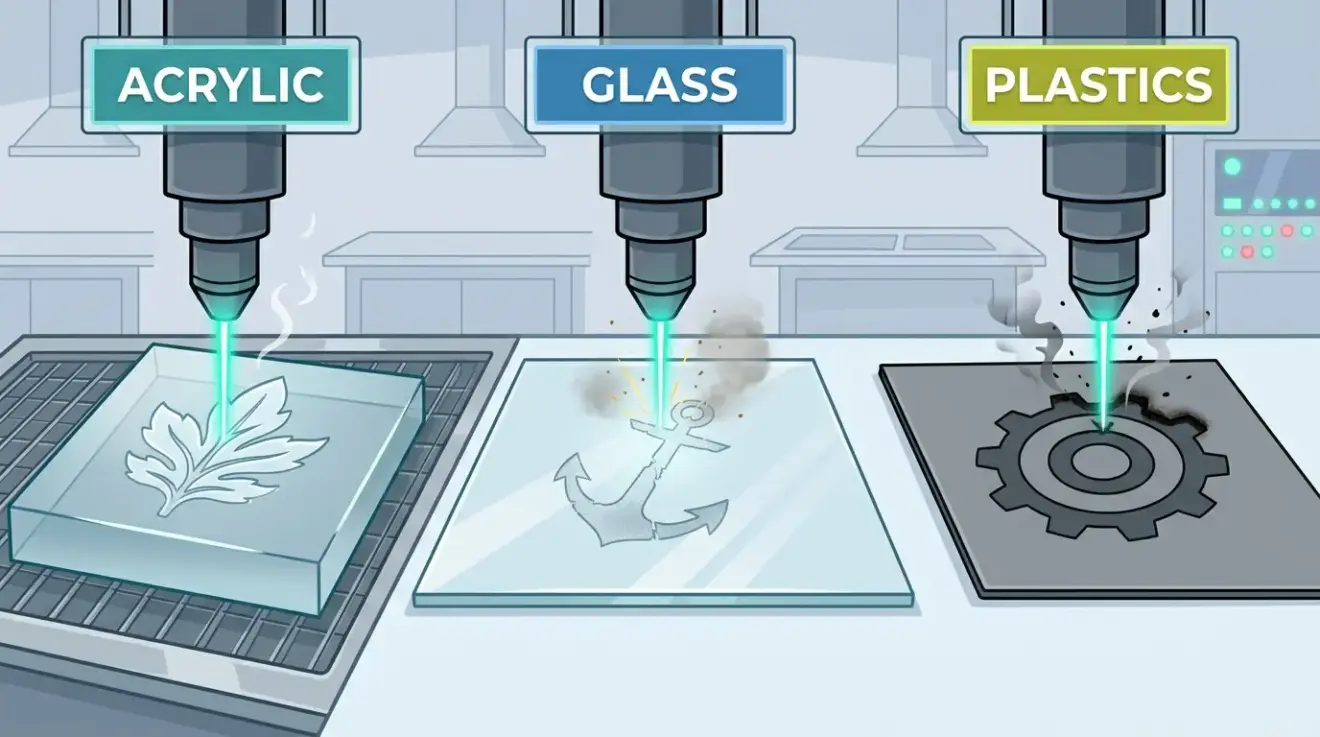
Laser Engraver for Acrylic, Glass, and Plastic: What Actually Changes by Material?
Tuesday, 21 April 2026
Most shops assume one laser engraver handles acrylic, glass, and plastic with minor parameter tweaks, yet that assumption usually fails within the first production batch. The beam comes from the same machine family, but material response, reject risk, cleanup burden, and recipe discipline shift substantially across substrates. Acrylic rewards visual consistency and cut-and-engrave flexibility, glass
- Published in Blog
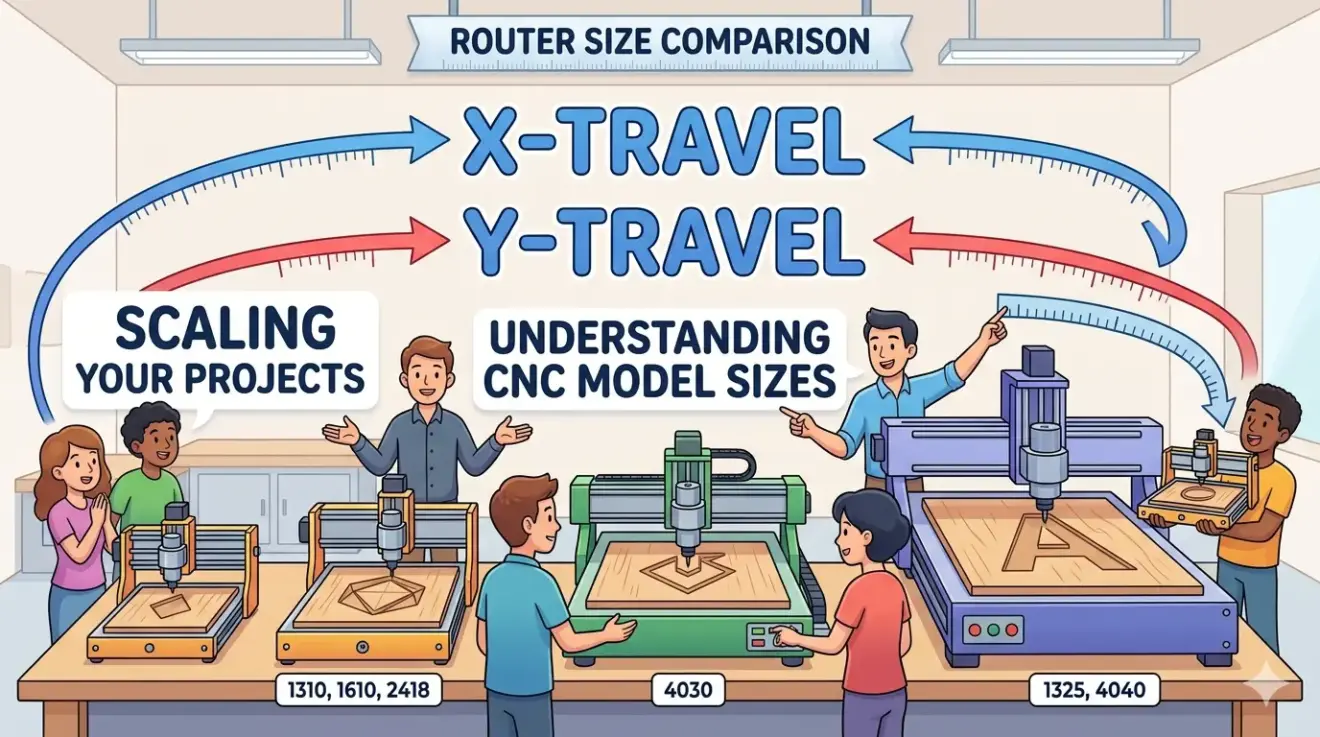
CNC 1310, 1325, 1610, 2418, 4030, and 4040 Machines: How These Router Model Numbers Compare
Tuesday, 21 April 2026
CNC router model numbers like 1310, 1325, and 4040 are routinely mistaken for performance ratings when they only hint at working envelope size. That misreading drives poor purchasing decisions: a compact machine gets assigned production work it cannot sustain, or a larger travel area creates false confidence in frame rigidity, spindle quality, and daily repeatability.
- Published in Blog
Small Laser Cutters for Light Commercial Work: Where They Fit and What to Evaluate
Tuesday, 21 April 2026
Compact laser systems fail in light commercial shops when buyers prioritize footprint or sticker price over the actual order pattern. This article addresses that mismatch directly, walking through where a small-format cutter earns its keep—short runs, frequent file changes, engraving-heavy work on wood and acrylic under roughly 600 x 400 mm—and where it becomes a
- Published in Blog
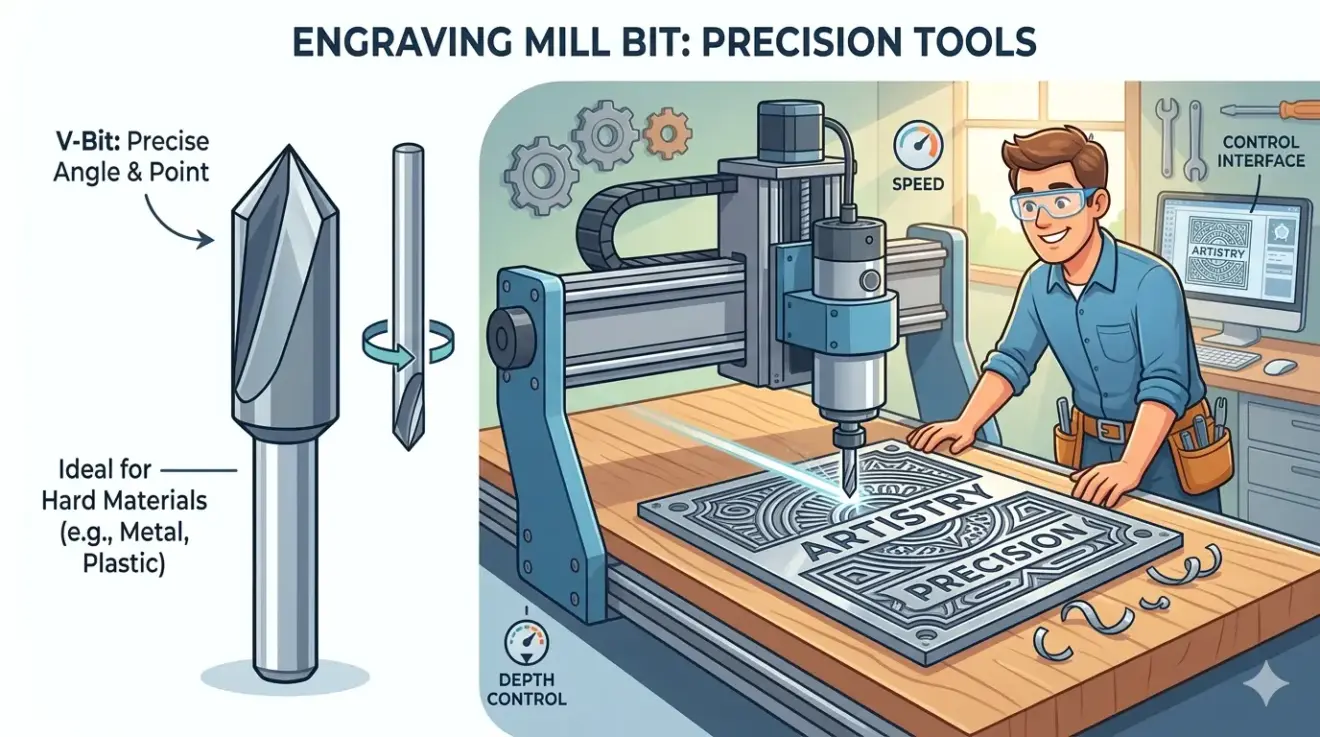
What Is an Engraving Mill Bit?
Tuesday, 21 April 2026
Selecting an engraving mill bit by cutter diameter alone is the fastest route to inconsistent marks, blurred line edges, and rejected panels. This article walks production teams through the real decision framework: defining the finished mark’s visual and functional requirements before opening the tooling catalog, then matching tip geometry, depth strategy, and workholding discipline to
- Published in Blog
Phantom CNC, Yeti CNC, and Other Niche Machines: How to Evaluate Unknown Brands
Tuesday, 21 April 2026
When a marketplace listing surfaces a CNC brand you have never heard of, the immediate temptation is to classify it as either a hidden gem or a trap—both judgments are premature and costly. This article addresses the real procurement dilemma: how to evaluate an unknown machine when brand recognition, installed base, and published service history
- Published in Blog
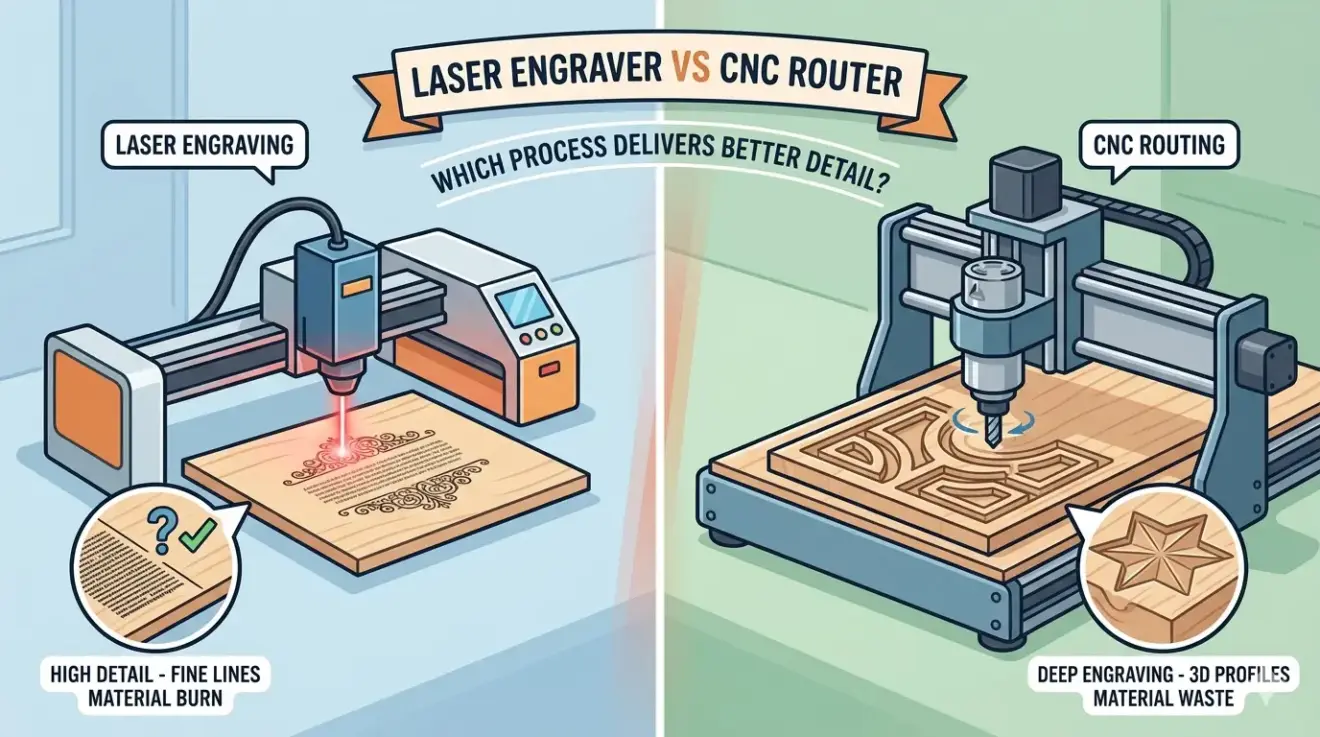
Laser Engraver vs CNC Router for Wood Products: Which Process Delivers Better Detail?
Tuesday, 21 April 2026
Wood product shops comparing laser engravers and CNC routers often frame the decision as a contest of raw precision, but the real question is which process matches the detail your parts actually sell. Surface graphics, geometric cuts, and machined depth features demand different capabilities: a laser handles fine text and sharp internal corners without cutter-radius
- Published in Blog
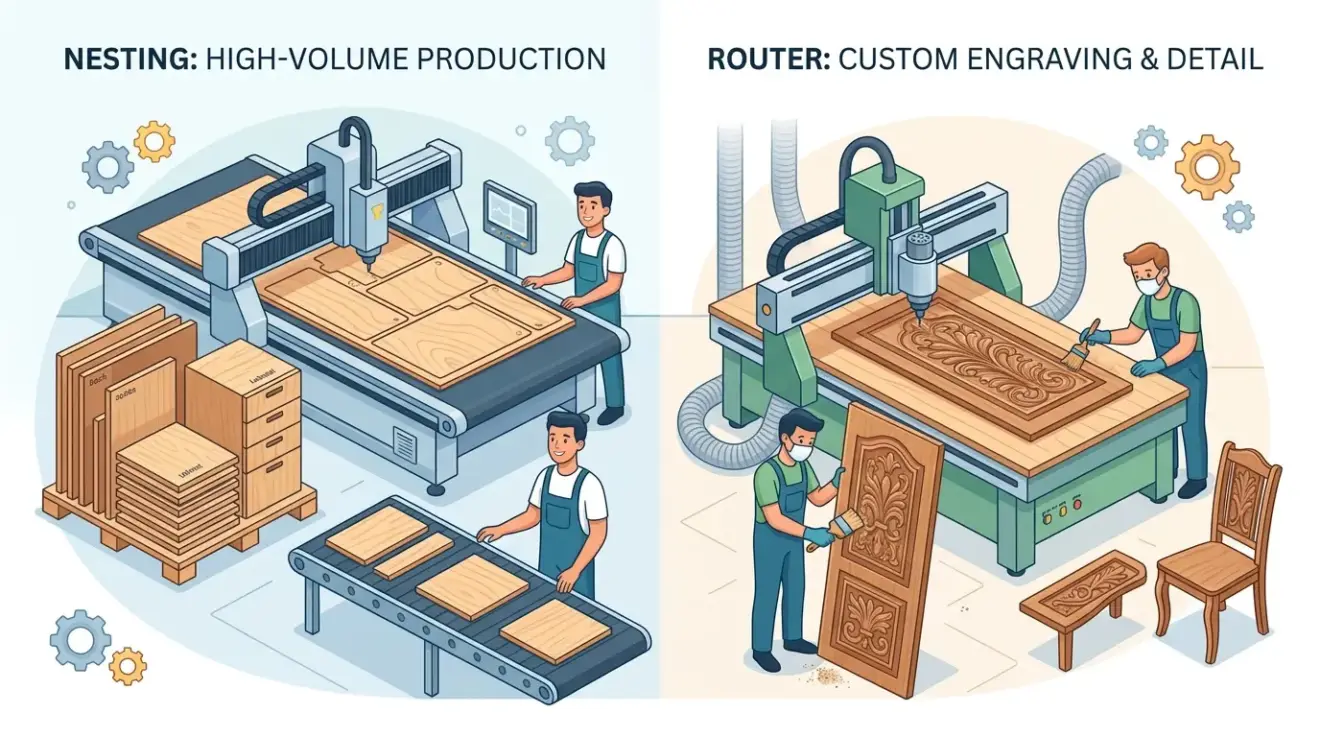
CNC Nesting Machine vs. CNC Router: What Actually Changes In Furniture Production?
Tuesday, 21 April 2026
When front-end pressure builds in a furniture plant, the symptoms are familiar: excessive manual sheet handling, unstable part flow into edge banding, and material yield that falls short of expectations. The decision between a CNC router and a nesting machine is not a hardware comparison, because both share gantry-style architecture and spindle-driven cutting. The real
- Published in Blog
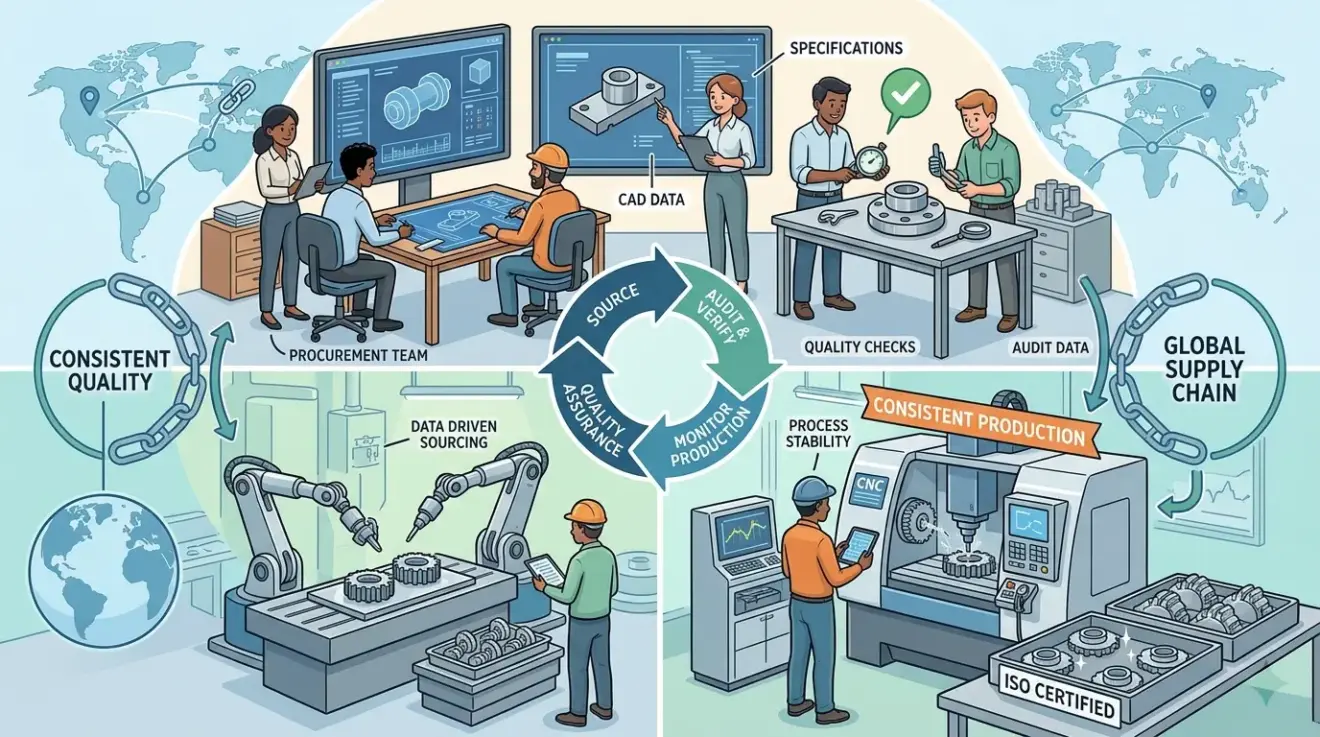
Machined Parts and CNC Components: How to Source Consistent Quality
Tuesday, 21 April 2026
Most quality problems in CNC-machined components surface long after incoming inspection, when assembly stops, warranty claims climb, or field failures trace back to hole-position drift that no routine check caught. The gap between what buyers assume and suppliers interpret creates variation before the first chip is cut. This article addresses that sourcing breakdown directly: how
- Published in Blog
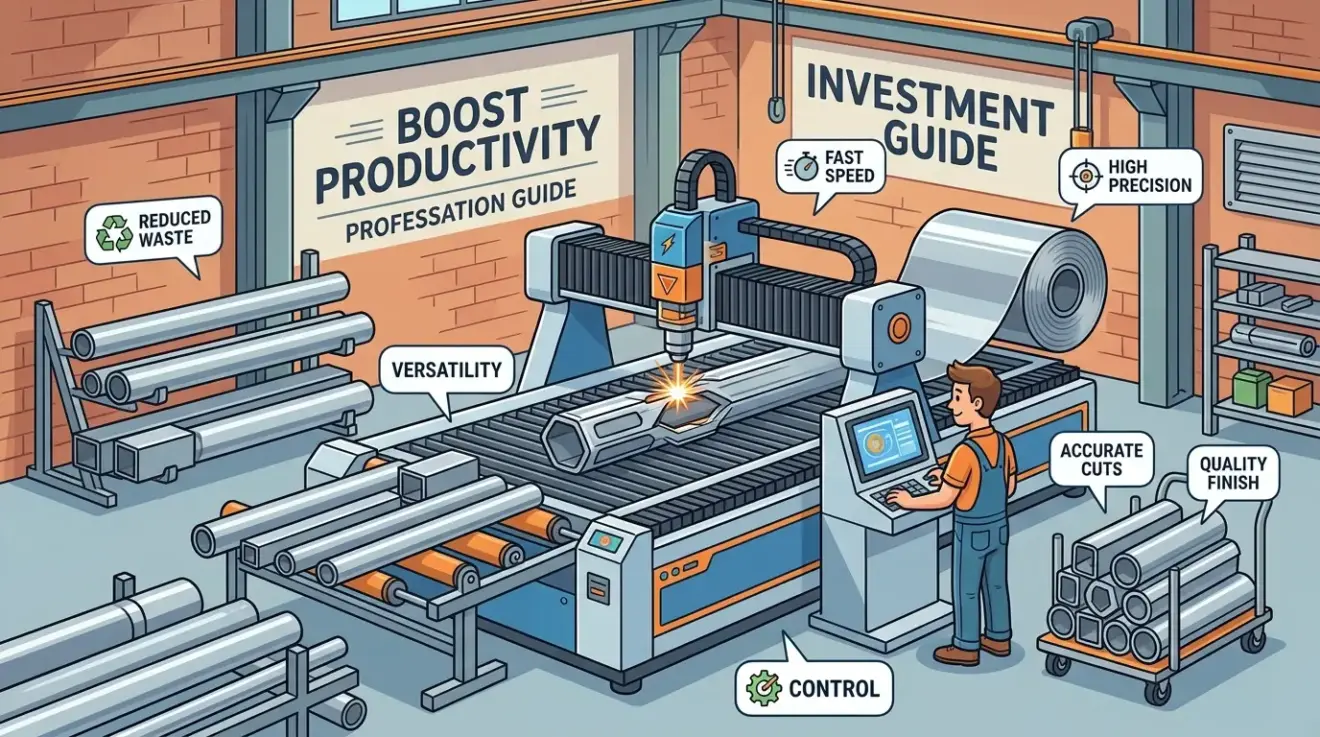
Laser Pipe Cutting Machine Buying Guide for Fabrication Shops
Monday, 20 April 2026
Tube and pipe preparation—sawing, drilling, marking, coping, and manual layout as separate steps—often becomes the true bottleneck in fabrication, long before welding or assembly. This guide addresses that workflow collapse, helping shops decide whether a laser pipe cutting machine genuinely fits their production reality. It forces evaluation of your actual part mix, profile variety, feature
- Published in Blog
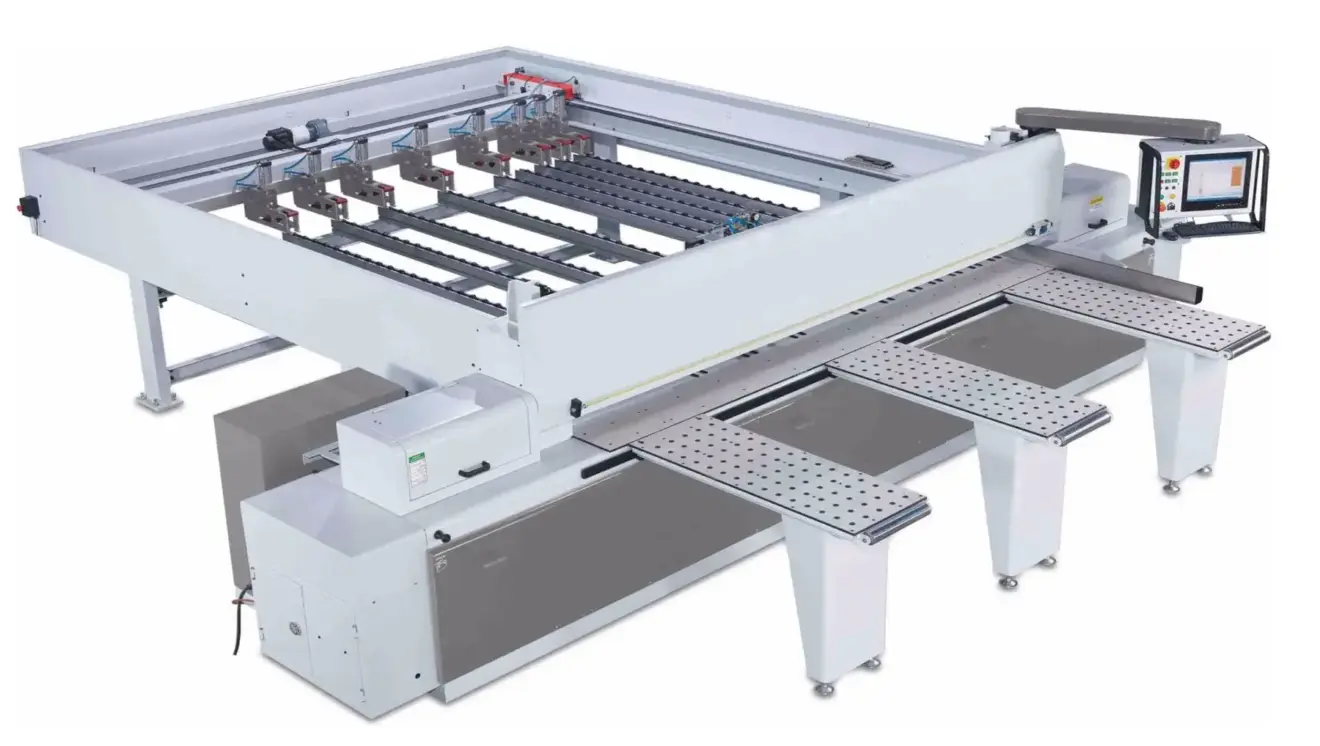
Panel Saws Explained: Types, Applications, and Buying Factors
Monday, 20 April 2026
Panel sizing errors rarely stop at the saw; they propagate into edgebanding misalignment, drilling drift, and assembly fit problems that force rework further down the line. That is why selecting a panel saw demands a workflow analysis rather than a feature comparison. This article walks through the main machine types—horizontal beam, vertical, operator-guided, and CNC-controlled—and
- Published in Blog
Edge Banding Equipment: What Matters Beyond Speed?
Monday, 20 April 2026
In panel furniture production, edge banding problems rarely show up as an argument about speed. They show up as visible glue lines, chipped corners, edge lifting after handling, mismatched panels at assembly, and operators stopping the line to correct work that should have moved forward cleanly the first time. That is why edge banding equipment
- Published in Blog
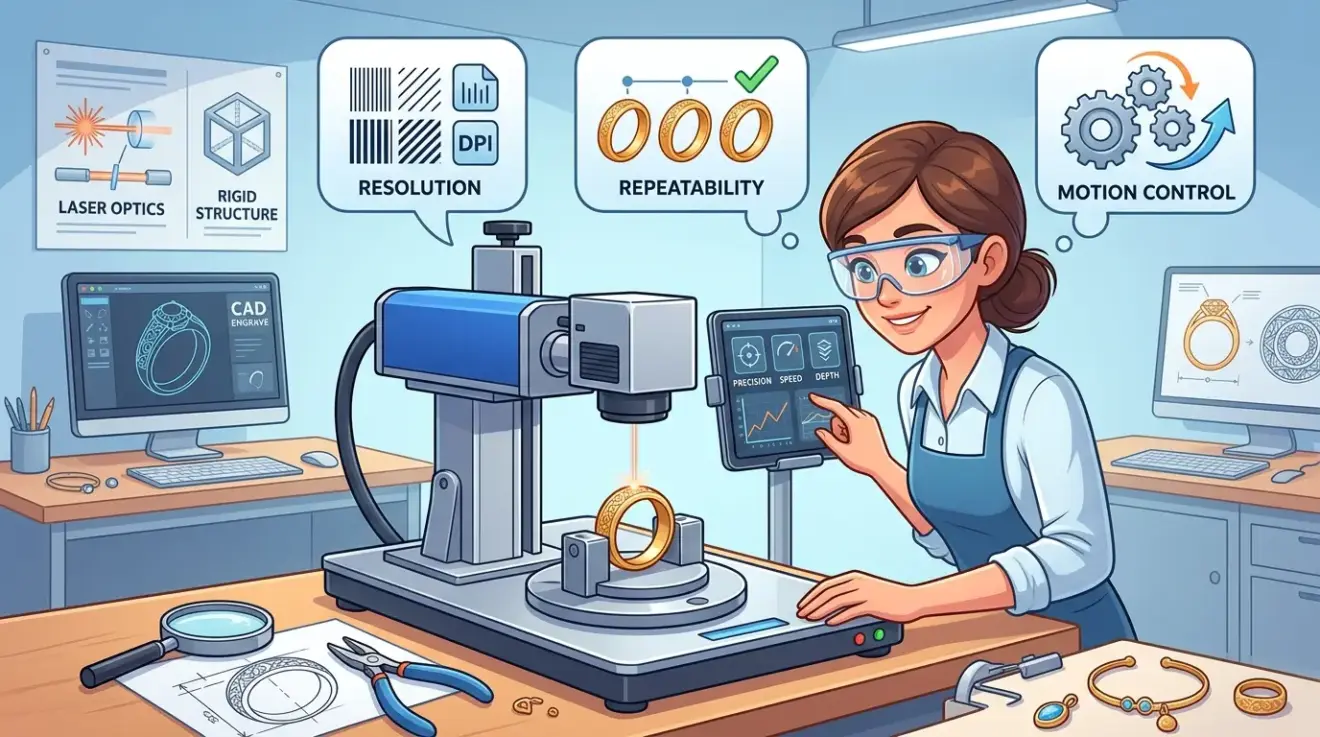
Jewelry Engraving Machine: What Precision Buyers Should Look For
Monday, 20 April 2026
Jewelry engraving precision fails most often not at the machine head but in the gap between a clean demo coupon and the realities of curved ring shanks, rhodium-plated surfaces, and batch repeatability. Shops that evaluate precision under sample conditions rather than production conditions end up comparing the wrong specifications, then discover blurred fine text, drifting
- Published in Blog
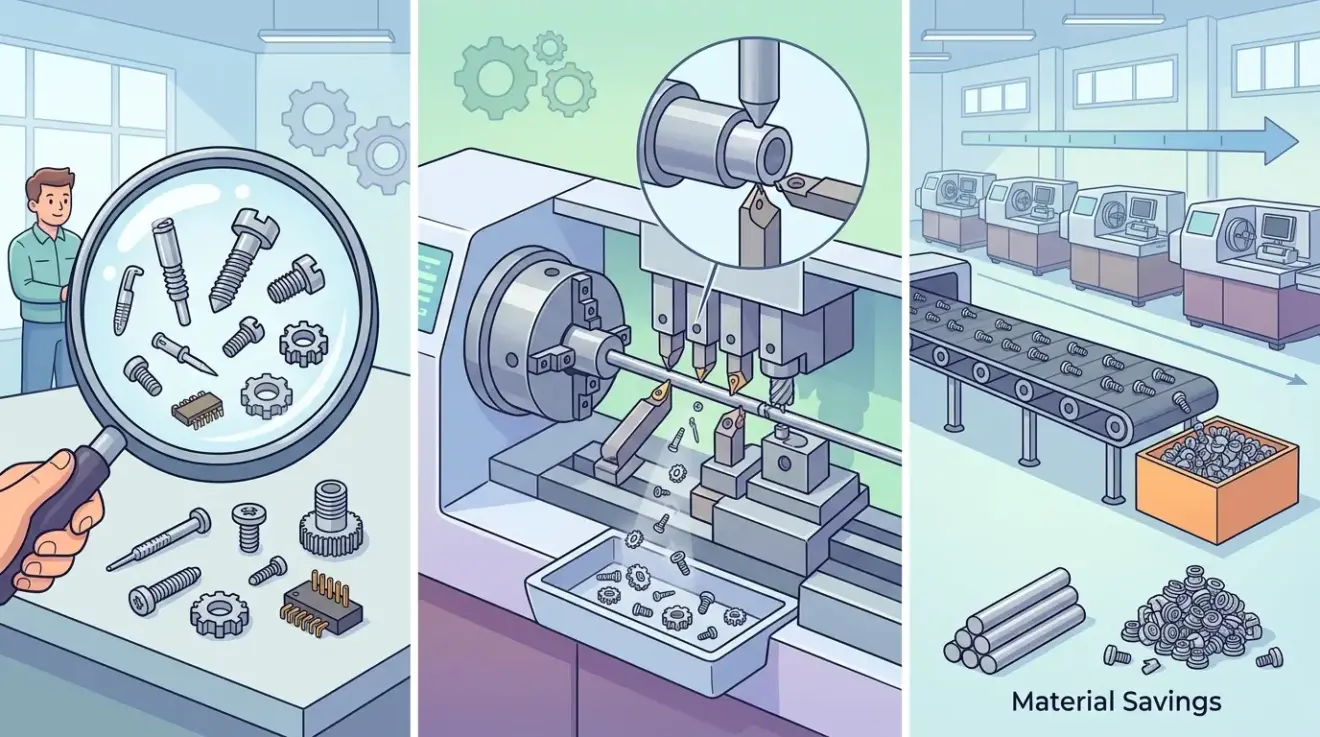
Swiss Turn Parts Explained: When Swiss-Type Machining Is the Better Option
Monday, 20 April 2026
Before any quote lands on your desk, the real question is whether the part’s geometry will hold still under the cut—not whether it simply looks small. Swiss-type machining earns its route only when near-cut support removes genuine instability, such as spring-like deflection on long, slender sections or fine features that drift under conventional holding. Buyers
- Published in Blog
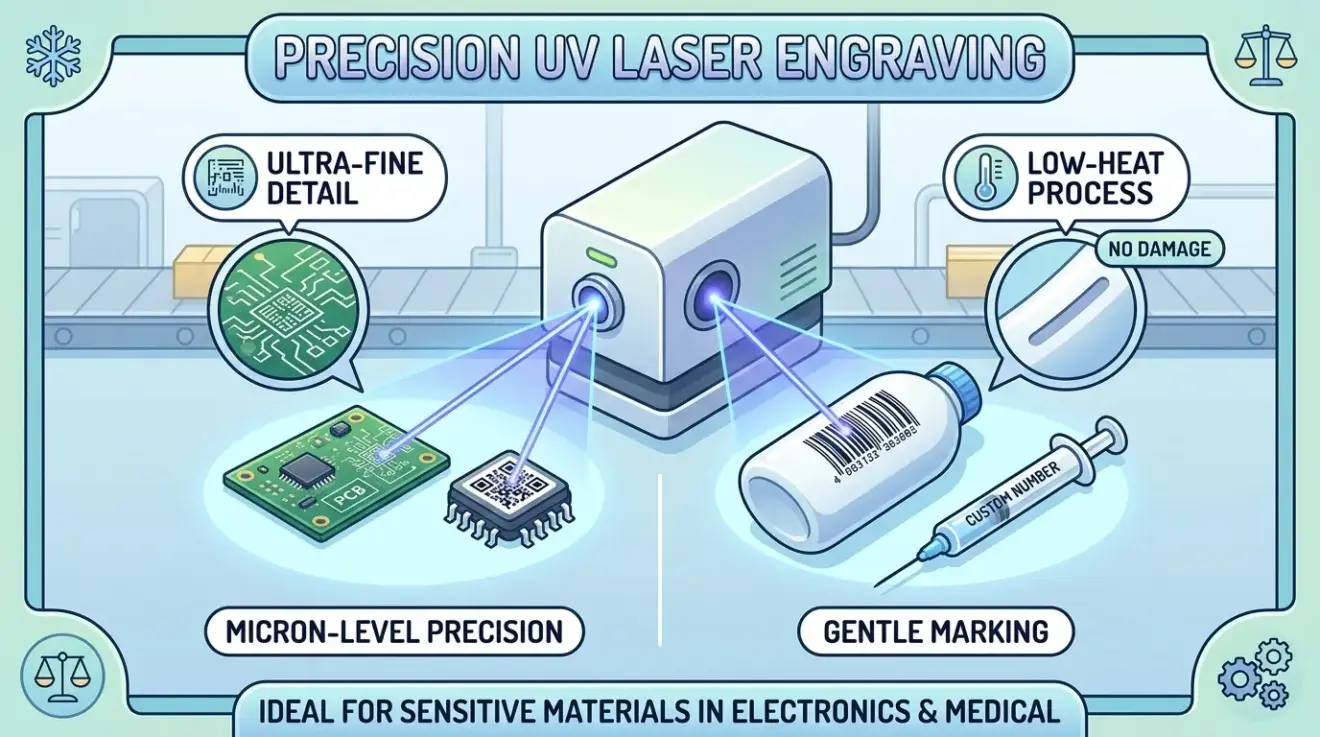
UV Laser Engraver for Fine, Low-Heat Marking: Where It Fits Best in Production
Monday, 20 April 2026
When a heat-sensitive part needs a fine, cosmetic-grade mark, the real production problem is reject risk, not raw laser capability. Standard thermal processes can whiten thin plastics, distort coated finishes, or haze brittle surfaces, turning traceability work into scrap. Before comparing UV laser spec sheets, buyers must decide whether the job is truly fine marking
- Published in Blog
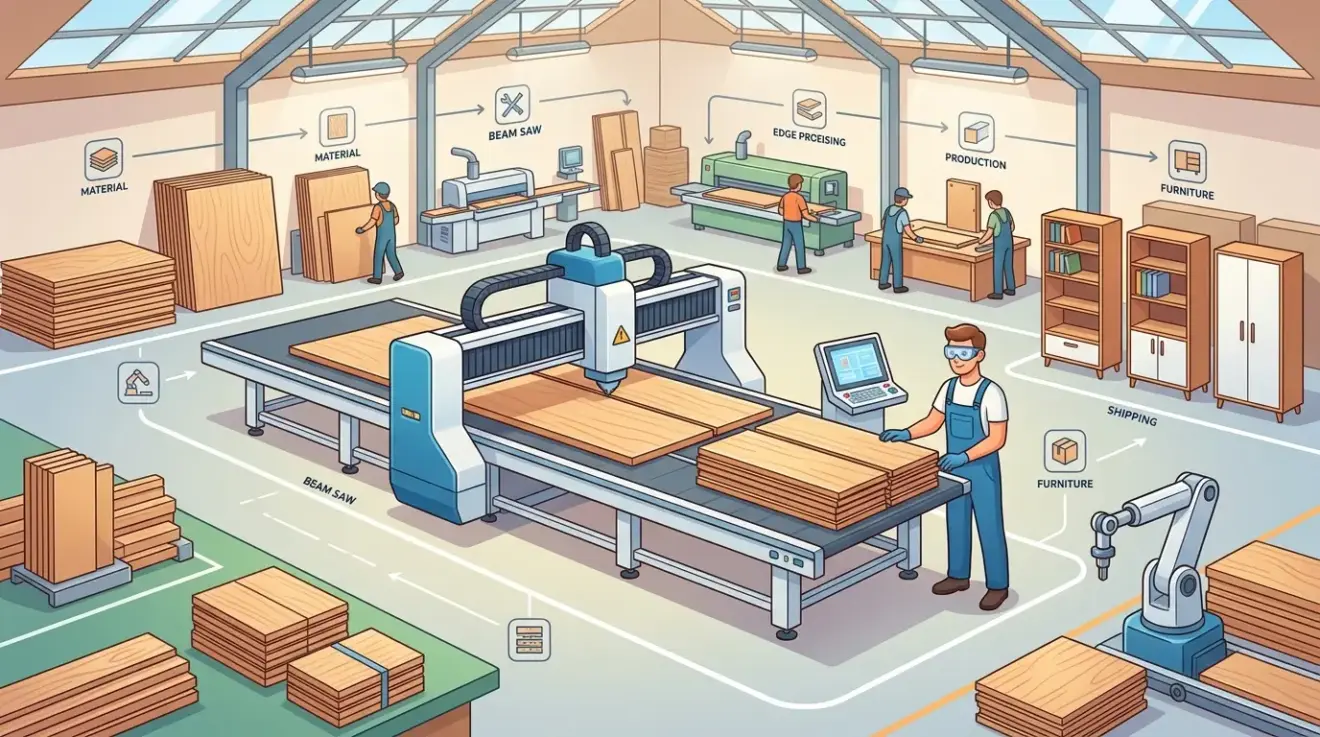
How To Choose a Beam Saw Machine for Furniture Factories
Monday, 20 April 2026
Panel cutting in a furniture factory rarely fails because the saw cannot make a cut; it fails when the cutting cell cannot feed edge banding, drilling, and assembly with stable, repeatable parts. Inconsistent dimensions force downstream operators to measure, re-cut, and adjust clamps, consuming labor and material without adding value. This guide helps production teams
- Published in Blog
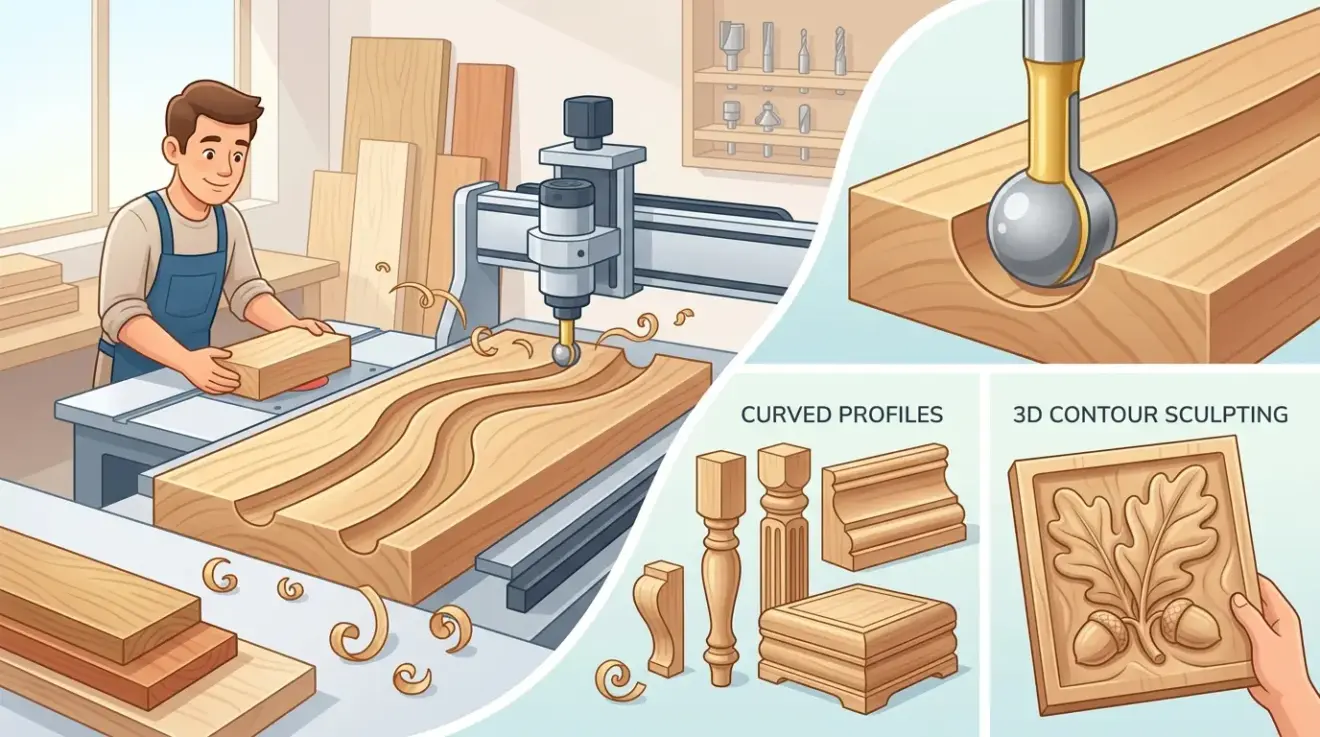
What Is a Ball Nose Router Bit?
Monday, 20 April 2026
When a production team weighs a ball nose router bit, the decision is rarely about the cutter itself—it is about how much sanding, scraping, and hand blending the shop is willing to absorb after the machine stops. Flat-ended tools leave visible stepping across curved geometry, and that finish defect becomes a labor cost that quietly
- Published in Blog